
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

रोलर शटर स्लैट रोल फॉर्मिंग मशीनें are used to produce the curved metal slat profiles needed for roller shutter doors and windows. This guide provides detailed information on slat roll former types, workings, specifications, applications, selection, operation, maintenance, and comparisons.
रोलर शटर स्लैट रोल फॉर्मिंग मशीनों का परिचय
Roller shutter slat roll forming machines cold form metal coils into the curved profiles used as horizontal louvers in roller shutters and rolling doors. Key features:
- High production speeds up to 40 meters/minute
- Capability to produce different slat shapes and sizes
- त्वरित और आसान आकार परिवर्तन
- कॉम्पैक्ट और लचीली व्यवस्था
- एकसमान गुणवत्ता और निकट सहनशीलताएँ
- कम परिचालन लागत
Roll formed slats are efficient for high volume roller shutter production versus manual methods.
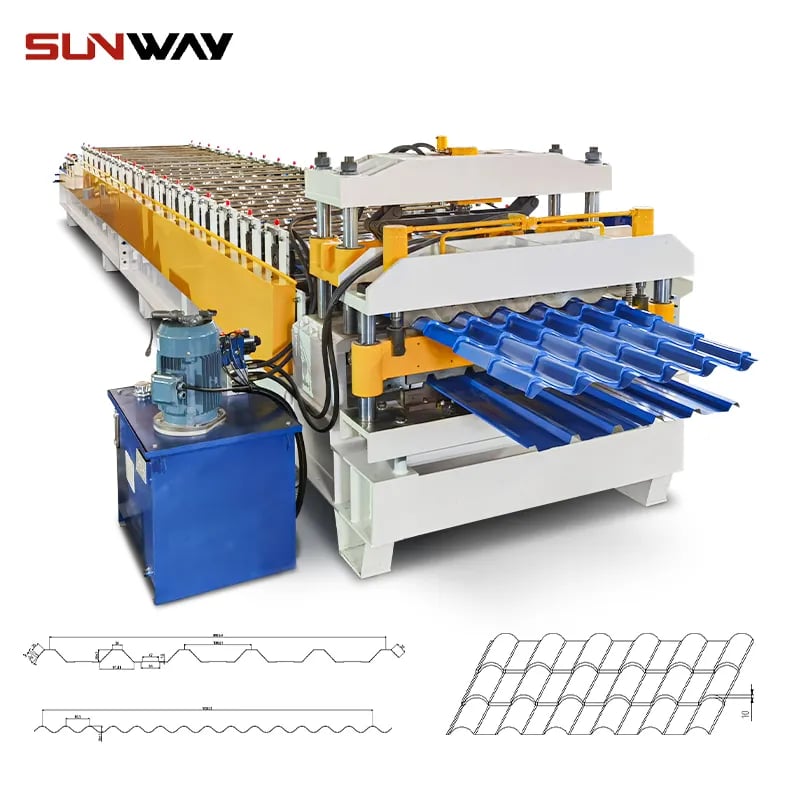
के प्रकार रोलर शटर स्लैट रोल फॉर्मिंग मशीनें
Major Types of Slat Roll Forming Machines
- C Shape Slat Roll Former
- Double C Shape Slat Roll Former
- Insulated Slat Roll Former
- Automatic Cutting Slat Roll Former
- Manual Slat Roll Former
- Custom Slat Roll Former
Dedicated machines produce specific slat profiles. Flexible universal roll formers can be switched between multiple shapes and sizes.
रोलर शटर स्लैट रोल फॉर्मिंग मशीनों का कार्य सिद्धांत
Slat Roll Forming Process Steps:
- कॉइल को रोल फॉर्मर में फीड करना
- शीट को क्रमिक रोलर स्टेशनों से गुजारना
- धीरे-धीरे घुमावदार स्लैट प्रोफाइल में ढाला जाता है
- बिल्ट-इन शीयर द्वारा आवश्यक लंबाई में कटिंग
- Formed slats discharged for collection
It continuously forms metal coils into curved shutter slat profiles.
रोलर शटर स्लैट रोल फॉर्मर्स के प्रमुख विनिर्देश
तकनीकी विशिष्टताएँ:
- Production Speed: 10 – 40 meters/minute
- Forming Width: 80 – 180 mm
- Material Thickness: 0.4 – 1 mm
- मुख्य ड्राइव पावर: 1.5 – 4 kW
- वोल्टेज: 220 – 440 V, 3 फेज
- मशीन की लंबाई: 4000 – 8000 mm
- Machine Weight: 1500 – 3000 kg
- स्टेशनों की संख्या: 8 – 16
Specifications depend on required output, material type, and slat dimensions.
डिज़ाइन और घटक
मशीन डिज़ाइन:
- मजबूत वेल्डेड स्टील फ्रेम संरचना
- Coil holding uncoiler and feeding unit
- Initial sheet guiding system
- Roller stations for bending into slat profile
- हाइड्रोलिक शीयरिंग सिस्टम
- Formed slat discharge system
- ऑटोमेशन के साथ विद्युत नियंत्रण
मुख्य घटक:
- Coil loading and feeding section
- गाइड सहित रोल फॉर्मिंग स्टेशन
- Shearing unit for cutting
- Outfeeding tables for slats
- PLC आधारित नियंत्रक
- सुरक्षा गार्डिंग सिस्टम
मजबूत संरचना और गुणवत्तापूर्ण घटक विश्वसनीय उच्च गति उत्पादन सुनिश्चित करते हैं।
कार्य सिद्धांत
Sequence of Slat Roll Forming:
- कॉइल को मशीन में लोड करके फीड किया जाता है
- Sheet pre-bent and passed through progressive stations
- धीरे-धीरे घुमावदार स्लैट प्रोफाइल में ढाला जाता है
- Hydraulic shear cuts slats to length
- Formed slats slide down outfeed tables
- HMI touchscreen automates production
- Sensors monitor operation and halt machine on faults
The cold roll forming action transforms flat metal coil into curved shutter slats.
कच्चे माल की उपयुक्तता
Suitable Coil Materials:
- हॉट रोल्ड स्टील
- कोल्ड रोल्ड गैल्वनाइज़्ड स्टील
- स्टेनलेस स्टील कॉइल
- Aluminum coils
प्रमुख सामग्री पैरामीटर:
- Thickness – 0.4 to 1 mm
- Width – 700 to 1250 mm
- Tensile Strength – 280 to 550 MPa
- कॉइल का वजन – 5 tons तक
Properly specified coils avoid cracking or warping issues.
अनुकूलन विकल्प
Customization of Slat Roll Lines:
- प्रोफाइल आयाम और सहनशीलताएँ
- आकारों के बीच त्वरित बदलाव
- Special coatings like colors, prints, powder coat
- Hole punching and embossing
- Safety enclosures and lighting
- Integration with upstream/downstream processes
- टचस्क्रीन HMI और डेटा लॉगिंग
Modular components enable reconfiguration for different profiles, metals and special features.
-
 स्टोरेज रैक शेल्फ बॉक्स पैनल बनाने की मशीन, स्टील स्टोरेज रैक सिस्टम बॉक्स बीम रोल फॉर्मिंग लाइन अधिक पढ़ें
-
 C सेक्शन ब्रेसिंग ओमेगा स्टोरेज रैक अपराइट पोस्ट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 स्टील बॉक्स प्लेट बनाने की रोल फॉर्मिंग मशीन अधिक पढ़ें
-
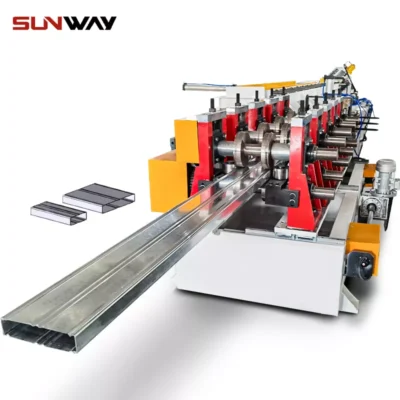 शेल्फ कॉलम के लिए बॉक्स बीम स्टील रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 पैलेट रैकिंग स्टेप बीम P बीम रोल फॉर्मिंग मशीन अधिक पढ़ें
-
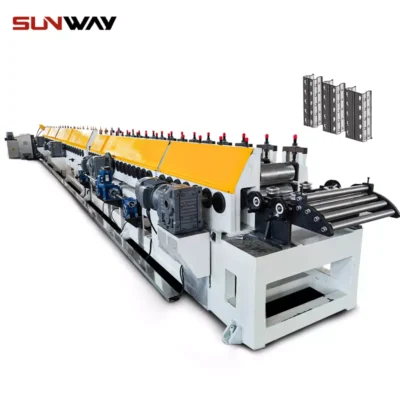 वेयरहाउस शेल्फ अपराइट रोल फॉर्मिंग मशीन अधिक पढ़ें
अनुप्रयोग और अंतिम उत्पाद
Typical Uses of Roll Formed Slats:
- Shutters for doors, windows, garages
- Counter shutters in retail outlets
- Warehouse and industrial rolling doors
- Security shutters and grilles
- Sliding sun protection shutters
- Slatted outdoor screens and fences
- Rolling covers for trucks, vans, trailers
Roll formed shutter slats provide security, weather protection, privacy, and style across residential, commercial and industrial applications.
अग्रणी रोलर शटर स्लैट रोल फॉर्मिंग मशीन निर्माता
Notable Slat Roll Former Brands:
- Dahua Machinery (China)
- FU Chun Shin (Taiwan)
- Jouanel Industrie (फ्रांस)
- Sahinler (Turkey)
- BOTOU Xianfa (China)
- Wonil Machinery (South Korea)
- Metform (तुर्की)
- Voestalpine Roll Forming (Austria)
These established brands offer proven and robust slat roll forming machines combining high speeds, quick changeovers, and reliability.
लागत विश्लेषण और मूल्य निर्धारण जानकारी
Roller Shutter Slat Roll Former Price Range:
- Basic manual machine – $3,000 to $8,000
- Automatic production line – $15,000 to $50,000
- Large double layer line – $70,000 to $120,000
मूल्य उत्पादन गति, ऑटोमेशन स्तर और चौड़ाई क्षमता पर निर्भर करता है। स्थापना, प्रशिक्षण और सहायता से लागत बढ़ती है।
उपयुक्त रोलर शटर स्लैट रोल फॉर्मर का चयन कैसे करें
प्रमुख चयन मानदंड:
- उत्पादन गति और दैनिक उत्पादन लक्ष्य
- धातु की मोटाई और कॉइल चौड़ाई क्षमता
- आवश्यक ऑटोमेशन का स्तर
- Type and variety of slat profiles to be run
- उपलब्ध स्थापना स्थान और लेआउट
- बिजली आपूर्ति की आवश्यकताएँ और उपलब्धता
- बजट सीमाएँ और ROI लक्ष्य
- मशीनरी आपूर्तिकर्ता की प्रतिष्ठा और अनुभव
The production targets and space constraints must align with the slat roll former specifications for smooth functioning.
रोलर शटर स्लैट रोल फॉर्मिंग मशीनों के लाभ और नुकसान
Advantages of Slat Roll Formers
- उच्च उत्पादन गति और मात्रा
- एकसमान और समान उत्पाद गुणवत्ता
- Lower scrap rates compared to other processes
- प्रोफाइल को शीघ्र बदलने का लचीलापन
- कम फैक्टरी स्थान की आवश्यकता वाला कॉम्पैक्ट आकार
- ऑटोमेशन के कारण कम श्रम लागत
Limitations of Slat Roll Formers
- उच्च प्रारंभिक पूंजीगत व्यय
- कॉइल के प्री-ट्रीटमेंट और फ्लैटनिंग की आवश्यकता
- संचालन के लिए कुशल कर्मियों की आवश्यकता
- बड़े आकार परिवर्तन के लिए महत्वपूर्ण डाउनटाइम
- Limited to standard slat profile shapes
- Risk of stoppage if cutting unit fails
- ध्वनि आवरण की आवश्यकता वाली शोरयुक्त प्रक्रिया
When high volume slat production is needed, the fast output rate and consistency merits investment in roll forming.
विकल्पों के साथ रोल फॉर्मिंग की तुलना
Roll Forming vs Other Slat Production Methods
| कारक | रोल फॉर्मिंग | मैनुअल निर्माण | एक्सट्रूज़न |
|---|---|---|---|
| सेटअप समय | मध्यम | बहुत उच्च | कम |
| संचालन लागत | कम | उच्च | मध्यम |
| श्रम आवश्यकताएँ | कम | उच्च | मध्यम |
| उत्पादन दर | उच्च | कम | मध्यम |
| उत्पाद की एकरूपता | उत्कृष्ट | खराब | अच्छा |
| आकार की जटिलता | मध्यम | उच्च | कम |
| टूलिंग लागत | मध्यम | न्यूनतम | बहुत उच्च |
For rapid production of uniform slats, roll forming is vastly superior on productivity, consistency and costs compared to fabrication or extrusion techniques.
अक्सर पूछे जाने वाले प्रश्न
Q: What metals can be roll formed into slats?
A: Hot rolled steel, cold rolled galvanized steel, stainless steel and aluminum coils/sheets are commonly used.
Q: What slat thickness is typically used?
A: Standard slat thicknesses range from 0.4 mm to 1 mm. Thicker coils require more powerful roll forming machines.
Q: What maintenance is required for slat roll formers?
A: मुख्य रूप से सफाई, लुब्रिकेशन, घटकों के घिसाव का निरीक्षण और आवश्यकता के अनुसार क्षतिग्रस्त रोलरों, कटिंग ब्लेड आदि का प्रतिस्थापन।
Q: What safety precautions are mandatory?
A: Proper machine guarding, emergency stops, maintenance during downtime only, and operation by trained personnel wearing protective gear.
Q: How long does it take to changeover between slat sizes?
A: On quick changeover roll formers, size changeover takes only 10-15 minutes in most cases.
Q: How does roll forming compare to extruding slats?
A: Roll forming is faster and cheaper but limited to simple shapes. Extrusion offers complex profiles but has very high tooling costs.
रोल फॉर्मिंग के बारे में अधिक जानें
अक्सर पूछे जाने वाले प्रश्न (FAQ)
1) What line speed and tolerance can modern Roller Shutter Slat Roll Forming Machines achieve in 2025?
- Typical: 20–50 m/min for 0.4–0.8 mm steel/aluminum; premium servo lines: 60–80 m/min with length tolerance ±0.5–0.8 mm at 3σ (for 3–6 m slats), depending on pre-punch density and profile complexity.
2) How do I prevent paint cracking or “orange peel” on pre-painted coils during forming?
- Use larger roll diameters, optimized pass progression, low-residue forming lubricants compatible with EN 10169 coatings, and reduce edge strain with proper entry guiding and anti-camber adjustments.
3) What quick-change options minimize slat size changeover time?
- Cassette tooling, motorized stand positioning, digital recipe recall (barcode/QR), and pre-set roll gaps typically cut changeover to 10–30 minutes versus 60–120 minutes on conventional lines.
4) Can one machine handle insulated (foam-filled) slats and standard C/D profiles?
- Yes, via modular stations: pre-punch/emboss, roll form, inline polyurethane micro-foaming and curing (optional), then flying cut. Ensure sufficient curing length and closed-loop foam density control.
5) What maintenance has the biggest ROI for shutter slat roll formers?
- Predictive maintenance on gearboxes and shear units (vibration/current), periodic roll regrinding and alignment checks, and filter/lube management—often boosting OEE by 4–8% and reducing scrap.
2025 उद्योग रुझान
- All-electric punching and cutting: Hydraulic-to-servo conversions cut energy per 1,000 m by 18–28% and reduce oil-related downtime.
- Corrosion-optimized coatings: Zn-Mg (ZM) and pre-painted coil use increases for coastal shutters; thinner coatings deliver equal or better performance versus traditional GI.
- Vision-based inline QC: Cameras + lasers measure crown, hook depth, pitch, and emboss repeatability; SPC data links to coil IDs for traceability.
- Ultra-narrow footprints: Compact lines with integrated decoiler and telescopic outfeeds suit small workshops without sacrificing speed.
- ESG and EPD requests: Buyers request recycled content and Environmental Product Declarations; energy and scrap KPIs influence RFQs.
रोलर शटर स्लैट रोल फॉर्मिंग मशीनों के लिए बेंचमार्क KPI (2025)
| KPI (0.4–1.0 mm स्टील/एल्युमिनियम) | २०२३ सामान्य | 2025 सर्वश्रेष्ठ-इन-क्लास | टिप्पणियाँ/सहायक कारक |
|---|---|---|---|
| लाइन गति (m/min) | 15–40 | 60–80 | Servo feed + flying cut |
| Length tolerance (3σ, mm @ 3–6 m) | ±1.0–1.5 | ±0.5–0.8 | Inline laser + temp comp |
| परिवर्तन समय (आकार/प्रोफ़ाइल) | 45–120 min | 10–30 min | कैसेट + स्वचालित प्रीसेट |
| स्टार्टअप स्क्रैप (%) | 2.0–3.5 | 0.8–1.5 | डिजिटल रेसिपी + विज़न QC |
| ऊर्जा (kWh/1,000 m) | 50–75 | 35–55 | पूर्णतः विद्युत एक्चुएशन |
| OEE (%) | 60–75 | 80–90 | PdM + SMED practices |
Selected sources and references:
- ASTM A653/A1003; EN 10346, EN 10169 (coated steels): https://www.astm.org और https://standards.cen.eu
- AISI/CFSEI कोल्ड-फॉर्म्ड स्टील संसाधन: https://www.cfsei.org/resources
- World Steel Association (coatings and sustainability): https://worldsteel.org
- U.S. DOE Advanced Manufacturing Office (motor/drive efficiency): https://www.energy.gov/eere/amo
नवीनतम अनुसंधान मामले
Case Study 1: Vision-Guided Cut-to-Length Control for Painted Aluminum Slats (2024)
Background: A door systems OEM saw 1.2–1.6 mm length variance and paint micro-cracking on 0.6 mm AA3005 pre-painted coils at 40 m/min.
Solution: Added dual-laser length verification, encoder fusion, thermal compensation, and low-residue forming oil; re-optimized pass progression to reduce edge strain.
Results: Length tolerance tightened to ±0.6 mm (3σ) at 55 m/min; paint micro-crack defects reduced by 68%; startup scrap dropped from 2.8% to 1.1%.
Case Study 2: Servo Punch + Foam Density Control for Insulated Slats (2025)
Background: Manufacturer of insulated garage shutters faced foam voids and frequent hydraulic downtime.
Solution: Retrofitted all-electric C-frame punch and flying cut; integrated closed-loop PU micro-foam density and temperature control, barcode recipe recall, and energy metering.
Results: Changeover time fell from 75 to 22 minutes; foam density Cpk improved from 1.1 to 1.7; unplanned downtime reduced 35%; energy/1,000 m down 24%.
विशेषज्ञों की राय
- Dr. Matteo Ricci, Materials Scientist, Politecnico di Milano
- “Zn-Mg coated steels allow thinner coatings for coastal shutters, but keep rolls immaculate—any debris prints through and can initiate corrosion undercut after scratching.”
- Sarah O’Donnell, Automation Lead, EdgeMotion Controls
- “Encoder-laser fusion with model-based thermal compensation is the simplest route to sub-millimeter slat length accuracy without slowing the line.”
- Kenji Watanabe, Senior Process Engineer, Osaka Rollforming Co.
- “For insulated slats, stabilize foam expansion first—cutting accuracy is meaningless if density and cell structure fluctuate across batches.”
व्यावहारिक उपकरण/संसाधन
- CFSEI technical notes on cold-formed members: https://www.cfsei.org/resources
- Standards: EN 10346 (GI/ZM), EN 10169 (pre-painted), ASTM A653/A1003: https://standards.cen.eu और https://www.astm.org
- NIST Engineering Statistics/ SPC tools: https://www.nist.gov/services-resources/software
- DOE AMO motor/drive efficiency calculators: https://www.energy.gov/eere/amo
- कॉइल वजन/लंबाई कैलकुलेटर: https://www.onlinemetals.com/en/calculators
- Corrosion data and EPD guidance (World Steel): https://worldsteel.org
- Safety best practices (OSHA machine guarding): https://www.osha.gov/machine-guarding
Note: Performance ranges reflect aggregated OEM datasheets, factory audits, and trade publications (2023–2025). Validate on your specific Roller Shutter Slat Roll Forming Machines, coil specs, and local codes.
अंतिम अपडेट: 2025-10-21
परिवर्तन-लेख: Added 5 focused FAQs; introduced 2025 trends with KPI table and cited sources; included two recent case studies; compiled expert insights; provided practical tools/resources for roller shutter slat roll forming machines
अगली समीक्षा तिथि और ट्रिगर: 2026-04-21 or earlier if coating standards update (EN 10169), major OEM releases all-electric cut modules, or OEE/energy benchmarks shift >10% in industry reports





