
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

Self lock roofing sheet roll forming machines produce interlocking roof panels with integrated connectors from coil feedstock. This guide reviews self lock roll former configurations, components, customization options, operation guidance and maintenance considerations to inform manufacturers.
सेल्फ लॉक रूफिंग शीट रोल फॉर्मिंग मशीन अवलोकन
Self lock roof sheet roll formers transform flat coil stock into roofing panels with integrated mechanical seams for simplified installation. Key features:
- High hourly production volumes lower cost per panel
- Flexibility producing varied interlock profile types
- स्टैम्पिंग प्रक्रियाओं की तुलना में कम सामग्री अपशिष्ट
- Continuous automated production 24×7 after coil loading
Reviewing configurations, customization possibilities and maintenance procedures assists manufacturers employing self lock roll formers optimally.
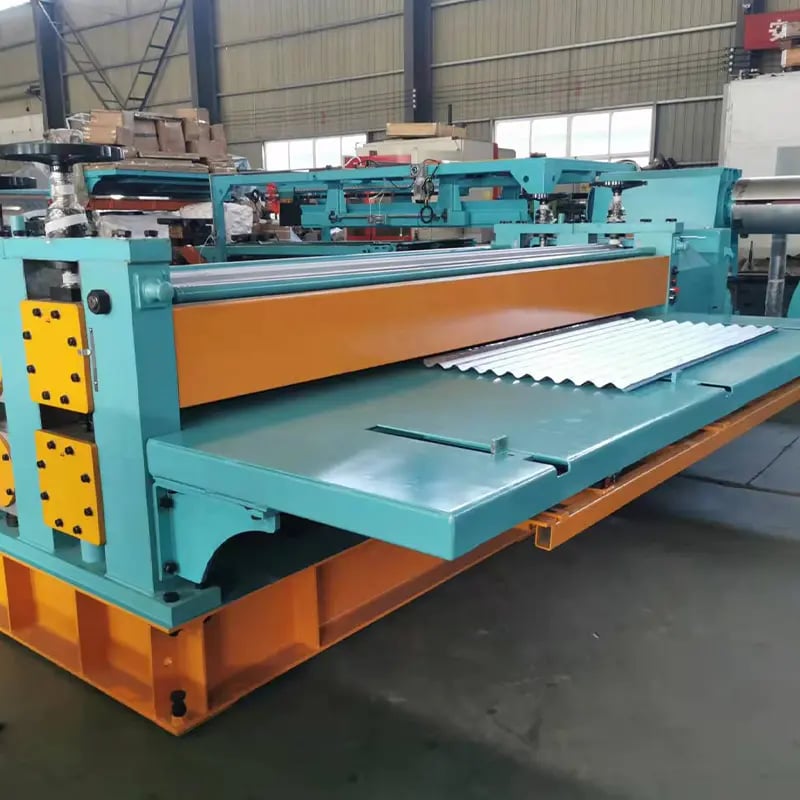
सेल्फ लॉक रूफिंग शीट रोल फॉर्मर्स के प्रकार
Common variants include:
| प्रकार | विवरण |
|---|---|
| यांत्रिक ड्राइव | यांत्रिक गियरबॉक्स के माध्यम से हाइड्रोलिक-संचालित स्टेशन |
| Servo Electric Drive | AC precision servo motors independently control stations |
| Single Layer | For standard smaller interlock profiles |
| डबल लेयर | Complex larger interlocks simultaneous top and bottom forming |
तालिका 1: Self lock roofing sheet roll former types covering power, configuration and forming considerations
Electric servo controls enable fast set changeovers while mechanical gears provide heavy duty economical forming reliability. Double layer machines boost output for standard self lock commodities.
सेल्फ लॉकिंग रूफ शीट के लिए रोल फॉर्मिंग प्रक्रिया
A multi-stage roll forming process for interlocking roof panels involves:
डीकॉइलिंग – कॉइल स्टॉक तनाव बनाए रखने वाले संचालित डिकोइलर में प्रवेश करता है
फीडिंग – फीड रोल स्टील को अगले स्टेशनों से खींचते हैं
पूर्व-फॉर्मिंग – Sheet lightly forms into early panel wave shape
प्रोफ़ाइल निर्माण – Sequential stands cut then form connector hooks
Lock Forming – Final stands close locks into other side
कटिंग – Hydraulic shear slices panels to length
गिनती – स्वचालित काउंटर शीटों की गिनती करते हैं
स्टैकिंग – Formed panels placed onto exit tables
Synchronizing these steps enables efficient high volume production of self locking roofing.
सेल्फ लॉक रूफिंग शीट रोल फॉर्मर्स के प्रमुख घटक
Typical engineered sub systems include:
- डिकॉयलर – कॉइल स्ट्रिप को फीडिंग लाइन के इनपुट में रखता है
- फीड सिस्टम – Pulls stock into first forming station
- Progressive Forming Dies – Gradually cut then shape interlocks
- हाइड्रॉलिक्स सिस्टम – यांत्रिक गियरबॉक्स ड्राइव को शक्ति प्रदान करता है
- नियंत्रण प्रणाली – Automates line speed and counting
- कटर – Shears panels to length after profile complete
- निकास कन्वेयर – Stacks finished panels
Interlinking these modules maximizes automated forming of self locking roof sheeting.
-
 इलेक्ट्रिकल कैबिनेट फ्रेम रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 Din रेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 केबल लैडर रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 PV माउंटिंग ब्रैकेट C आकार प्रोफाइल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 केबल ट्रे रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 PV माउंटिंग ब्रैकेट रोल फॉर्मिंग मशीन (HAT / Omega प्रोफ़ाइल) अधिक पढ़ें
-
 PV माउंटिंग ब्रैकेट Z आकार प्रोफाइल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 सोलर माउंटिंग स्ट्रट चैनल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 स्ट्रट चैनल रोल फॉर्मिंग मशीन अधिक पढ़ें
सेल्फ लॉक रूफ शीट रोल फॉर्मर लाइनों का अनुकूलन
While standardized, customization possibilities include:
- Profile Tooling – Special roll sets match customer interlock geometries
- गति – Servo electric drives for faster cycle times
- स्वचालन – Monitoring, stacking and packaging allows lights out operations
- Decoiler Size – Large coils mean fewer loading interruptions
- द्वितीयक संचालन – Custom post-forming fabrication steps like punching
Articulating special engineering goals in procurement requests allows pricing appropriate customization delivering lines matching security interlock roofing business requirements.
सेल्फ लॉक रूफ शीट रोल फॉर्मर निर्माताओं का चयन
When evaluating suppliers, key selection criteria encompasses:
- विशेषज्ञता – समर्पित रोल फॉर्मर मशीन विक्रेताओं की तलाश करें
- अनुभव – Review company lineage and client installation portfolio
- डिजाइन सेवाएँ – Necessitate engineering support for custom needs
- गुणवत्ता – Require all steel fabricated construction
- सत्यापन – Look for quality/safety control certifications
- सेवाएँ – Installation, training and maintenance support options
- मूल्य निर्धारण – Compare proposals ensuring adequate feature parity
Thoroughly vetting numerous manufacturers on engineering strengths, safety-focused production and ongoing services availability builds confidence when investing in major factory enhancing automation.
सेल्फ लॉक रूफ शीट रोल फॉर्मर की कीमत
Budget estimates for complete roll forming line costs span:
- बेस मशीन – Around $125,000 for basics
- आकार अनुकूलन – For bigger decoilers add $5,000-$15,000
- सर्वो अपग्रेड – Adds $25,000-$60,000 versus base mechanical drives
- कन्वेयर/ट्रांसफर – स्वचालन के आधार पर $5,000-$15,000
- स्थापना/परिवहन – Typically runs $15,000-$30,000 using professional technicians
Factor $175,000 to $275,000+ for turnkey lines matching standard versus fully customized order specifications ultimately aligning fabricated productivity to target business volume, flexibility and quality prerequisites demanded daily.
सेल्फ लॉक रूफ शीट रोल फॉर्मर संचालन का रखरखाव
To sustain consistent production, recommended routines include:
दैनिक सफाई – ट्रांसफर में बाधा डालने वाले लाइन मलबे को साफ करें
निर्धारित निरीक्षण – Monthly inspect hydraulics, electricals and alignments
रोल रखरखाव – Lubricate/resurface roll dies minimizing scratches
पुनः अंशांकन – Annual servicing checking sensors, actuators and press alignments
Catching component wear early via prescribed maintenance prevents unplanned downtime through replacing parts proactively – a reliability-focused mindset applied sustaining high percent operating availability enabling consistent interlock roof sheeting production 24×7 over decades seamlessly matching variable market demand seen historically the world over.
रोल फॉर्मिंग की तुलना स्टैम्प प्रेस से
| विचार | रोल फॉर्मिंग | स्टैम्पिंग प्रेस |
|---|---|---|
| सेटअप समय | घंटे | दिन |
| लीड टाइम | सप्ताह | महीने |
| टूलिंग लागत | दसियों हजार | सैकड़ों हजार |
| सामग्री उपयोग | 95%+ | 60% |
| Short Run Flexibility | मज़बूत | सीमित |
| उत्पाद जटिलता | सरल प्रोफाइल | उच्च जटिलता प्राप्त की जा सकती है |
तालिका 2. Comparing self lock roof sheeting production via roll forming and large stamping press approaches
For producing mixed niche products across varying monthly volumes efficiently, the flexibility of roll forming solutions deserve consideration when evaluating optimal fabrication system investments supporting both current and projected business over likely decades of changing requirements likely to emerge.
अक्सर पूछे जाने वाले प्रश्न
Q: What thickness and hardness ranges can lines accommodate?
A: Most handle 0.4 – 1 mm thickness across harness levels to Temper 07/3H notoriously difficult to coin stamp without splitting or cracking as strains localized harden exceeding 85% depending on geometry and penetration ratios determine equipment upgrade requirements balancing tonnage against forming stations properly supporting bends completed. Additional secondary process annealing often minimizes refinement stresses although reducing margins so each specification deserves scrutiny evaluating entire production ecosystem capabilities currently installed.
Q: What causes scratching defects on finished roof panels?
A: Buildup, press roll alignment drift or inadequate external blowoff occasionally requires increased vigilant monitoring and maintenance ensuring pristine surface quality production not impacted short or long term. Address root causes rather than applying temporary containment inspecting why problems manifested initially.
Q: Can a single production line handle multiple interlock profile types?
A: Yes, additional quick change roll sets transformed systems enabling mixed products supporting high product varieties still maintaining profitably – flexibility enabling broader building construction panel catalogs competitively. Modern quick tool change solutions make this possible.
Q: What production speed range capability exists on these roll formers?
A: Mechanical lines typically operate around 20 meters per minute. Integrated servo electric lines can achieve 80+ meters per minute output contingent upon installed power, press tonnage transfer and stock decoiler feed rate capabilities all sized appropriately mapping final throughput targets forecast each year. Carefully validate proposed specifications against realistic volume expectations ensuring honest capacity communications.





