
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

अवलोकन
एक OEM पर्लिन रोल फॉर्मिंग मशीन is a specialized industrial equipment system used to continuously mass produce long length metal purlins and girts from coiled steel feedstock for use in original equipment manufactured steel buildings and structures.
Purlins act as structural Z, C or U-shaped roof and wall framing members that support exterior covering materials in metal building systems. Roll formed purlin sections optimize strength-to-weight rations with their vertical web and flange cross-sectional shape.
This guide provides a comprehensive overview of OEM purlin roll former technology, including:
- मशीन के प्रकार और घटक
- The purlin roll forming process
- Design factors and building standards
- Purlin framing applications
- लागत विश्लेषण
- Comparisons with other framing methods
- Leading global manufacturers
Gaining technical insight into OEM purlin roll former capabilities and structural framing assists engineers, contractors and architects evaluating optimized building solutions.
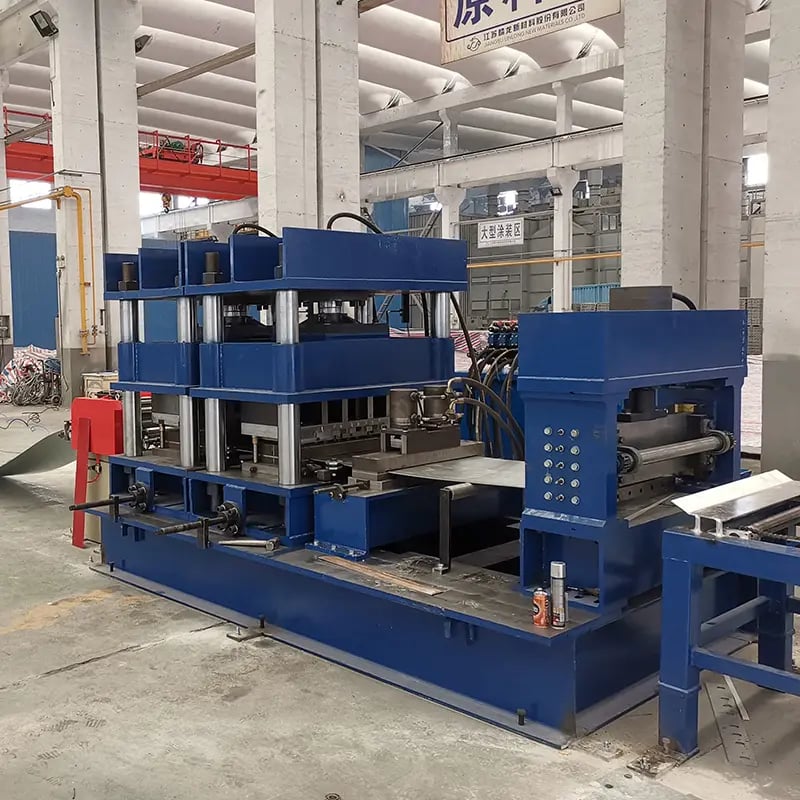
OEM पर्लिन रोल फॉर्मिंग मशीनों के प्रकार
There are two primary machine configurations used for high volume OEM purlin production:
Pyramid-Type Purlin Roll Formers
- Typically 10-16 forming stations in decreasing diameter tiers
- Compact layout, smaller footprint
- Slower production speeds
Inline Purlin Roll Formers
- Stations horizontally inline
- Longer line lengths
- High volume capacity
- Faster cycle times
पर्लिन रोल फॉर्मर के मुख्य घटक
A typical OEM purlin roll forming line integrates these key sections:
कॉइल पेऑफ रील
- Holds raw steel coil
- Powered unwind
प्रवेश गाइड
- Straighten and align strip
- सामग्री फीड को अनुकूलित करें
Accumulator / Bridle
- बैक टेंशन ज़ोन बनाता है
- प्रवाह में होने वाले बदलावों को सुचारु करता है
फॉर्मिंग स्टेशन
- Progressive die rollers shape strip
- संख्या और प्रकार प्रोफ़ाइल निर्धारित करते हैं
कटर
- Pneumatic or servo shear
- Trims finished purlins
Exit Conveyor Table
- Transfers finished lengths
- Supports long products
Automation Controller
- टचस्क्रीन HMI
- Stores recipes
- Production data feedback
पर्लिन रोल फॉर्मिंग मशीनें कैसे काम करती हैं
The OEM purlin roll forming process shapes steel coil strip into C or Z-shaped roof and wall framing sections by bending and forming the feed material incrementally as it passes through a series of roller die stations:
- Powered coil payoff reel feeds raw coiled steel into entry guides
- Guides align strip and feed into initial roller stations
- Rolling dies at each station make gradual precision bends
- Strip exits each stand slightly more formed
- Finished purlin profile emerges at end of line
- Pneumatic shear cuts to length
- Exit conveyor tables transfer finished lengths
The number of roller die stands determines possible purlin profile complexity. Quick change tooling allows fast production changeovers.
-
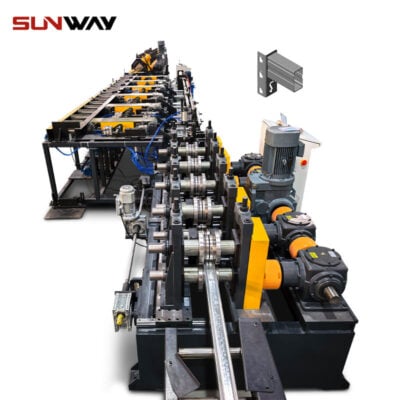 स्टोरेज रैक शेल्फ बॉक्स पैनल बनाने की मशीन, स्टील स्टोरेज रैक सिस्टम बॉक्स बीम रोल फॉर्मिंग लाइन अधिक पढ़ें
-
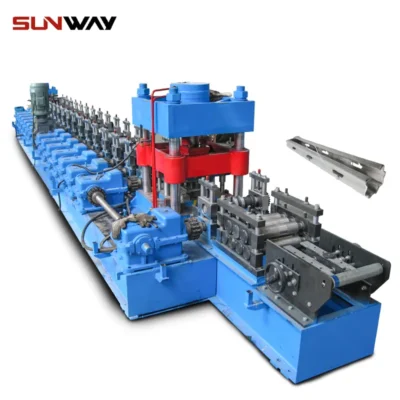 वाइनयार्ड पोस्ट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
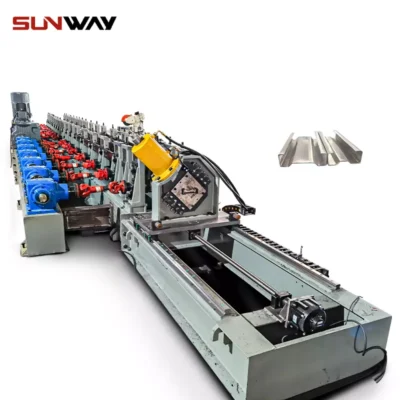 ऑटो साइज चेंजेबल सिग्मा पर्लिन रोल फॉर्मिंग मशीन अधिक पढ़ें
-
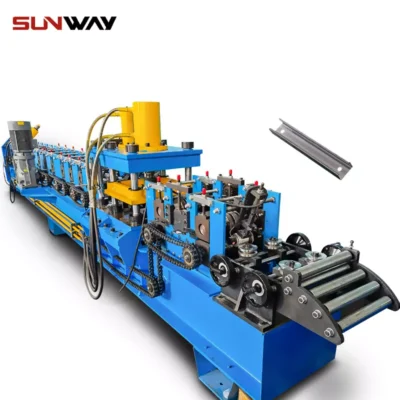 C सेक्शन ब्रेसिंग ओमेगा स्टोरेज रैक अपराइट पोस्ट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
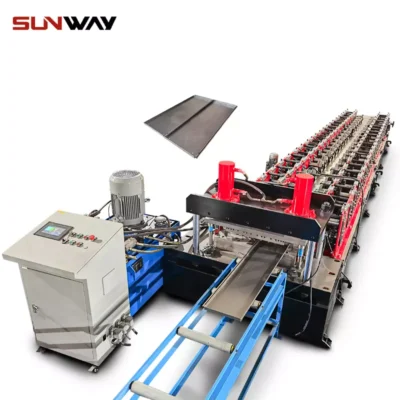 स्टील बॉक्स प्लेट बनाने की रोल फॉर्मिंग मशीन अधिक पढ़ें
-
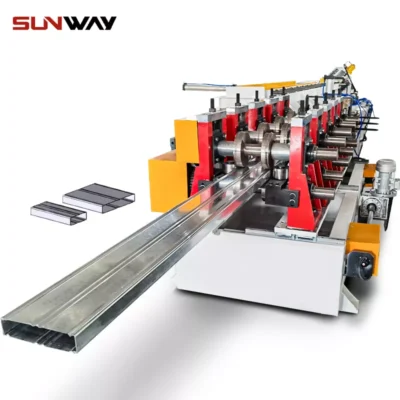 शेल्फ कॉलम के लिए बॉक्स बीम स्टील रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 पैलेट रैकिंग स्टेप बीम P बीम रोल फॉर्मिंग मशीन अधिक पढ़ें
-
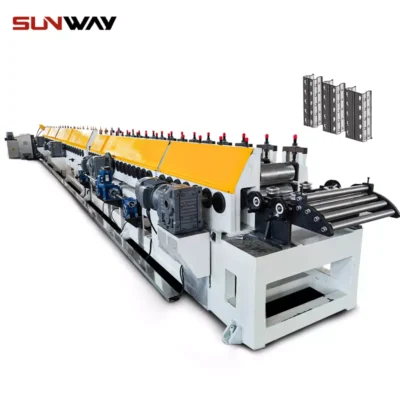 वेयरहाउस शेल्फ अपराइट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
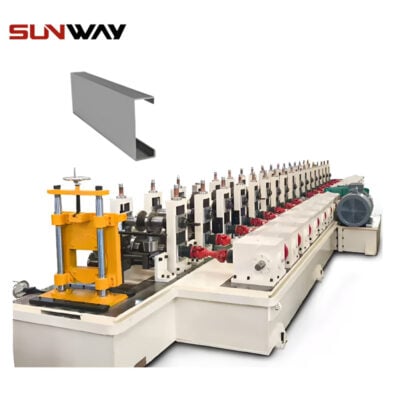 PV माउंटिंग ब्रैकेट C आकार प्रोफाइल रोल फॉर्मिंग मशीन अधिक पढ़ें
पर्लिन रोल फॉर्मिंग के लिए मुख्य डिज़ाइन कारक
Equipment specifiers evaluate numerous characteristics when selecting OEM purlin roll formers:
Building Type
- Pre-engineered steel structures
- Agricultural & commercial spans
- Residential metal roofing
Purlin Type
- Zee, Zed, Sigma
- Narrow flange Cee
- Structural tees
सामग्री
- कम कार्बन स्टील
- उच्च-शक्ति स्टील
- Galvanized coatings
मोटाई
- 16 गेज से 7 गेज
- 1.2mm to 4mm+
प्रोफ़ाइल ऊँचाई
- 75mm to 400mm+
- 3” to 18”+
लाइन गति
- 10 to 35 m/min
- 33 to 115 ft/min
चेंजओवर
- त्वरित बदलाव टूलिंग
- Secondary fab stations
OEM पर्लिन के लिए फ्रेमिंग मानक
While often custom engineered for specific buildings, these standards guide commercial purlin designs:
| मानक | विवरण |
|---|---|
| AISI S100 | North American cold-formed steel framing |
| AS/NZS 4600 | Australian / New Zealand cold-formed steel structures |
| BS 5950 | British cold rolled steel sections |
| EN 1993-1-3 | European cold-formed steel structural framing |
| IS 801 | Indian standard purlin sections |
पर्लिन फ्रेमिंग के सामान्य अनुप्रयोग
Common structural framing applications utilizing OEM roll formed steel purlins include:
Roof Purlins
- Metal building roofing support
- Standing seam roofing
- Single skin systems
Wall Girts
- Exterior metal panel backing
- कर्टेन वॉल फ्रेमिंग
- Interior divide framing
Platform Framing
- Supporting floors
- Structural bridging
- प्लेटफ़ॉर्म छतें
Structural Racking
- Warehouse racks
- मेज़ानाइन
- Equipment platforms
कृषि भवन
- Pole barns
- Grain bin rings
- Storage sheds
Purlin Specifications
| मीट्रिक | सामान्य सीमा |
|---|---|
| ऊँचाई | 75 mm – 400 mm |
| फ्लैंज की चौड़ाई | 30 mm – 100 mm |
| मोटाई | 1.5 mm – 4 mm |
| लंबाई | 2 m – 13 m |
| Load | 3 kN/m – 10 kN/m |
| स्पैन | 1.5 m – 8 m |
अग्रणी OEM पर्लिन रोल फॉर्मर निर्माता
Top international OEM purlin roll former producers include:
| कंपनी | स्थान |
|---|---|
| Formtek | USA |
| Epicenter Machinery | चीन |
| BOTOU Xianfa | चीन |
| Gasparini | इटली |
| Metform | तुर्की |
मूल्य निर्धारण
| मशीन | औसत लागत (USD) |
|---|---|
| Basic Pyramid Roll Former | $92,000 |
| Inline 20-Station Machine | $185,000 |
| High Capacity Servo Line | $430,000 |
| Purlin | Average Cost Per Foot (USD) |
|---|---|
| 12” 18 Gauge Zee | $1.15 |
| 8” 14 Gauge Cee | $1.75 |
| 4” 11 Gauge Sigma | $2.40 |
के लाभ OEM Purlin Roll Forming
लाभ
- उच्च उत्पादन गति
- सटीकता सहनशीलताएँ
- Quality consistency
- Minimal fabrication
- Lower material cost
- Reduced building construction time
सीमाएं
- High machine capital costs
- Mainly long, straight shapes
- Can require secondary punching
- Fixed tooling less flexible
अक्सर पूछे जाने वाले प्रश्न
What is the maximum length of OEM roll formed purlins?
Standard exit conveyor tables allow continuous forming of purlins up to 40′ (12 m). Custom extra long beds can produce sections approaching 65′ (20 m).
What metals can use roll forming for purlins?
All common building steels including low carbon, high strength alloy steels, corrosion resistant alloys as well as lightweight aluminum framing grades.
What if secondary holes or clips are needed in the purlins?
Inline punching presses, drilling machines and clip insertion equipment can be integrated on the exit conveyor to add holes or mounting features.
What is the thickest gauge purlin an OEM roll former can produce?
Average max thickness is around 7 gauge steel or 4mm plate. Heavy duty custom machines can produce structural shapes from 3 gauge steel and beyond.
रोल फॉर्मिंग के बारे में अधिक जानें
अक्सर पूछे जाने वाले प्रश्न (FAQ)
1) Can an OEM purlin roll forming machine switch between C, Z, and Sigma profiles without changing the whole line?
- Yes. Modern OEM purlin roll forming machines support quick-change cassettes or auto-size tooling that swaps out roll sets and adjusts web/flange widths via servo-actuated stands. Changeovers can be under 15–30 minutes on advanced lines.
2) How do I size motor power and line speed for 3 mm high-strength galvanized steel?
- For 3 mm HSS (≥350 MPa), lines typically use 22–45 kW main drives and run 15–30 m/min depending on profile depth and punching density. Accumulators and bridle systems are recommended to maintain tension during punching and cutting. Consult AISI S100 or EN 1993-1-3 for structural limits and required tolerances.
3) What tolerances are typical for OEM C/Z purlins?
- Common production tolerances: web/flange ±0.5–1.0 mm, angle ±0.5°, straightness ≤1.5 mm per meter, bow ≤3 mm per 3 m, hole-to-edge ±0.5 mm (with servo punching). Verify against project specs and local standards (AISI S100, AS/NZS 4600, EN 1993-1-3).
4) Do I need inline punching or can I post-process holes?
- Inline servo punching improves throughput, positional accuracy, and reduces WIP. Post-process turret punching or drilling increases handling costs and risk of distortion. For high-mix OEM orders, consider modular punching stations with programmable tooling.
5) What quality control checks should run per shift?
- Coil cert verification (grade, coating), first-article dimensional audit, hardness and coating thickness spot checks, inline vision for hole pattern, cut-length verification, and periodic straightness/bow checks. Log data via the HMI/MES for traceability (ISO 9001/EN 1090 compliance).
2025 उद्योग रुझान
- Shift to high-strength, low-alloy (HSLA) coils and ZAM/Al-Zn coatings to extend service life in aggressive environments.
- Growth of auto-adjust (size-changeable) C/Z purlin lines with recipe-driven servo stands to reduce changeover downtime in OEM operations.
- Integration of OPC UA/MQTT connectivity and edge analytics for predictive maintenance and scrap reduction.
- Safety and compliance: more OEMs adding EN ISO 14120 guarding, PL d safety circuits, and e-stop zoning.
- Regionalization of coil sourcing and just-in-time slit coil inventory to mitigate logistics volatility.
OEM पर्लिन रोल फॉर्मिंग मशीनों के लिए 2025 के मुख्य मेट्रिक्स
| मीट्रिक | २०२३ सामान्य | 2025 अग्रणी धार | Impact on OEM Purlin Roll Forming Machine ROI |
|---|---|---|---|
| Changeover time (C↔Z, width/depth) | 45–60 मिनट | 8–15 मिनट | +6–10% OEE; faster small-batch runs |
| स्क्रैप दर (स्टार्टअप + स्थिर) | 3.0–4.5% | 1.2–2.0% | Material savings on HSLA coils |
| ऊर्जा उपयोग (kWh/ton) | 95–120 | 70–90 | Lower operating cost, ESG alignment |
| पूर्वानुमानित रखरखाव अपनाना | 20–30% of lines | 55–65% of new lines | कम अनियोजित रुकावटें |
| Inline punching accuracy (± mm) | ±0.7–1.0 | ±0.3–0.5 | Better fit-up, reduces rework |
| Typical line speed (m/min, 2–3 mm) | 15–25 | 20–35 | Higher throughput with servo shear |
Sources: World Steel Association 2025 outlook (https://worldsteel.org), AISI S100 updates (https://www.awc.org/standards/aisi), CEN EN 1993-1-3 developments (https://standards.cen.eu), vendor whitepapers (Formtek, Gasparini, Metform).
नवीनतम अनुसंधान मामले
Case Study 1: Auto-Size C/Z Line Retrofit for HSLA Coils (2025)
- Background: An OEM building systems producer in the EU struggled with 3–4% scrap and 50-minute changeovers on 1.6–3.2 mm galvanized HSLA purlins.
- Solution: Retrofitted servo-driven cassette stands, closed-loop length control with encoder wheel, and OPC UA data layer feeding a predictive bearing wear model.
- Results: Changeover reduced to 12 minutes; scrap to 1.6%; OEE up 8.4%; payback in 11 months. Dimensional Cp/Cpk improved >1.33 on flange width and hole positions. Compliance aligned with EN 1993-1-3 tolerances.
Case Study 2: Integrated Inline Punching and Vision QC for OEM Z-Purlins (2024)
- Background: North American OEM needed rapid variant production with dense hole patterns for solar canopies.
- Solution: Added servo turret punching with quick-change tooling and AI vision for hole presence/position; synchronized with flying shear.
- Results: Throughput +22% at 28 m/min; hole defects down 72%; rework time cut by 40%. Met AISI S100 and ASTM A653 coating integrity criteria.
विशेषज्ञों की राय
- Dr. Helen Park, वरिष्ठ सामग्री इंजीनियर, World Steel Association
- Viewpoint: “HSLA and Al-Zn coatings are delivering longer life purlins without weight penalties. For OEM purlin roll forming machines, consistent coil mechanical properties and slit edge quality are now as critical as tooling geometry.” (https://worldsteel.org)
- Marco Bellini, CTO, Gasparini Industries
- Viewpoint: “Auto-size changeover with servo stands and real-time analytics has moved from nice-to-have to standard. The biggest ROI lever in 2025 is predictive maintenance on bearings and gearboxes tied to vibration and thermal trends.” (https://www.gasparini.com)
- Laura Chen, विनिर्माण प्रणालियों की निदेशक, Formtek Group
- Viewpoint: “Inline punching with digital twins lets OEMs validate hole patterns and cut lengths virtually, minimizing first-article scrap. We’re seeing customers achieve sub-0.5 mm positional accuracy at 30+ m/min.” (https://www.formtekgroup.com)
व्यावहारिक उपकरण/संसाधन
- AISI S100 (North American Specification for Cold-Formed Steel): https://www.awc.org/standards/aisi
- EN 1993-1-3 (Eurocode 3, Cold-formed members): https://standards.cen.eu
- AS/NZS 4600 (Cold-Formed Steel Structures): https://www.standards.govt.nz
- World Steel Association के बाजार पूर्वानुमान: https://worldsteel.org
- Coil Calculator and Bend Allowance Tool (The Fabricator): https://www.thefabricator.com
- OPC UA for Industrial Interoperability: https://opcfoundation.org
- Gasparini Roll Forming का ज्ञान आधार: https://www.gasparini.com/en/knowledge
- Formtek Technical Resources: https://www.formtekgroup.com/resources
- NIST स्मार्ट विनिर्माण संसाधन: https://www.nist.gov/el/smart-manufacturing
अंतिम अपडेट: 2025-10-23
परिवर्तन-लेख: Added 5 new FAQs; inserted 2025 industry trends with performance table; provided two 2024/2025 case studies; included expert opinions with sources; added practical tools/resources
अगली समीक्षा तिथि और ट्रिगर: 2026-03-31 or earlier if AISI/EN standard revisions publish, HSLA coil availability shifts, or predictive maintenance benchmarks change by >10%





