
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

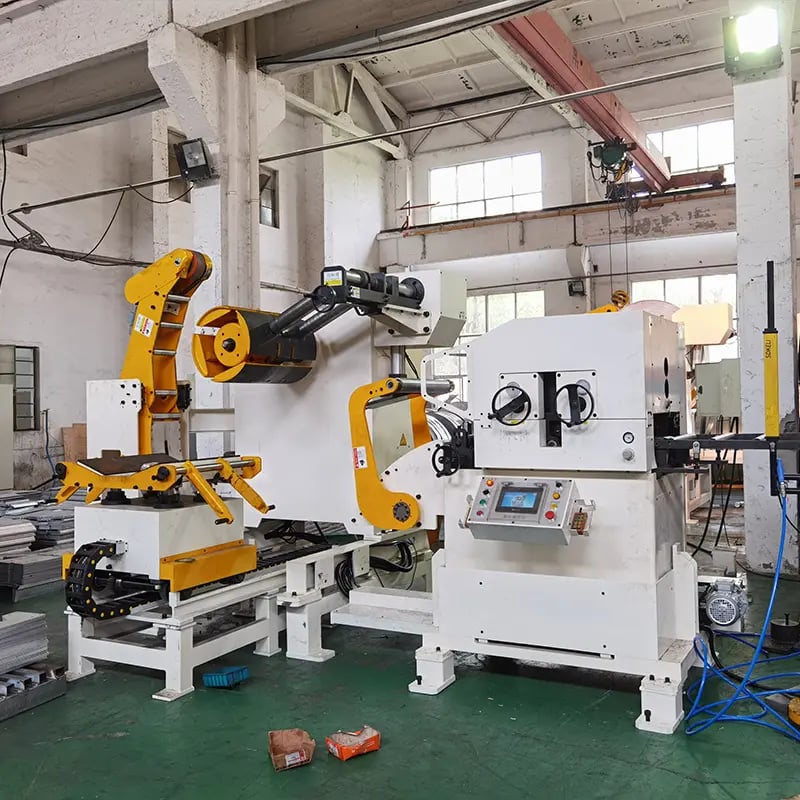
डबल रो स्टड रोल फॉर्मिंग मशीनें continuously form structural metal studs with dual protruding ridges from steel coil feedstocks. The machines utilize a series of roller dies to progressively shape flat strip substrate into C or Z section studs with vertical web and uniform horizontal flange ridges running along both sides of the member length.
This guide covers standard offerings, the roll forming process basics, machine component details, operational guidance, customization possibilities, supplier comparisons, selection factors, pros vs cons considerations, and commonly asked questions regarding double rows stud roll forming line equipment.
डबल रो स्टड रोल फॉर्मिंग मशीन प्रकार
Double rows stud roll former types include manual, automatic, and customized CNC programmable lines (Table 1):
| प्रकार | विवरण |
|---|---|
| मैनुअल | बुनियादी मैन्युअल रूप से समायोज्य रोल डाइज़ |
| स्वचालित | Servo powered auto gauging and speed control |
| मानक | Common stud geometries and sizes |
| अनुकूलित | Special profiles or inline operations |
तालिका 1. Double Rows Stud Roll Former Model Options
The systems integrate with auxiliary uncoilers, feed tables, levelers, saws and exit conveyors.
डबल रो स्टड रोल फॉर्मिंग कैसे काम करती है
The roll forming process utilizes shaped roller dies to incrementally cold form continuous flat strip stock into final stud profiles with two protruding flanges along both sides of the vertical web as it passes through the production line (Figure 1). Steps include:
- Feeding line level sheet into system from coil
- Progressively cold roll forming with upper/lower roller dies
- Bending narrow horizontal flanges uniformly up from web
- Calibrating final profile to intended dimensions
- Shearing cutoff studs to length upon exit
- Accumulating or coiling finished parts
चित्र 1. Double Row Stud Roll Forming Diagram
The number of progressive stands, tooling geometry, and process settings determine the final stud specifications.
डबल रो स्टड रोल फॉर्मिंग उपकरण के घटक
Key system components influencing functionality include (Table 2):
| घटक | विवरण |
|---|---|
| फॉर्मिंग रोलर्स | Solid precision CNC machined roller dies |
| रोलर स्टेशन | Upper/lower die sets responsible for each bend sequence |
| रोलर शाफ्ट | Driven forming roller rotation via gears/chains |
| शीट गाइड | Centered strip guidance during forming |
| फीडिंग सिस्टम | Pulls or pushes strip through roll stations |
| कतराई | Hydraulic cut-off presses slice output |
| डिकॉयलर | Unwinds raw strip coil stock |
| स्वचालन | Servo feed drives, gauging sensors |
तालिका 2. Double Row Stud Roll Former Parts Overview
डबल रो स्टड लाइनों का अनुकूलन
Specialized structural stud requirements involve custom roll forming solutions including:
| क्षेत्र | अनुकूलन की संभावनाएँ |
|---|---|
| Profile geometry | Unique vertical web height, horizontal flange sizes |
| Flange counts | Beyond traditional double rows, additional protrusions |
| चौड़ाई क्षमता | Machines accommodating over 1.5m part widths |
| Tooling materials | Custom metal alloys tailored for niche sheeting grades |
| जोड़े गए संचालन | Hole punching, tapping, offset notch cuts |
| स्वचालन | Advanced servo controls and monitoring |
| सामग्री हैंडलिंग | Decoiler, exit conveyor, pack table options |
| डेटा लॉगिंग | Advanced gauge stats, predictive maintenance |
| सुरक्षा | विस्तारित सुरक्षा कवर, रखरखाव प्लेटफ़ॉर्म |
Close collaboration between engineers and roll tooling specialists enables specialized stud profiles.
डबल रो स्टड रोल फॉर्मर की कीमत और आपूर्तिकर्ता
| निर्माता | स्थान | मूल्य सीमा |
|---|---|---|
| Formtek | USA | $$$$$ |
| Gasparini SPA | इटली | $$$ |
| Hangzhou Roll Form | चीन | $$ |
| Zhejiang New Shengda | चीन | $$ |
| CustomPartNet | USA | $$$$ |
तालिका 3. Double Row Stud Roll Forming Equipment Suppliers and Prices
Cost ranges span from $10,000 for elementary Chinese machinery up to $300,000+ for sophisticated American lines engineered for high production environments.
डबल रो स्टड रोल लाइनों के संचालन की प्रक्रियाएँ
कुशल निरंतर संचालन प्रक्रियाओं में शामिल हैं:
| गतिविधि | विवरण |
|---|---|
| सेटअप | Stage strip coils, thread through stands, set feed rates, test run profiles, finalize calibrations |
| संचालन | Monitor sheet tracking/alignment, confirm output dimensional uniformity via gauging, log any errors |
| रखरखाव | Replace worn rollers, lubricate bearings/slides, calibrate automation controls |
तालिका 4. Double Row Stud Roll Former Procedures
Schedule preventative maintenance appropriately to minimize unplanned downtime. Continuously inspect output profile correctness.
डबल रो स्टड रोल उपकरण के तुलना कारक
| विचार | विवरण |
|---|---|
| Annual volume targets | Match acceptable process speeds to output needs |
| पार्ट के आयाम | Check against machine width capacities and die access |
| सामग्री गुण | मज़बूती, अनुमत मोटाई सीमा |
| जोड़े गए संचालन | Requirements for hole punching/notching |
| बजट सीमाएँ | उत्पादन उद्देश्यों बनाम पूंजीगत व्यय |
| स्थान संबंधी कारक | Available qualified global machinery supply sources |
| मापनीयता | भविष्य के अतिरिक्त टूलिंग, क्षमता वृद्धि |
Analyze current and future projection requirements against machine specifications and supplier expertise.
-
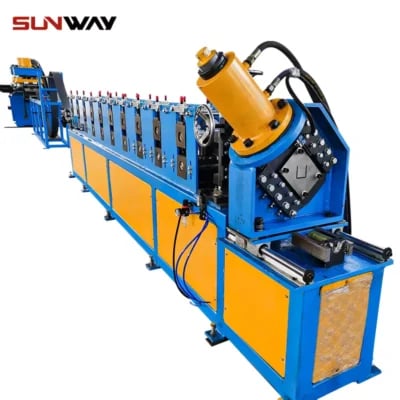 इलेक्ट्रिकल कैबिनेट फ्रेम रोल फॉर्मिंग मशीन अधिक पढ़ें
-
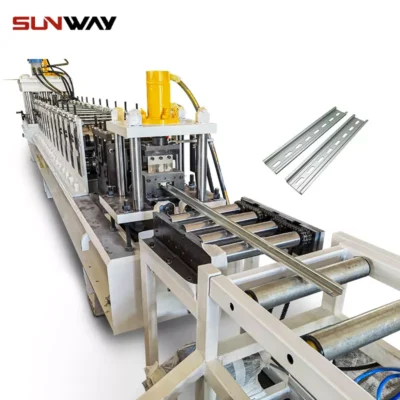 Din रेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
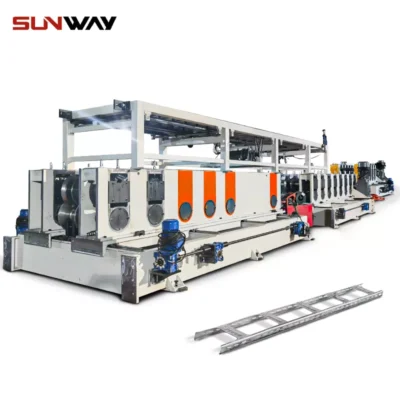 केबल लैडर रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 PV माउंटिंग ब्रैकेट C आकार प्रोफाइल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 केबल ट्रे रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 PV माउंटिंग ब्रैकेट रोल फॉर्मिंग मशीन (HAT / Omega प्रोफ़ाइल) अधिक पढ़ें
-
 PV माउंटिंग ब्रैकेट Z आकार प्रोफाइल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 सोलर माउंटिंग स्ट्रट चैनल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 स्ट्रट चैनल रोल फॉर्मिंग मशीन अधिक पढ़ें
डबल रो स्टड लाइनों के लाभ और हानियों का मूल्यांकन
| लाभ | हानियां |
|---|---|
| उच्च गति वाली निरंतर प्रोसेसिंग | प्रारंभिक मशीनरी पूंजी निवेश |
| Consistent uniform output stud quality | अनुकूलित टूलिंग लागत |
| उच्च आयामी सटीकता मानक | सेटअप/चेंजओवर डाउनटाइम आवश्यकताएँ |
| मूल सामग्री के गुणों का संरक्षण | संचालन और रखरखाव कौशल की आवश्यकताएँ |
| कच्ची सामग्री का सीमित अपशिष्ट | मॉडल के अनुसार आकार सीमा की बाधाएँ |
| अतिरिक्त स्टेशनों के माध्यम से विस्तार-क्षमता | सटीक निगरानी आवश्यक |
तालिका 5. Double Row Stud Roll Former Benefits vs Limitations
When applied appropriately for sufficient volumes, roll forming offers clear manufacturing performance advantages over alternate fabrication approaches.
अक्सर पूछे जाने वाले प्रश्न
What thickness range can double rows stud roll formers handle?
Standard models process material thicknesses from 0.75mm – ~5mm hot rolled coils and galvanized sheet products. Thinner gauges depend on required bend radii while thickness equates to drive power.
How fast do these machines operate?
Typical production line speeds averaging 10-15 meters per minute enable rapid processing suited for most structural metal stud volume requirements. Appropriate feed power settings prevent tearing.
What expertise is recommended for operation?
Some automation eases skill requirements, however mechanical fabrication experience proves helpful for optimizing output through procedural adjustments and troubleshooting quality issues.





