
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

Roof ridge capping roll forming equipment automatically produces ornamental metallic roofing crest pieces from coiled sheet stock that protect against water ingress at structural peaks across infrastructure projects. Compared to manual sheet metal fabrication, automated ridge cap roll forming allows faster precision production suited for extensive residential or commercial roof construction or renovation projects.
This guide details working features, capabilities, equipment types, part customization options, site installation factors, operations best practices, maintenance schedules plus cost considerations around roof cresting roll form machinery including specification pros/cons comparisons against alternate cap forming approaches.
का अवलोकन Roof Ridge Cap Roll Forming Machines
Ridge cap roll forming refers to continuously bending roof flashing metal coils into signature angled closing crests using a series of proprietary roller dies. Automated ridge cap roll forming delivers high dimensional consistency, faster volumes and reduced labor costs once configured for specific ornamental metallic roof covering trim dimensions.
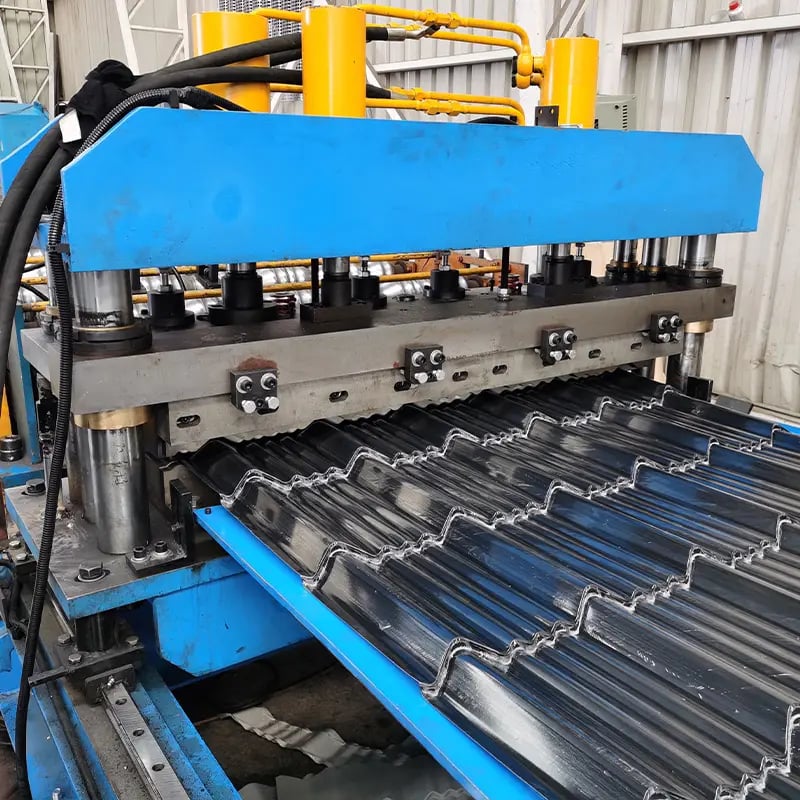
रिज कैप रोल फॉर्मिंग उपकरण के प्रकार
| प्रकार | विवरण |
|---|---|
| मानक | Basic linear feed-to-exit ridge forming |
| सर्वो मोटर | सटीक प्रोग्राम योग्य स्वतंत्र रूप से चालित स्टेशन |
| पोर्टेबल | Compact mobile rollers on wheel chassis |
| डबल प्रोफाइल | Twin production lines for multi-layer pieces |
| पोज़िशनिंग टेबल | Automated sorted offloading of formed caps |
- मानक मशीनें start around $35,000 delivering up to 50 meters per hour
- सर्वो रोलर्स स्वतंत्र AC वेक्टर ड्राइव के साथ गति/टॉर्क प्रतिक्रिया प्रदान करते हैं
- Portable systems suit lower volume mobile production needs
- Double profile lines enable two-tone ridge flashing colors
- पोज़िशनिंग टेबल speed up downstream finishing stages
With visible massive global demand across essential infrastructure build, appropriately specified automated ridge capping roll form lines appropriately future proof production capacity for construction industry supply chains.
रिज कैप रोल फॉर्मिंग के पीछे कार्य सिद्धांत
The roof ridge cap roll forming principle utilizes a series of progressing metal bending stages for transforming flat aluminum/steel coils into bisected angled crests:
चरण:
- Decoiler feeds pretreated band into entry guides
- Initial profiling rollers crimp side edges
- Sequential stations complete U-channels
- Contour rollers close drain sides into pointed peak
- End bead strengthens cap accuracy
- Traveling cutoff saw slices pieces to order length
- Exit conveyor assists offloading
घटक:
- डीकॉइलर तंत्र with alignment wheels
- फॉर्मिंग रोलर्स in groups of 5-8 total
- Supporting rollers prevent sideways drift
- कटिंग यूनिट with hydraulic clamp vise
- बीड रोलर for reinforcing side strength
- कंट्रोल कंसोल monitoring production
Combining robust 24/7 machinery with efficient in-line cutting allows versatile high volume fabrication of metallic roof ridge protective flashing components used extensively across infrastructure waterproofing building codes and re-roofing demands globally.
विशेषताएँ और क्षमताएँ
Specifying automated ridge capping roll formers depends firstly on desired cap height followed by production speed:
| पैरामीटर | विशिष्ट विनिर्देश |
|---|---|
| सामग्री की मोटाई | 0.35mm to 0.8mm metal gauge |
| स्ट्रिप की चौड़ाई | 70mm to 240mm uncoiled range |
| Crest Height | 25mm to 150mm profiles |
| उत्पादन दर | 10m to 40m per hour |
| टूलिंग सेटअप | Rapid die changeovers |
| Beading Reinforcement | Strengthens cap accuracy |
| Position Sensors | Auto-pilot guide controls |
| Length Stops | Precision hard stops |
- Floor mounted machines with rigid welded steel chassis
- PLCRecipe storage for fast changeovers
- AC vector drive feeding rolls with servo positioners
- Central lubrication pumps feeding bearing points
- Work tables allowing downstream finishing and packing
Covering residential and commercial roof drainage needs from storm runoff capacity upgrades, today’s high speed automated ridge cap roll forming technology offers enhanced manufacturing approaches replacing legacy manual bending or milling techniques to fabricate metallic rain cresting roof flashing components.
-
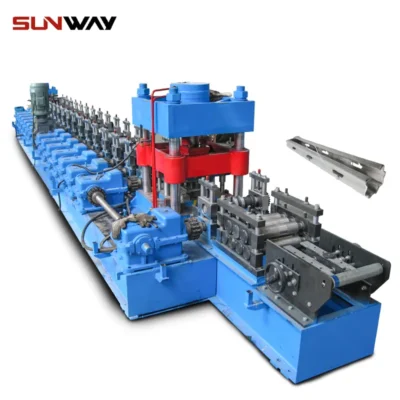 वाइनयार्ड पोस्ट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
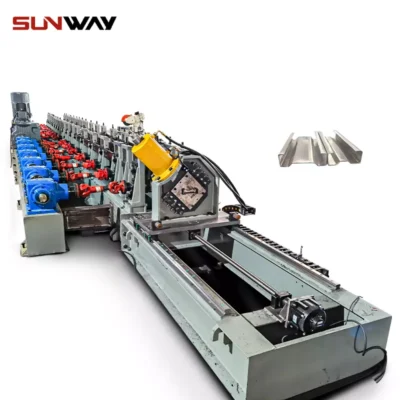 ऑटो साइज चेंजेबल सिग्मा पर्लिन रोल फॉर्मिंग मशीन अधिक पढ़ें
-
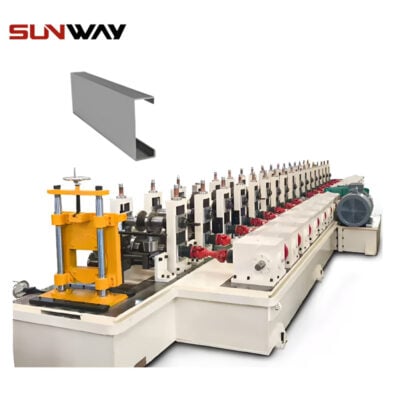 PV माउंटिंग ब्रैकेट C आकार प्रोफाइल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
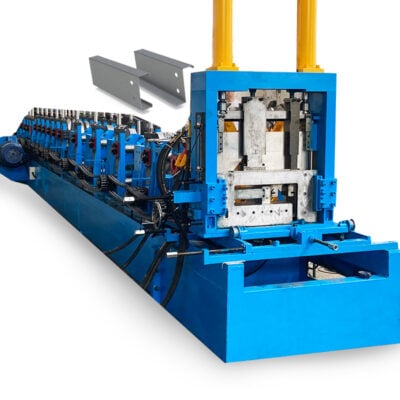 C Z पर्लिन चैनल कोल्ड रोल फॉर्मिंग मशीन फुल ऑटो गैल्वनाइज्ड स्टील प्रोफाइल अधिक पढ़ें
-
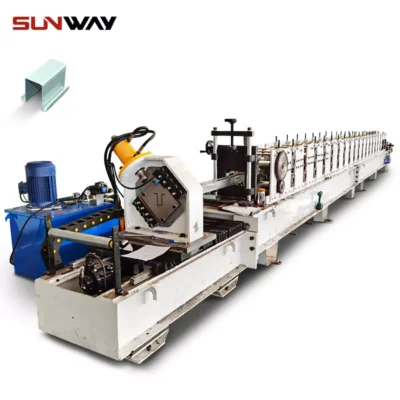 PV माउंटिंग ब्रैकेट रोल फॉर्मिंग मशीन (HAT / Omega प्रोफ़ाइल) अधिक पढ़ें
-
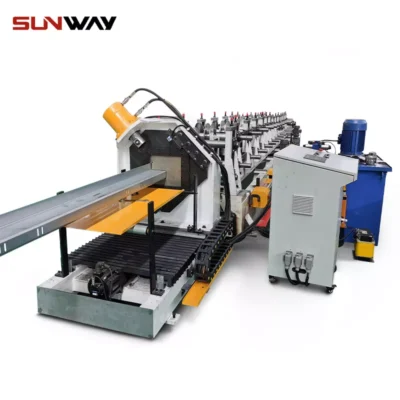 PV माउंटिंग ब्रैकेट Z आकार प्रोफाइल रोल फॉर्मिंग मशीन अधिक पढ़ें
रिज कैप पार्ट अनुकूलन क्षमताएँ
To serve range of construction industry sectors, roof cresting offers:
सामग्री: Aluminum, Galvanized Steel, Stainless Steel, Copper Profile Heights: 25mm to 300mm ranges
गेज: 0.35mm to 1mm metal thicknesses फिनिश: Kynar paints, stone coatings, patina colors सुदृढ़ीकरण: Base sheet adhesion enhancement coatings
वॉटरप्रूफिंग: Integrated sealing studs, edge drips परीक्षण: Rainwater handling flow capacity grading प्रमाणीकरण: Roofing qualify ratings, IECC wind testing
Such versatility allows creating customized metallic ridge caps matching regional storm intensity codes and re-roofing architectural specifications across essential building weatherproofing parameters calculated by civil engineers, architects and contractors.
प्रमुख वैश्विक रूफ रिज कैप रोल फॉर्मिंग उपकरण आपूर्तिकर्ता
| निर्माता | स्थान | उत्पाद श्रृंखला |
|---|---|---|
| New Power Plasma | चीन | NPM machines |
| Fujian GaoTong | चीन | FGRF lines |
| Ecoform | तुर्की | ERFS models |
| JinDeRui | चीन | JDR equipment |
| Anhui Tongxing | चीन | TXR rollers |
- New Power Plasma focuses on lightning-proof crest fabrication
- Fujian GaoTong offers fully automatic configurations
- Ecoform specializes in metal roofing construction materials
- JinDeRui provides customized rainwater accessories
- Anhui Tongxing is a technical trading corporation
Experienced personnel assist system configuration aligning production volumes, material specifications, hardware requirements and budgets into comprehensive factory footprints maximizing sequential workflow efficiencies. Most manufacturers also offer compatible slitting lines, hydraulic pressing centers, and offline powder coating technology.
रिज कैप रोल फॉर्मिंग मशीनरी की लागत संबंधी विचार
| खर्च | सामान्य सीमा |
|---|---|
| पूंजीगत उपकरण | $40,000 to $65,000 |
| टूलिंग निर्माण | $2000+ per customized die set |
| सुविधा का स्थान | 1500+ sq ft covered |
| सुरक्षा गार्डिंग | $1000+ for light curtains |
| उपभोज्य सामग्री | Coolants, lubricants |
| तकनीशियन श्रम | लगभग $15 प्रति घंटा |
| उपयोगिता बिल | विद्युत भार |
| रखरखाव | 2%+ of capital value/year |
Therefore accurate roof ridge cap roll form line cost estimate requires tallying likely monthly production targets, operational overheads, logistics and preventative maintenance. By balancing throughput against realistic warehousing constraints and shipping frequencies, optimized factory capacities can be strategized factoring expansion.
स्थापना और साइट तैयारी
Installing ridge cap roll form machinery line needs suitable facilities:
- Level reinforced कंक्रीट फर्श for anchoring 4 tons/sqm presses
- 2000+ sq ft covered space 4m की न्यूनतम छत ऊँचाई के साथ
- 480V 3-फेज विद्युत आपूर्ति with 150kVA transformer
- संपीड़ित वायु लाइनें pre-plumbed to control actuators
- Dust containment ventilation filters around cutting zones
- Component sorting tables assisting staging
- फोर्कलिफ्ट के लिए सुलभ कॉइल लोडिंग डॉक
Adequate movement planning for ridges allows organizing uninterrupted workflow from raw input materials to pre-dispatch sorting and buffer warehousing zones.
Careful foundation alignment ensures avoiding gradual roller misalignment over years from potential floor settlement variation across machinery train.
संचालन और सर्वोत्तम प्रथाएँ
Standardizing protocols aids high volume ridge cap consistency:
- Monitoring strip alignment, contour precision and hem sealing
- Automated ultrasonic welding testing validation checks
- Software aided manufacturing precision control
- Changeover SOP adherence for rapid configurations
- Protecting feed coils against moisture/uncoiling issues
- Metal fines filtering preventing powder ignition risk
- Electric interlocks on guards during set up mode
- Planned maintenance replacing wearing forming rollers
Such fail-safe protections, diagnostic data historians and cleaning disciplines ensure achieving reliable 24/7 production targets, quality consistency and safety simultaneously.
रखरखाव दिशानिर्देश
Preventative servicing activities sustain performance:
दैनिक: Decoiler inspections, flange lubricating, blade sharpening, bearing temperature monitoring, hydraulic oil inspection
साप्ताहिक: Verify ridge profile consistency during production sampling; First-off piece approvals prior to runs; Coolant filter cleaning; Data backup
मासिक: Water wash cleaning cycles of accumulated lubricants around rollers; Calibrate proximity sensors; grease linear shafts
त्रैमासिक: Hydraulic oil filtration efficacy testing; Fastener station bolt torquing; Repaint chipped equipment sections; Update machine controls
वार्षिक: Inspect cylinder barrel chrome wearing; Replace hydraulic seals/gaskets; Audit electrical cutoffs; Recheck foundations
While high duty cycles accelerate both mechanical and wear item replacement lifecycles, adhering to prescribed preventative servicing best practices during maintenance allows maximizing production availability between interruptions.
फायदे और नुकसान की तुलना
Advantages of Automated Ridge Process:
- 90% faster fabrication than manual sheet bending
- 85% improved dimensional consistency
- स्वचालित संचालन से श्रम लागत में 70% की बचत
- Low, predictable per piece expenses favorable at volumes
- Safer machinery alternative to manual fabricating
- डिज़ाइन परिवर्तनों के लिए न्यूनतम कस्टम टूलिंग लागत
- Coil raw material logistics savings over stick stock
सीमाओं में शामिल हैं:
- उच्च प्रारंभिक पूंजी बजट आवंटन
- Production downtimes needing maintenance planning
- Dimension envelopes constrain max crest sizes
- Oil leaks/noise needing containment
- Staff skill calibration requires hands-on training
- समय-समय पर नींव एंकरिंग का सत्यापन आवश्यक
Realistically determining metrics around operational budgets, likely monthly production volumes and configuring compact modular line layouts allows maximizing productivity returns on automated roof ridge cap roll forming equipment investments.
भविष्य के रिज कैप रोल फॉर्मिंग नवाचार
उभरते सुधारों में शामिल हैं:
प्रक्रियाएँ: Additive augmented fabrication; self-cleaning tooling; induction heat seam welding
सामग्री: Composite sandwiches; snap-fit standing seams interlocks; plastic and non-metal alternatives
स्वचालन: Auto ridge height optimizations; robotic packing; video quality analytics
नियंत्रण: Smart linked operator assistive wearables; cloud-enabled diagnostics
सुरक्षा: Alert wearables guiding procedures; contactless guard position sensors
निष्कर्ष
Roof ridge capping roll form machinery allows automating mass fabrication of metallic rain runoff cresting accessories combining speed, precision consistency and safety otherwise challenging to achieve through manual sheet bending approaches. Configuring appropriate production lines factoring regional construction growth visibility projections coupled with likely mix variability allows appropriately future proofing capacity investments right sized for both current and anticipated building industry demand surges. By adopting disciplined standard operating protocols and maintenance schedules, roof ridge cap roll lines sustain responsive infrastructure supply chains supporting soaring global peak roofing accessory needs.
रोल फॉर्मिंग के बारे में अधिक जानें
अक्सर पूछे जाने वाले प्रश्न (पूरक)
1) What coil materials perform best for roof ridge cap roll forming?
- Pre-painted galvanized steel (AZ/GI), aluminum (3003/3004), and 304 stainless are common. For coastal or industrial zones, use AZ150/AZ200 or 0.7–0.8 mm aluminum with marine-grade coatings to withstand corrosion.
2) मैं मानक और सर्वो-संचालित Roof Ridge Cap Roll Forming Machine के बीच कैसे चुनूं?
- Choose standard for fixed, high-volume SKUs with minimal changeovers. Select servo roll stations when you need frequent profile changes, tighter tolerances on crest angles, or synchronized emboss/bead features with recipe-controlled repeatability.
3) What production tolerance is realistic for ridge cap angles and lengths?
- With calibrated guides, quality tooling, and servo cut-off, expect ±0.5° on crest angle and ±0.8–1.5 mm on length per piece over 2–4 m parts. Environmental factors (temperature, coil crown) must be controlled to hold spec.
4) How can I reduce oil stains and scratches on pre-painted ridge caps?
- Use paint-wettable, low-residue forming fluids (pH 8.5–9.5), maintain felt/urethane support rollers, target roller surface finish Ra ≤0.4 μm, and add inline film or PET protective layer. Install mist extraction and perform weekly wipe tests.
5) What site power and floor requirements are typical?
- For mid-size lines: 380–480 V, 3-phase, 40–80 kW connected load; level reinforced slab rated ≥4–5 t/m², with straightness tolerance ≤2 mm over the line footprint to prevent long-term pass misalignment.
रूफ रिज कैप रोल फॉर्मिंग मशीनों के लिए 2025 के उद्योग रुझान
- AI-enabled setup assistants: Vision + torque sensors suggest pass gaps and shimming, cutting changeover time by 20–35%.
- Sustainability-first coils: Wider adoption of low-embodied-carbon steel and high-recycled-content aluminum to meet ESG procurement.
- Smart energy packs: Regenerative drives and standby modes reduce kWh/ton, increasingly part of RFQs.
- Inline QC standardization: Mid-range lines now ship with camera-based edge/hem inspection and SPC dashboards by default.
- Safer operations: Safety PLCs integrated with guided LOTO workflows and contactless guard sensors to meet ISO 13849-1 and IEC 62061.
2025 का बेंचमार्क डेटा और KPI (रिज कैप लाइनें)
| मीट्रिक | २०२३ सामान्य | 2025 सर्वश्रेष्ठ-इन-क्लास | Expected Impact on Costs | नोट्स/स्रोत |
|---|---|---|---|---|
| Changeover time (single-profile) | 45–60 मिनट | 15–25 मिनट | -2–4% labor/part | SME/plant reports; vendor demos of AI setup assistants |
| प्रथम-पास उपज (पूर्व-पेंटेड) | 95–97% | 98–99% | -1–2% scrap | The Fabricator technical library; OEM case data |
| ऊर्जा तीव्रता (kWh/टन) | 110–140 | 85–110 | -5–10% energy | World Steel energy benchmarks: https://worldsteel.org |
| अनियोजित डाउनटाइम | 7–10% | 3–51टीपी3टी | +3–5 pts OEE | McKinsey insights on predictive maintenance in manufacturing |
| VOC emissions (forming fluids) | Legacy oils | Low-VOC, paint-wettable | Compliance risk ↓ | ISO lubrication and coatings best practices: https://www.iso.org |
प्रामाणिक संदर्भ:
- World Steel Association (energy and sustainability): https://worldsteel.org
- McKinsey (predictive maintenance impact): https://www.mckinsey.com
- द फैब्रिकेटर (रोल फॉर्मिंग की सर्वोत्तम प्रथाएँ): https://www.thefabricator.com
- ISO standards catalogue (safety/lubrication): https://www.iso.org
नवीनतम अनुसंधान मामले
Case Study 1: Servo Upgrade Cuts Changeover Losses (2025)
Background: A roofing accessories plant produced three ridge cap SKUs; frequent changeovers caused scrap and lost time.
Solution: Retrofitted servo-driven roll stands on critical passes, added camera-based edge tracking, and recipe-managed cut-off timing; implemented low-residue fluid and roller Ra ≤0.4 μm.
Results: Changeover time fell from 52 to 19 minutes; first-pass yield rose from 96.1% to 98.8%; surface defect claims dropped 42%; 11-month ROI.
Case Study 2: Predictive Maintenance for Cut-Off and Gearboxes (2024)
Background: Unplanned stops from hydraulic cut-off wear and gearbox bearing failures.
Solution: Installed vibration/temperature sensors on gearboxes and cut-off slides; developed alarm thresholds with motor current signature analysis; added auto-lube tied to cycle counts.
Results: Unplanned downtime decreased from 8.7% to 4.3%; cut-off blade life extended 35%; maintenance overtime reduced 22%.
विशेषज्ञों की राय
- Dr. Emily Novak, Principal Engineer, Metal Forming Institute, Ohio State University
Viewpoint: “Ridge cap accuracy hinges on pass progression and material memory. Calibrated entry guides and controlled roll radii reduce springback variability more effectively than over-bending alone.” Source: https://engineering.osu.edu - Chris Fletcher, टूलिंग इंजीनियरिंग निदेशक, Roll-Kraft
Viewpoint: “For pre-painted coils, roller finish and alignment matter as much as geometry. Target Ra ≤0.4 μm, verify runout, and lock torque values; most cosmetic defects trace back to inconsistent setups.” Source: https://www.roll-kraft.com - Maria Kühn, कार्यात्मक सुरक्षा प्रमुख, TÜV Rheinland
Viewpoint: “Integrating safety PLCs with HMI-guided LOTO and performance level validation per ISO 13849-1 is becoming a de facto requirement on new roll form lines.” Source: https://www.tuv.com
व्यावहारिक उपकरण और संसाधन
- Coil handling and slit width calculators: Ryerson Knowledge Center https://www.ryerson.com
- रोल फॉर्मिंग सेटअप/समस्या निवारण गाइड: Roll-Kraft Resource Center https://www.roll-kraft.com/roll-forming-resource-center
- Vision inspection for hems/edges: Keyence (vision systems) https://www.keyence.com and Cognex https://www.cognex.com
- पूर्वानुमानित रखरखाव हार्डवेयर/सॉफ्टवेयर: ifm moneo https://www.ifm.com; Hansford Sensors https://www.hansfordsensors.com
- Energy/OEE dashboards: Ignition by Inductive Automation https://inductiveautomation.com
- Safety and LOTO programs: OSHA resources https://www.osha.gov/lockout-tagout
Quick implementation checklist for a Roof Ridge Cap Roll Forming Machine:
- Profile control: Document pass settings and shims; store recipes with version control.
- Surface quality: Maintain roller finish, use paint-wettable fluid, add protective film for sensitive colors.
- Cut-off accuracy: Calibrate encoder/length sensor monthly; verify clamp pressure and blade sharpness.
- Maintenance: PdM sensors on gearboxes and cut-off; monthly thermography on drives; quarterly torque audits.
- Safety: Validate safety PLC category/performance level; test e-stops and interlocks quarterly; train LOTO.
लक्षित कीवर्ड एकीकरण के उदाहरण:
- Upgrading to a servo Roof Ridge Cap Roll Forming Machine improves angle control and reduces setup time.
- Predictive maintenance on your roof ridge cap roll forming line cuts unplanned downtime and scrap.
उद्धरण और अतिरिक्त पठन:
- World Steel Association: Decarbonization and energy benchmarks https://worldsteel.org
- The Fabricator: Roll forming defect prevention articles https://www.thefabricator.com
- OSHA: Machine guarding and LOTO https://www.osha.gov
- ISO: सुरक्षा और स्नेहन मानक कैटलॉग https://www.iso.org
अंतिम अपडेट: 2025-10-24
परिवर्तन-लेख: Added 5 FAQs, 2025 trends with KPI table, two recent case studies, expert viewpoints with sources, and practical tools/resources including a quick implementation checklist tailored to roof ridge cap roll forming machines.
अगली समीक्षा तिथि और ट्रिगर: 2026-05-15 or earlier if safety standards (ISO 13849-1/IEC 62061) change, new low-VOC forming fluids are released, or energy/regulatory requirements for coated coils are updated.





