
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

Double furring ceiling roll forming machines are used to produce double furring ceiling panels from coil metal sheets. This advanced equipment forms the sheet metal into specialized ceiling panel profiles with double furring features.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग मशीन Equipment Guide
| उपकरण प्रकार | विवरण |
|---|---|
| कॉइल फीडर | Unwinds metal coil and feeds into roll former |
| रोल फॉर्मिंग स्टेशन | Progressively form the sheet into desired profile with rolls |
| पंचिंग इकाई | Punches holes for installation |
| कटिंग मशीन | Cuts formed panels to required length |
This core equipment produces the double furring panels. Additional equipment can be added for automation:
- Decoilers for easy coil loading
- Coil car for moving coils
- Welding machine to weld framing
- Supporting conveyors
- हाइड्रॉलिक सिस्टम
- कंट्रोल पैनल
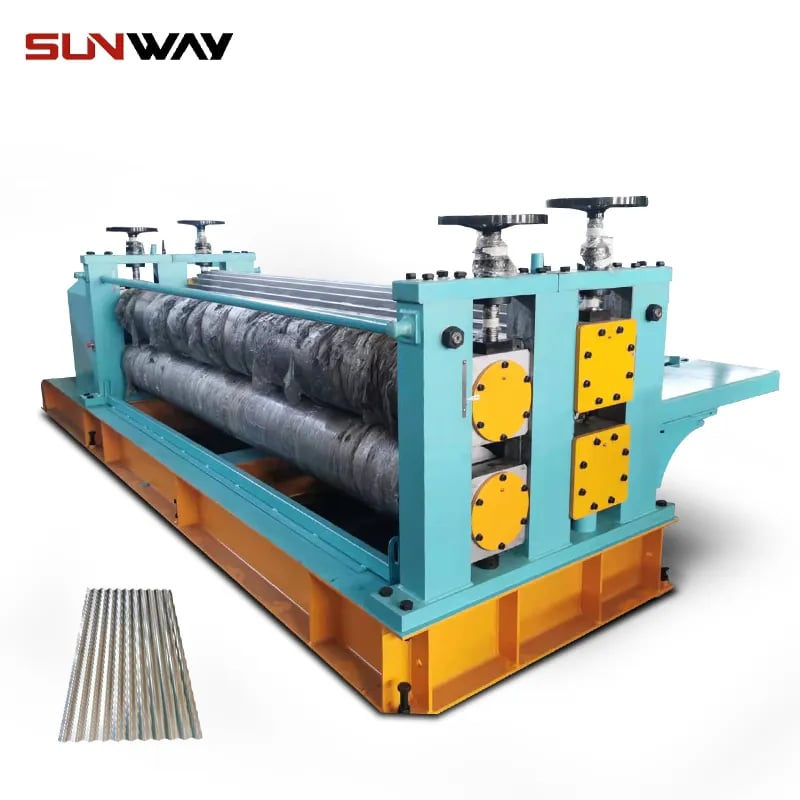
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग प्रक्रिया
The double furring ceiling roll forming process starts by loading a coil of thin gauge metal sheet into thedecoiler or coil feeder. The sheet gets unwound and fed into the rolling stations.
Each rolling station progressively forms the sheet further with precision rolls. The stations bend and shape the sheet into the desired double furring panel profile. Common profiles include box ribbed, wedge, butterfly, wave, and other geometric patterns.
As the formed sheet exits the last station, it moves through the punching unit. This punctures installation holes into the panel at fixed intervals.
Finally, the cutting machine slices the long panel at the required length into individual pieces. The finished double furring ceiling panels exit the roll former automatically.
This continuous roll forming process can create panels of any length by adjusting the cut-off position. Operators can select custom lengths per project requirements.
-
 इलेक्ट्रिकल कैबिनेट फ्रेम रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 Din रेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 केबल लैडर रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 PV माउंटिंग ब्रैकेट C आकार प्रोफाइल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 केबल ट्रे रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 PV माउंटिंग ब्रैकेट रोल फॉर्मिंग मशीन (HAT / Omega प्रोफ़ाइल) अधिक पढ़ें
-
 PV माउंटिंग ब्रैकेट Z आकार प्रोफाइल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 सोलर माउंटिंग स्ट्रट चैनल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 स्ट्रट चैनल रोल फॉर्मिंग मशीन अधिक पढ़ें
डबल फ्यूरिंग सीलिंग पैनल सामग्री
| सामग्री | विशेषताएं |
|---|---|
| गैल्वनाइज्ड स्टील |
|
| एल्यूमिनियम |
|
| कोल्ड रोल्ड स्टील |
|
| प्री-पेंटेड स्टील |
|
Galvanized steel is the most common choice for roll formed double furring panels due to its optimal balance of strength, corrosion resistance, fire safety, and cost-effectiveness.
डबल फ्यूरिंग सीलिंग पैनल डिज़ाइन
The double furring panel design is engineered for:
- Structural strength and rigidity
- Acoustic insulation properties
- Integration with lighting, HVAC, fire prevention systems
- Aesthetic appearance
- स्थापना में आसानी
Critical design factors include:
- धातु की मोटाई और ग्रेड
- Panel height
- Furring dimensions and geometry
- Hole spacing and size
- Curvature – linear or tapered
- Surface coating – galvanized, painted etc.
Complex software simulations help optimize the panel parameters to meet architectural and engineering specifications.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग प्रक्रिया स्वचालन
| समतल | विवरण |
|---|---|
| मैनुअल | Operators control all functions like feeding, cutting, part handling |
| अर्ध-स्वचालित | Some tasks automated like coiling feed, cutting length |
| पूर्णतः स्वचालित | Complete in-line production with automated material flow |
Higher automation reduces labor and increases output, but also raises investment costs. The optimal level depends on production volume and cost targets.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग उत्पादन दर
| धातु की मोटाई | अधिकतम गति | आउटपुट |
|---|---|---|
| 0.3 mm | 18 m/min | 500 m2/hr |
| 0.4 mm | 15 m/min | 400 m2/hr |
| 0.5 mm | 12 m/min | 300 m2/hr |
Thinner gauges can run at higher speeds and output. Heavier gauges like 0.6-0.8 mm can go up to 8 m/min.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग उपकरण आपूर्तिकर्ता
| कंपनी | स्थान |
|---|---|
| Btianjing | चीन |
| Zhongliang | चीन |
| JinDeLi | चीन |
| Eagle National | संयुक्त राज्य अमेरिका |
| Metform | तुर्की |
China has the most double furring roll forming equipment manufacturers, offering cost-effective machines. Western suppliers provide higher precision and automation options.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग उपकरण की लागत
| उत्पादन दर | स्वचालन | मूल्य सीमा |
|---|---|---|
| 100 m2/hr | मैनुअल | $8,000 – $15,000 |
| 300 m2/hr | सेमी-ऑटो | $18,000 – $25,000 |
| 500 m2/hr | पूर्णतः स्वचालित | $28,000 – $38,000 |
Higher production volumes and automation levels increase costs. Additional equipment for decoiling, conveying, and fabrication can further raise investment.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग उपकरण की स्थापना
- Carefully plan equipment layout to optimize material and part flow
- Ensure adequate space on all sides for operation and maintenance access
- Prepare level concrete foundations as per floor plan
- Lifting equipment may be needed to position heavy parts
- Assemble sections as per supplier instructions
- Install hydraulic, pneumatic, lubrication, and electrical systems
- Connect to power supply and grounding
- Test run the line and make adjustments as needed
Proper installation is key for smooth functioning. Take suppliers’ help or hire experienced mechanical contractors.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग लाइनों का संचालन
- Strictly follow the supplier manual for pre-checks and start-up
- Load coils using overhead crane or forklift
- Thread coil end through decoiler and guides into roll former
- Set forming speed and cut-off length as required
- Adjust guides, rolls, and pressure as needed
- Monitor line operation and finished panels
- Safety protocols are critical – wear PPE, use safety guards
- Schedule periodic maintenance and lubrication
- Ensure sufficient material inventory and trained staffing
- Adjust parameters to change profiles if desired
Trained operators are essential for efficient roll forming operation.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग उपकरण का रखरखाव
| गतिविधि | आवृत्ति |
|---|---|
| रोल की स्थिति का निरीक्षण करें | मासिक |
| Check hydraulic system | 3 महीने |
| बेयरिंग को चिकनाई दें | 3 महीने |
| Verify alignments | 6 महीने |
| Change damaged rolls | आवश्यकतानुसार |
| सेंसरों को कैलिब्रेट करें | वार्षिक |
Preventative maintenance minimizes unplanned downtime and improves performance.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग उपकरण आपूर्तिकर्ता का चयन कैसे करें
| कारक | मानदंड |
|---|---|
| उत्पादन दर | Match to required output volume |
| Panel profiles | Equipment capable of specific designs needed |
| स्वचालन स्तर | Manual, semi or fully automatic |
| परिशुद्धता | Tolerances, repeatability, precision of forming |
| विश्वसनीयता | Reputable brand with proven quality |
| लागत | Budget targets and value for money |
| लीड टाइम | Delivery schedule requirements |
Evaluate suppliers based on both technical specifications and commercial factors.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग के लाभ और हानियाँ
फायदे
- अत्यधिक उत्पादक सतत प्रक्रिया
- Consistent quality panels in long lengths
- Versatile – can produce varied panel profiles
- Lower material waste versus sheet stamping
- Lower investment cost versus extrusions
- Flexible production volumes with quick changeovers
- Automation possible for high-volume needs
- Proven and mature roll forming technology
नुकसान
- Upfront design and tooling cost for new profiles
- Repeating initial set-up for short runs
- Skill needed for specialized machine operation
- Size limitations of roll forming line
- Limited material strength versus extrusions
- Complex double furring shapes can be challenging
डबल फ्यूरिंग सीलिंग पैनल बनाम एक्सट्रूडेड पैनल
| Roll Formed Panels | Extruded Panels | |
|---|---|---|
| लागत | Lower equipment investment | Higher capital costs |
| लचीलापन | Faster changeovers between profiles | सीमित प्रोफाइल आकार |
| मजबूती | Suitable for light to medium duty | Stronger for heavy duty applications |
| थ्रूपुट | Up to 500 m2/hr | Up to 600 m2/hr |
| फिनिश | Secondary painting required | उत्कृष्ट सतह फिनिश |
| Panel size | Limitations on width and height | Unlimited panel dimensions |
Roll forming strikes an optimal balance of cost, flexibility and speed for double furring ceiling panel production.
डबल फ्यूरिंग सीलिंग पैनल स्थापना युक्तियाँ
- Carefully inspect panels before installation for any defects
- Measure ceiling dimensions and cut panels to fit if needed
- Plan the panel layout pattern and sequence
- Lift panels safely using straps around perimeter – do not bend
- Fasten to ceiling frame using self-tapping screws into holes
- Level and align each panel as you go
- Install edge trim and end caps for finished look
- Seal any gaps for enhanced thermal insulation
- Touch up scratches with matching paint if needed
Proper planning, handling and fastening ensure the roll formed panels come out looking great.
अक्सर पूछे जाने वाले प्रश्न
| प्रश्न | उत्तर |
|---|---|
| What types of metal can be roll formed into double furring panels? | Galvanized steel, aluminum, cold rolled steel and pre-painted steel sheets are commonly used. |
| What thickness of coils can be processed? | Typically 0.3 mm to 1 mm thickness sheets are suitable for these panels. |
| How long can the roll formed panels be? | Standard lengths range from 2 to 12 meters. Custom lengths are possible. |
| What safety precautions are important? |
रोल फॉर्मिंग के बारे में अधिक जानें
अक्सर पूछे जाने वाले प्रश्न (FAQ)
1) What line speed can I expect for Double Furring Ceiling Roll Forming Machines with punching?
- Typical 2025 ranges: 10–22 m/min without embossing; 8–16 m/min with inline punching and flying cutoff. Speed depends on metal thickness, hole pitch, and cutoff type.
2) Which coil substrates and coatings perform best for indoor ceilings?
- Galvanized steel (Z140–Z275) and zinc–magnesium (ZM90–120 per EN 10346) for corrosion resistance; pre-painted steel per EN 10169 with polyester or PVDF topcoats for visible spaces; 3003/5052 aluminum for humid or coastal interiors.
3) How do I reduce burrs and deformation around punched holes?
- Use fine-blanking-style punches with minimal die clearance (~6–10% of stock thickness), keep punch/die sharpness within spec, apply stripper springs, and synchronize servo feed to avoid punch drag.
4) What tolerance is realistic on furring height and straightness?
- Best-in-class: furring height ±0.3–0.5 mm; straightness ≤1.5 mm over 3 m. Achieved with precision roll alignment, crowned rolls, and closed-loop length control via encoder/laser.
5) What is the most cost-effective automation upgrade for small shops?
- Servo flying cutoff + recipe-based length control integrated with the punching unit. Typical ROI 9–15 months from scrap reduction (<1.2%), faster changeovers (30–50%), and improved throughput.
2025 उद्योग रुझान
- Shift to all-electric flying cutoff and punching, reducing oil leaks and energy use.
- Inline vision and laser gauging verify hole pitch, strip camber, and furring height in real time.
- Zn–Mg coils adopted for better cut-edge corrosion in HVAC-heavy interiors.
- Quick-change cassettes and digital recipes shorten profile changeover to under 30 minutes.
- OPC UA/MQTT connectivity streams production/QC to MES for traceability on commercial projects.
डबल फ्यूरिंग सीलिंग रोल फॉर्मिंग के लिए 2025 के बेंचमार्क
| KPI (0.35–0.6 mm GI/PPGI) | २०२३ सामान्य | 2025 सर्वश्रेष्ठ-इन-क्लास | प्रमुख सक्षम कारक |
|---|---|---|---|
| पंचिंग के साथ लाइन गति (m/min) | 8–12 | बारह–सोलह | Servo feed, all-electric press |
| लंबाई सहनशीलता (3σ, mm) | ±1.5 | ±0.6–0.9 | High-res encoders, temp comp |
| Hole pitch accuracy (mm) | ±0.8–1.2 | ±0.3–0.5 | विज़न फीडबैक, सर्वो सिंक |
| चेंजओवर समय (min) | 60–120 | 20–35 | Cassette rolls, auto presets |
| स्टार्टअप स्क्रैप (%) | 2.5–4.0 | 0.8–1.5 | डिजिटल रेसिपी, SPC |
| ऊर्जा (kWh/1,000 m) | 50–70 | 32–48 | IE4 मोटर, VFD, स्मार्ट आइडल |
| Zn–Mg coil share (EU interiors) | 8–12% | 18–28% | संक्षारण + स्थिरता |
आधिकारिक स्रोत:
- EN 10346 (निरंतर हॉट-डिप कोटेड स्टील): https://standards.cen.eu
- EN 10169 (organic coated steel): https://standards.cen.eu
- ASTM A653 (GI) and A755/A755M (prepainted): https://www.astm.org
- OPC Foundation (OPC UA): https://opcfoundation.org
- U.S. DOE AMO (मोटर दक्षता): https://www.energy.gov/eere/amo
नवीनतम अनुसंधान मामले
Case Study 1: Vision-Assisted Hole Pitch Control for Double Furring Profiles (2025)
Background: A commercial ceiling supplier faced installation misfits due to variable hole pitch and panel length across multi-shift production.
Solution: Integrated camera-based vision metrology to measure hole pitch and furring height; implemented closed-loop correction to the punching servo and line encoder; added auto thermal compensation.
Results: Hole pitch accuracy improved from ±1.1 mm to ±0.4 mm; length tolerance tightened to ±0.7 mm (3σ); scrap reduced by 58%; average line speed increased 12% with fewer stops.
Case Study 2: All-Electric Cutoff + Zn–Mg Coil Transition in Humid Environments (2024)
Background: Projects in high-humidity interiors reported edge rust on GI double furring channels after 12–18 months.
Solution: Switched from Z275 GI to ZM120 coils (EN 10346); replaced hydraulic flying cutoff with all-electric unit; optimized lube and anti-scuff roll finish.
Results: 1,000 h neutral salt spray edge creep improved by 30–40%; warranty claims decreased 45% YoY; energy per 1,000 m dropped 17%; maintenance downtime fell 3.5%.
विशेषज्ञों की राय
- डॉ. Sofia Marin, वरिष्ठ सामग्री इंजीनियर, European Coil Coaters Association
- “Zinc–magnesium coatings offer superior cut-edge protection for interior ceiling systems, allowing reduced coating mass without sacrificing durability—ideal for double furring channels.”
- Daniel Wu, इंजीनियरिंग निदेशक, Formtek Group
- “All-electric punching and flying cutoff deliver repeatability and faster diagnostics. For ceiling furring, that translates to tighter hole pitch and fewer onsite installation issues.”
- प्रो. Liam O’Connor, प्रमुख, Advanced Forming Research Centre, University of Strathclyde
- “Vision-in-the-loop roll forming is moving from pilot to production, enabling sub-millimetre control on thin-gauge, prepainted stock with minimal paint marring.”
व्यावहारिक उपकरण/संसाधन
- COPRA RF (roll design) and COPRA RF Vision: https://www.datam.de
- UBECO PROFIL (roll form design software): https://www.ubeco.com
- NIST Engineering Statistics Handbook (SPC for inline QC): https://www.itl.nist.gov/div898/handbook
- ASTM A653, A755/A755M standards access: https://www.astm.org
- European Coil Coaters Association की सर्वोत्तम प्रथाएँ: https://www.prepaintedmetal.eu
- OPC Foundation (मशीन डेटा के लिए OPC UA): https://opcfoundation.org
- ऊर्जा अनुकूलन के लिए DOE Motor Systems Tool: https://www.energy.gov/eere/amo
नोट: खरीद या प्रक्रिया में बदलाव से पहले अपने विशिष्ट डबल फ्यूरिंग ज्यामिति, होल पैटर्न, सब्सट्रेट और स्थानीय बिल्डिंग कोड के आधार पर बेंचमार्क का सत्यापन करें।
अंतिम अपडेट: 2025-10-21
परिवर्तन-लेख: 5 FAQs जोड़े गए; KPI तालिका के साथ 2025 के रुझानों का संकलन किया गया; दो हालिया केस स्टडी शामिल की गईं; विशेषज्ञों की राय जोड़ी गई; प्रामाणिक लिंक के साथ व्यावहारिक टूल/संसाधन प्रदान किए गए
अगली समीक्षा तिथि और ट्रिगर: 2026-04-21 या उससे पहले, यदि EN/ASTM मानकों में संशोधन किया जाता है, प्रमुख OEMs पूरी तरह इलेक्ट्रिक पंचिंग/कटऑफ अपग्रेड जारी करते हैं, या Zn–Mg कॉइल अपनाने के दिशानिर्देश बदलते हैं





