
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

मेटल रूफ रिज कैप रोल फॉर्मिंग मशीन provide decorative finishing touches protecting critical roofing joints. This guide covers various metal ridge cap profile types, working principles of roll forming lines producing them, key machmetal roof ridge cap roll forming machineine components, installation guidelines, maintenance factors, leading global manufacturers, and typical end-use case comparisons.
रोल फॉर्मर्स द्वारा उत्पादित सामान्य रिज कैप प्रोफाइल
| प्रोफ़ाइल प्रकार | प्रमुख विशेषताएँ | सामान्य सामग्री |
|---|---|---|
| Angular ridge caps | Triangle cross-section | Painted steel, zinc |
| Flatlock ridge caps | Overlapping flat pan | एल्यूमिनियम |
| Beaded ridge caps | Rounded ornamental bead | तांबा |
| Venting ridge caps | Perforations for ventilation | गैल्वनाइज्ड स्टील |
| Bullnose ridge caps | Convex curved shape | स्टेनलेस स्टील |
Roll formed ridge caps protect vulnerable roofing joints from weather stresses aesthetically. Fit with panels.
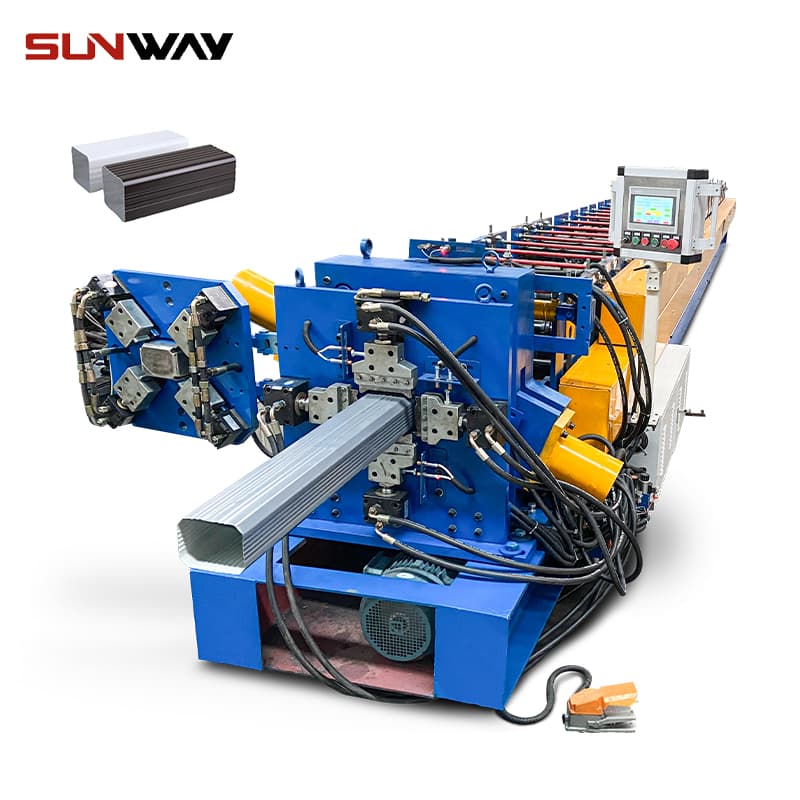
कार्य सिद्धांत मेटल रूफ रिज कैप रोल फॉर्मिंग मशीन
Continuous forming from coil stock into ridge cap profiles uses a series of bending and shaping roller dies operating in matched male-female pairs. Main aspects:
- Programmable tooling molds specific geometries
- Strategic positioning for metal grain flow
- स्वचालित किनारा मार्गदर्शन और गेजिंग
- Supporting decoilers and straighteners
- Flying shear length cutoff control
- Exit tables, automated packing
Fully formed cap sections exit at the designed lengths continuously when feeds optimized.
मेटल रूफ रिज कैप रोल फॉर्मिंग मशीन के प्रमुख घटक
| घटक | भूमिका |
|---|---|
| डिकॉयलर | Feeds raw metal coil stock |
| प्रवेश गाइड | Aligns strip before dies |
| फॉर्मिंग स्टेशन | Each imparts profile incrementally |
| नियंत्रण कैबिनेट | Manages production logic |
| हाइड्रॉलिक यूनिट | Powers die actuation |
| फ्लाइंग कटऑफ | Trims caps to length |
| निकास कन्वेयर | Transfers finished caps out |
Standardized modular designs allow changing machine widths easily.
-
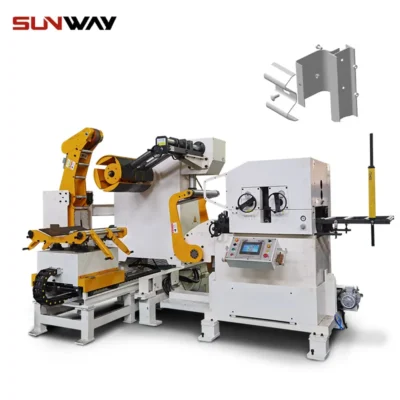 हाईवे गार्डरेल एंड टर्मिनल फॉर्मिंग मशीन अधिक पढ़ें
-
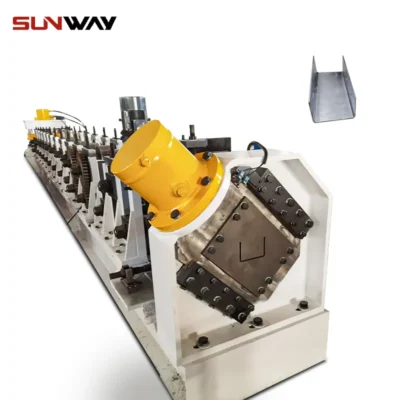 हाईवे U/C पोस्ट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
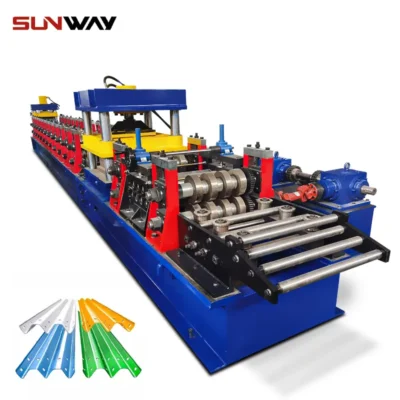 2 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
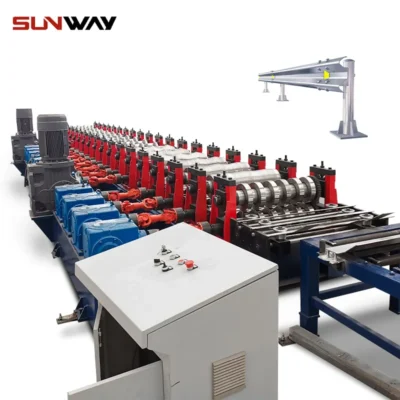 3 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
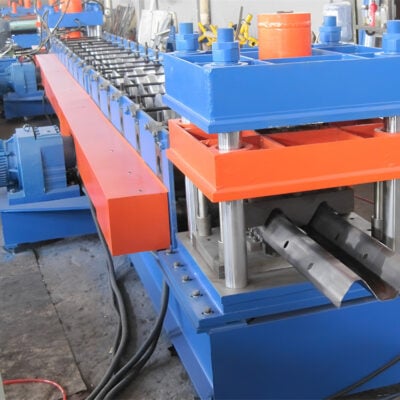 दो वेव हाईवे गार्डरेल मशीन अधिक पढ़ें
-
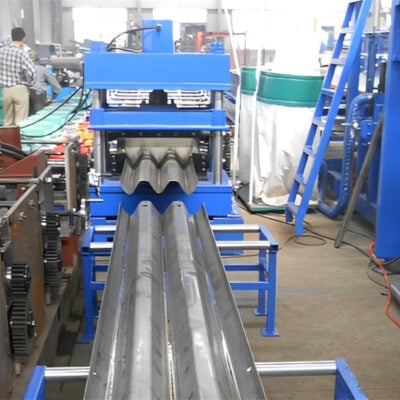 तीन वेव हाईवे गार्डरेल मशीन अधिक पढ़ें
-
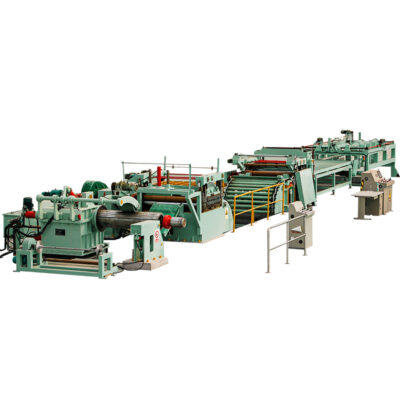 स्टील कॉइल कट टू लेंथ लाइन मशीन अधिक पढ़ें
-
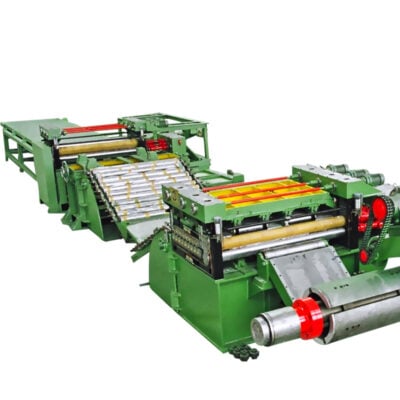 स्टील कॉइल कट टू लेंथ लाइन मशीन अधिक पढ़ें
-
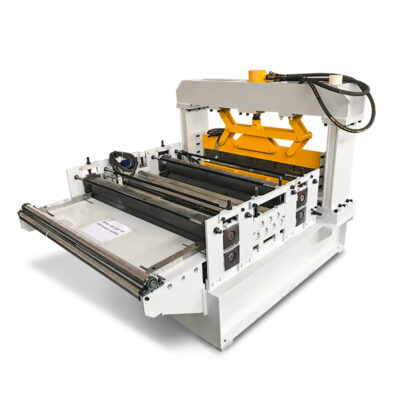 स्टील कॉइल कट टू लेंथ लाइन मशीन अधिक पढ़ें
स्थापना दिशानिर्देश
| गतिविधि | प्रक्रिया |
|---|---|
| स्थिति निर्धारण | Level concrete base |
| लेआउट | Rear access considered |
| कनेक्शन | पावर ड्रॉप, कंड्यूट |
| Initial run | Confirm clearances, flows |
| प्रोग्रामिंग | Template recipes for profiles |
| कमीशनिंग | Validate with test materials first |
Utilize factory technician support during initial configuration to streamline debugging and maximize runtime productivity faster.
संचालन और रखरखाव कारक
| समय-सारणी | कार्य |
|---|---|
| दैनिक | रोलर के स्नेहन की पुष्टि करें |
| साप्ताहिक | Inspect/tension drive chains |
| मासिक | हाइड्रॉलिक रिसाव की जाँच करें |
| त्रैमासिक | Inspect control wiring |
| वार्षिक | बेयरिंग प्रतिस्थापन |
Keep records of length inspection data, downtime causes and electrical faults to prioritize improvements increasing overall equipment effectiveness.
रिज कैप रोल फॉर्मिंग मशीनें खरीदते समय विचार
| कारक | मूल्यांकन मानदंड |
|---|---|
| उत्पादन दर | प्रति घंटे लीनियर फीट की दर |
| सामग्री के प्रकार | Steel, aluminum etc |
| प्रोफाइल रेंज | Variants required |
| सटीकता | Twist, bow, length variation |
| स्वचालन स्तर | मैनुअल संचालन की मात्रा |
| रनटाइम की गारंटी | विफलताओं के बीच औसत समय |
| डिलीवरी की शर्तें | इंस्टॉलेशन कार्यक्रम |
| प्रशिक्षण | ऑपरेटर परिचय का दायरा |
Request machine tolerance capabilities report from vendors during selection process.
प्रमुख रिज कैप रोल फॉर्मर निर्माताओं का तुलनात्मक विश्लेषण
| कंपनी | सटीकता | लीड टाइम | लागत |
|---|---|---|---|
| Metform | बहुत अच्छा | 10 सप्ताह | मध्यम |
| EWMenn | अच्छा | 12 सप्ताह | कम |
| Rollmac | उत्कृष्ट | 14 सप्ताह | अधिक |
| Gasparini SpA | बहुत अच्छा | 16 सप्ताह | अधिक |
| botou Xianfa | अच्छा | 8 सप्ताह | कम |
लाभ और सीमाएँ
| फायदे | नुकसान |
|---|---|
| त्वरित बड़े पैमाने पर उत्पादन | उच्च प्रारंभिक टूलिंग लागत |
| कम परिचालन लागत | Skilled technician requirment |
| Consistent end quality | Heavier gauge capability limited |
| Range of integration | बड़ा उत्पादन क्षेत्र |
| Cost efficiency at utilization | Significant foundations needed |
Calculate total cost savings from accelerated roofing project timelines against higher equipment investment when planning capacity.
अक्सर पूछे जाने वाले प्रश्न
What thickness range can these machines handle?
Most standard lines efficiently process 0.4 mm to 0.7 mm metallic sheets for ridge caps. Thicker specialty materials require heavier presses and custom roller sets.
What determines maximum line speed?
Motor drive power ratings, press tonnage capabilities, decoiler payload and rates of downstream handling systems govern production tempo. Vendor proposal should provide speed calculations.
How quick are changeovers between profiles?
1-2 days is typical for experienced technicians to switch dedicated ridge profile roller sets handling similar substrate widths. Modular designs speed changeovers.
What degree of length precision held?
Precision servo powered cutoffs with rigid framing achieve under 2 mm length tolerance capability for quality lines even at peak speeds.
How to select suitable lubricants?
Consult lubricant vendor to match fluids, oils and greases to operating pressures, velocities, material specs, temperatures and ambient conditions to maximize machine lifespan while preventing contamination.
निष्कर्ष
In summary, specialized ridge cap roll formers deliver productive roofing accessory manufacturing combining operational cost efficiencies vital for regional building products supply security. Careful evaluation of purchase costs against revenue projections from resultant sales funnel ROI potentials assists strategic capacity investments.





