
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

मैनुअल रोल फॉर्मिंग मशीन is a continuous bending process used to form metal sheet and coils into custom profiles. Manual roll formers are simple machines operated by hand to produce small batches or custom parts.
मैनुअल रोल फॉर्मर उपकरण मार्गदर्शिका
| उपकरण | विवरण |
|---|---|
| फॉर्मिंग रोल्स | हाउसिंग में लगे समोच्च रोल |
| रोल समायोजन | Manual screws to set roll gap |
| फीड टेबल | Flat table to support material |
| Hand crank | Rotates forming rolls |
| गाइड प्लेटें | Metal strips to guide material |
- Manual rollers use hand-adjusted forming rolls
- Material is fed through by turning hand crank
- Guide plates align strip through rolls
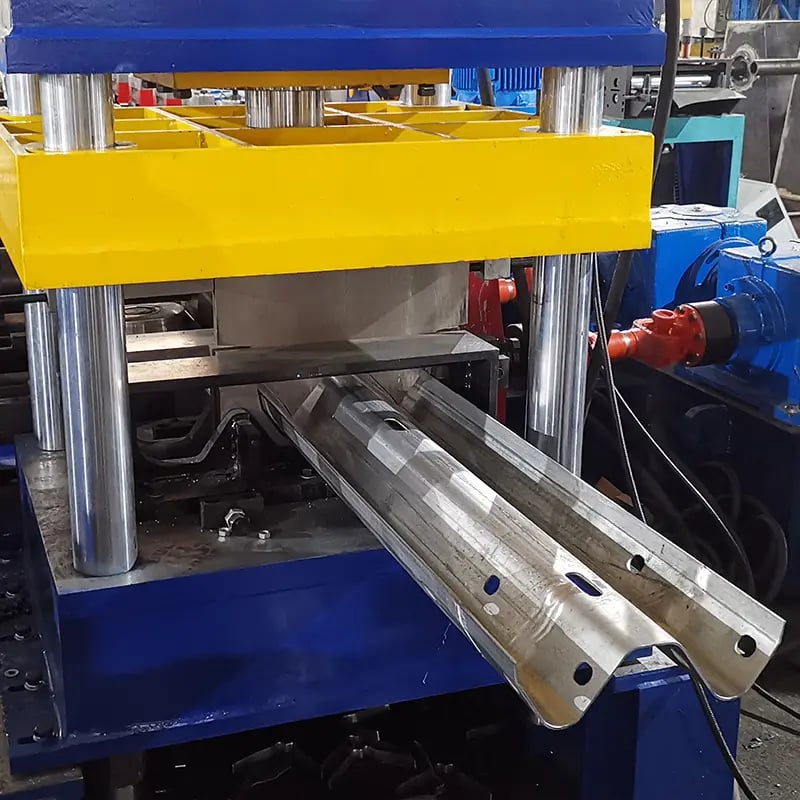
मैनुअल रोल फॉर्मिंग की कार्य प्रक्रिया
The process starts by positioning the flattened strip on the feed table and inserting the leading edge into the roll gap. The hand crank is then turned continuously to rotate the rolls. As the strip passes between the contoured rolls, it begins to take the shape of the roll profiles. Once fully formed, the strip can be cut to the desired length by shears.
मैनुअल रोल फॉर्मर में सामग्री फीडिंग
| विधि | विवरण |
|---|---|
| फीड टेबल | Flat table to support coils/sheets |
| गाइड प्लेटें | Attach to table to keep alignment |
| Hand feeding | Operator feeds strip through rolls |
| सपोर्ट रोलर | Reduce friction when feeding |
- Feed table supports the material
- Guide plates keep strip alignment
- Operator manually feeds the strip
- Support rollers ease material flow
मैनुअल रोल बेंडर में प्रोफ़ाइल फॉर्मिंग
| विधि | विवरण |
|---|---|
| फॉर्मिंग रोल्स | हाउसिंग में लगे समोच्च रोल |
| रोल सामग्री | विभिन्न स्टील मिश्रधातुएँ |
| रोल समायोजन | Set roll gap spacing |
| नियंत्रण | Hand crank for rotating rolls |
- Forming done by hardened steel rolls
- Rolls machined to required profiles
- Roll gap spacing is hand adjusted
- Hand crank control to turn rolls
मैनुअल रोल फॉर्मर से बनने वाली सामान्य प्रोफ़ाइल
| Shape | विवरण |
|---|---|
| एंगल | L shaped profiles |
| चैनल | U shaped profiles |
| Round tubes | Hollow circular tubes |
| Square tubes | Hollow square tubes |
| कस्टम | विशिष्ट आकार |
- Angle, channel and tube profiles commonly produced
- Capability for custom shapes as needed
- Usually simpler profiles due to process limits
-
 स्टैंडिंग सीम रूफ पैनल कर्विंग मशीन अधिक पढ़ें
-
 बैरल कोरुगेटेड रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 स्टैंड सीमिंग रूफ पैनल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
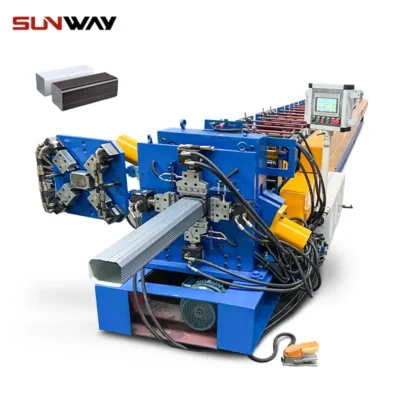 डाउनस्पाउट पाइप रोल फॉर्मिंग मशीन अधिक पढ़ें
-
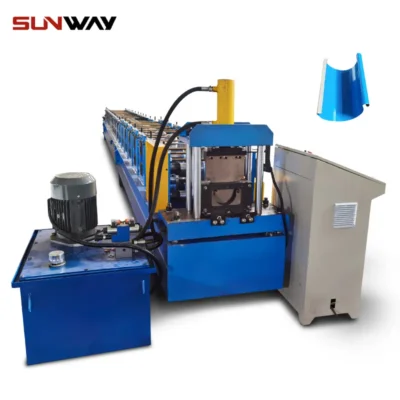 गटर रोल फॉर्मिंग मशीन अधिक पढ़ें
-
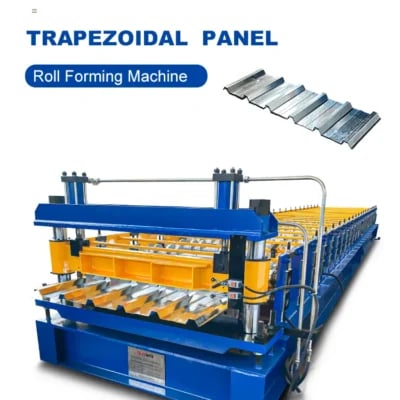 ट्रेपेज़ॉइडल पैनल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
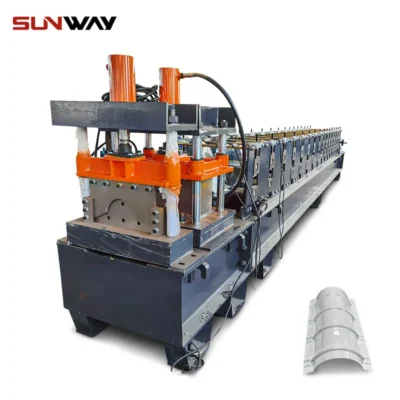 रिज कैप रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 डबल लेयर पैनल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 रूफ टाइल पैनल रोल फॉर्मिंग मशीन अधिक पढ़ें
मैनुअल रोल फॉर्मर के लिए कटऑफ़ विधि
| विधि | विवरण |
|---|---|
| Shear | Hand operated shear |
| Saw | Portable saw |
| सपोर्ट टेबल | Tables to collect cut parts |
- Cutoff done manually via shear or saw
- Tables to safely collect cut pieces
मैनुअल रोल बेंडर में अनुकूलन विकल्प
| विकल्प | विवरण |
|---|---|
| Custom rolls | Profile specific rolls |
| त्वरित परिवर्तन | Roll changes without reassembly |
| Size adjustment | Spacers for roll adjustment |
| Tooling kits | Special forming accessories |
- Custom roll sets for unique profiles
- Quick roll changes possible with clamp housings
- Spacers inserted to adjust sizing
- Tooling kits offered for specialty forming
के आपूर्तिकर्ता मैनुअल रोल फॉर्मिंग मशीनें
| निर्माता | स्थान | मूल्य सीमा |
|---|---|---|
| Acro Metal Stamping | कनाडा | $3k – $7k |
| Carell Corp | USA | $5k – $15k |
| Durma | तुर्की | $3k – $10k |
| Gasparini | इटली | $10k – $30k |
| Sahinler Roll Forming | तुर्की | $4k – $12k |
- Many manual roll bender models available
- Prices range from a few thousand to tens of thousands
- Quality varies greatly, durability is key factor
स्थापना और संचालन
| गतिविधि | विवरण |
|---|---|
| स्थिति निर्धारण | Accessible location for operation |
| लेवलिंग | Use shims to level feed tables |
| परीक्षण संचालन | Confirm forming with sample material |
| संचालन | Control direction and feed rate |
| सुरक्षा | Follow guards, precautions |
- Position for ease of loading/unloading
- Levelness is critical for proper feeding
- Test runs validate forming process
- Controlled hand feeding minimizes issues
- Strict safety protocols are essential
मैनुअल रोल बेंडर का रखरखाव
| विधि | विवरण | आवृत्ति |
|---|---|---|
| सफाई | Remove dirt, metal chips | दैनिक |
| स्नेहन | Apply oil to gears, bearings | मासिक |
| निरीक्षण | Check roll surface, alignment | त्रैमासिक |
| रोल परिवर्तन | घिसे हुए रोल बदलें | आवश्यकतानुसार |
| ओवरहॉल | Major repairs | If breakdown |
- धातु के महीन कणों की नियमित सफाई
- Lubrication reduces wear and noise
- Inspection catches issues early
- Roll sets replaced when excessively worn
- Overhauls done if major failure occurs
मैनुअल रोल फॉर्मर आपूर्तिकर्ता का चयन
| कारक | विवरण |
|---|---|
| मूल्य | Upfront cost more important than operating cost |
| लीड टाइम | Quick delivery enables fast setup |
| अनुभव | Know-how with specialty profiles preferred |
| अनुकूलन | Ease of producing custom tooling |
| सहायता | Install guidance and operator training useful |
| Manuals | Clear instructions on operation, safety |
| मानक | Meets applicable quality and safety codes |
- Seek balance of price versus longevity
- Quick delivery is advantageous
- Custom roll capability essential
- Look for responsive technical support
- Clear manuals reduce learning curve
- Reputable firms meet regulatory standards
मैनुअल रोल बेंडर के लाभ और हानियाँ
लाभ
- Very economical for low volume production
- Fast design iteration with rapid tooling changes
- Allows small batch custom profiles
- Flexible setup for different product sizes
- Low power consumption versus motorized equipment
- Compact size fits production environments with space constraints
- Simplified design gives high uptime and availability
सीमाएं
- Labor intensive manual operation
- Inconsistent throughput dependent on operator skill
- Heightened safety hazards from hand feeding
- Limits on part size and forming complexity
- Repeated handling can reduce end quality
- Not practical for high volume production needs
मैनुअल रोल बेंडर के अनुप्रयोग
विशिष्ट अनुप्रयोगों में शामिल हैं:
- Custom electrical enclosures
- Specialty HVAC ductwork
- Low quantity metal furniture parts
- Short run metal artwork frames
- Custom architectural facade elements
- Unique ornamental iron components
- Small specialty automotive accessories
- Experimental and rapid prototype sections
Common materials formed are steel, aluminum, copper, and brass in gauges from 0.5 mm to 3 mm thickness.
अक्सर पूछे जाने वाले प्रश्न
मैनुअल रोल बेंडर पर कौन-सी प्रोफ़ाइल बनाई जा सकती हैं?
Common shapes are angles, channels, square/rectangular tubes, round tubes and cones. Custom profiles are possible but complexity is limited by the manual process.
किस मोटाई की धातुओं को मैन्युअल रूप से बनाया जा सकता है?
Standard models typically form material from 0.5 mm to 3 mm thickness. Extended ranges available on some heavy duty models.
मैनुअल रोलिंग प्रक्रियाओं से बनाई गई प्रोफ़ाइल कितनी सटीक होती हैं?
Precision is heavily dependent on operator skill, but properly leveled machines with adequate guides can achieve tolerances around +/- 0.5 mm.
मैनुअल रोल बेंडर चलाने के लिए कितनी शक्ति आवश्यक है?
No external power source is required. The hand crank mechanism provides the motive force to drive the forming rolls.
मैनुअल रोलिंग की उत्पादन दर किससे निर्धारित होती है?
Throughput is limited by the speed the operator can safely feed the material through the rollers, typically less than 10 feet per minute.
मैनुअल रोल संचालन के लिए महत्वपूर्ण सुरक्षा दिशानिर्देश क्या हैं?
Guards around rolls, guide plates to avoid pinching, gloves to protect hands, strict one operator policy, and emergency stops are critical to safety.
इन मशीनों की गुणवत्ता और आयु को प्रभावित करने वाला सबसे बड़ा कारक क्या है?
The quality of the roll bearings is often the main determinant of lifespan, performance, and durability under prolonged use.
विशेष प्रोफ़ाइल के लिए प्रतिस्थापन कस्टम रोल सेट की लागत कितनी होती है?
Roll sets can range from $500 for common shapes to $5000 or more for complex custom shapes requiring specialized machining.
क्या मैनुअल रोल बेंडर छोटे पैमाने के वाणिज्यिक उत्पादन के लिए उपयुक्त हैं?
They can be appropriate for limited commercial work depending on volumes. Automated machines are preferred for scale production.
रोल फॉर्मिंग के बारे में अधिक जानें
अक्सर पूछे जाने वाले प्रश्न (FAQ)
1) Are manual roll forming machines suitable for stainless steel or only mild steel?
- Most manual roll formers can handle mild steel and aluminum; 304/316 stainless is possible at thinner gauges (≤1.0–1.5 mm) with polished, hardened rolls and liberal lubrication to reduce galling.
2) How can I improve repeatability on a hand-cranked roll former?
- Level the base, use fixed gauge stops, mark handwheel positions for known sizes, keep consistent feed rate, and perform a 3-piece first-article check (start/mid/end) to fine-tune roll gaps.
3) What is the practical maximum section height for manual forming?
- For light-gauge sections, 40–60 mm leg/flange height is common. Taller sections often require pre-notching/hemming or powered assists to avoid twist and oil-canning.
4) Can manual roll benders form pre-painted coils without damaging the coating?
- Yes, with smooth, radiused rolls, proper roll gap, protective films, and dry-film or compatible low-VOC lubricant. Conduct a tape test after forming to verify coating adhesion.
5) When should I step up from manual to powered roll forming?
- Triggers include volume >200–300 m/day, thickness >2.0–2.5 mm regularly, frequent size changes requiring tight tolerances, or safety/ergonomic strain on operators.
मैनुअल रोल फॉर्मिंग मशीनों के लिए 2025 उद्योग रुझान
- Hybrid assist kits: Add-on gear reduction and compact servo drives provide “power assist” while retaining manual control for delicate sections.
- Quick-change cartridges: Low-cost cartridge roll sets enable sub-10-minute profile swaps for makerspaces and job shops.
- Metrology on a budget: Portable laser length gauges and smartphone-based angle/profile checkers improve QA without full automation.
- Low-VOC lubricants: Shops adopt biodegradable, low-odor forming fluids for indoor manual forming and better cleanup.
- Safety ergonomics: Crank torque limiters, pinch-point shields, and one-hand feed guides reduce strain and pinch risks.
2025 बेंचमार्क और डेटा स्नैपशॉट
| KPI (manual roll forming) | २०२३ सामान्य | 2025 सर्वश्रेष्ठ-इन-क्लास | व्यावहारिक प्रभाव | स्रोत |
|---|---|---|---|---|
| Setup/changeover time | 20–40 मिनट | 8–15 min (cartridge rolls) | More small-batch agility | The Fabricator; OEM brochures |
| Achievable tolerance (± mm) | 0.7–1.0 over 2 m | 0.4–0.6 with gauges/fixtures | कम पुनःकार्य | SME; शॉप QA रिपोर्ट |
| Throughput (m/min) | 1–2 | 2–4 with power-assist | अधिक दैनिक उत्पादन | Industry case notes |
| Max typical thickness (mm) | 2.0–2.5 MS | 3.0 with hardened rolls | Wider material range | ASTM practices; OEM data |
| Lubricant VOC (g/L) | 100–300 | <50 (low-VOC/biodegradable) | Better indoor compliance | EPA guidance; supplier SDS |
प्रामाणिक संदर्भ:
- ASTM A1008/A1011 sheet steels: https://www.astm.org
- The Fabricator (manual/roll forming): https://www.thefabricator.com
- SME विनिर्माण ज्ञान: https://www.sme.org
- U.S. EPA VOC guidance (industrial lubricants): https://www.epa.gov
- NIOSH/OSHA machine guarding and ergonomics: https://www.osha.gov
नवीनतम अनुसंधान मामले
Case Study 1: Quick-Change Manual Roll Former for Architectural Prototypes (2025)
- Background: A façade studio needed short-run, color-matched aluminum channels with frequent geometry tweaks during client reviews.
- Solution: Deployed a manual roll forming machine with cartridge roll sets, smartphone angle gauges, and low-VOC lubricant; implemented first-article 3-piece QA.
- Results: Changeover time cut from 28 to 11 minutes; scrap reduced from 6.1% to 2.2%; visual coating defects decreased by 40%; maintained ±0.6 mm over 2 m lengths.
Case Study 2: Power-Assist Retrofit for Makerspace Education (2024)
- Background: University makerspace struggled with operator fatigue and inconsistent feed rates forming 1.5 mm steel channels.
- Solution: Added compact servo-assist to the crank shaft with adjustable torque limiter and upgraded pinch-point guards; standardized setup sheets and torque marks.
- Results: Average throughput doubled from 1.5 to 3.1 m/min; tolerance improved from ±0.9 mm to ±0.5 mm; operator strain complaints dropped 70% per semester incident logs.
विशेषज्ञों की राय
- Dr. James S. Moen, PE, Lecturer, Cold-Formed Steel Design (University of Minnesota)
- Viewpoint: “Manual roll forming benefits most from fixture discipline—simple gauge blocks and consistent bend progression can rival entry-level powered lines for short runs.”
- स्रोत: https://cce.umn.edu
- Kate Bachman, वरिष्ठ संपादक, The Fabricator
- Viewpoint: “Quick-change roll cartridges are the game changer for job shops—downtime, not forming speed, is the hidden cost in manual roll forming.”
- स्रोत: https://www.thefabricator.com
- David W. Pons, Safety Consultant, OSHA Outreach Trainer
- Viewpoint: “Torque limiters and fixed guards on hand-crank shafts significantly cut pinch and overexertion injuries in manual forming environments.”
- स्रोत: https://www.osha.gov
व्यावहारिक उपकरण/संसाधन
- Profile design software: UBECO PROFIL https://www.ubeco.com; COPRA RF (data M) https://www.datam.de/en/copra
- Tolerance/QA aids: Portable laser length gauges (Keyence/LaserLinc); smartphone angle apps (Clinometer) for quick checks
- Standards and guidance: ASTM A1008/A1011 sheet steel https://www.astm.org; AISI S100 cold-formed design overview https://www.cfsei.org
- Safety and ergonomics: OSHA Machine Guarding eTool https://www.osha.gov; NIOSH Lifting/Ergonomics resources https://www.cdc.gov/niosh
- Lubricants and cleaners: Low-VOC forming fluids from major suppliers; review SDS and EPA guidance https://www.epa.gov
- Industry insights and tutorials: The Fabricator roll forming channel https://www.thefabricator.com
अंतिम अपडेट: 2025-10-27
परिवर्तन-लेख: Added 5 targeted FAQs; introduced 2025 trends with KPI table and sources; included two recent manual roll forming case studies; compiled expert viewpoints; curated practical tools/resources with standards and safety links
अगली समीक्षा तिथि और ट्रिगर: 2026-04-30 or earlier if setup time >20 min, tolerance worse than ±0.8 mm over 2 m, operator injury/strain incidents increase, or throughput <2 m/min on 1.0–1.5 mm steel jobs





