
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

अवलोकन
Roll forming is an efficient, continuous process for forming light steel sections like studs, battens, roofing, decking, panels and other profiles from coiled sheet. Automated light steel roll forming lines provide high productivity and precision in producing structural framing members and architectural cladding products.
This guide covers the working principles, main components, configurations, specifications, manufacturers, costs, installation, operation and maintenance for modern light steel roll forming equipment. Helpful comparison tables summarize technical details to assist buyers in selecting the right roll former.
Investing in automated light steel roll forming systems allows manufacturers to boost speed, quality consistency and labor productivity. By understanding the technical factors involved, producers can choose equipment matched to their output needs.
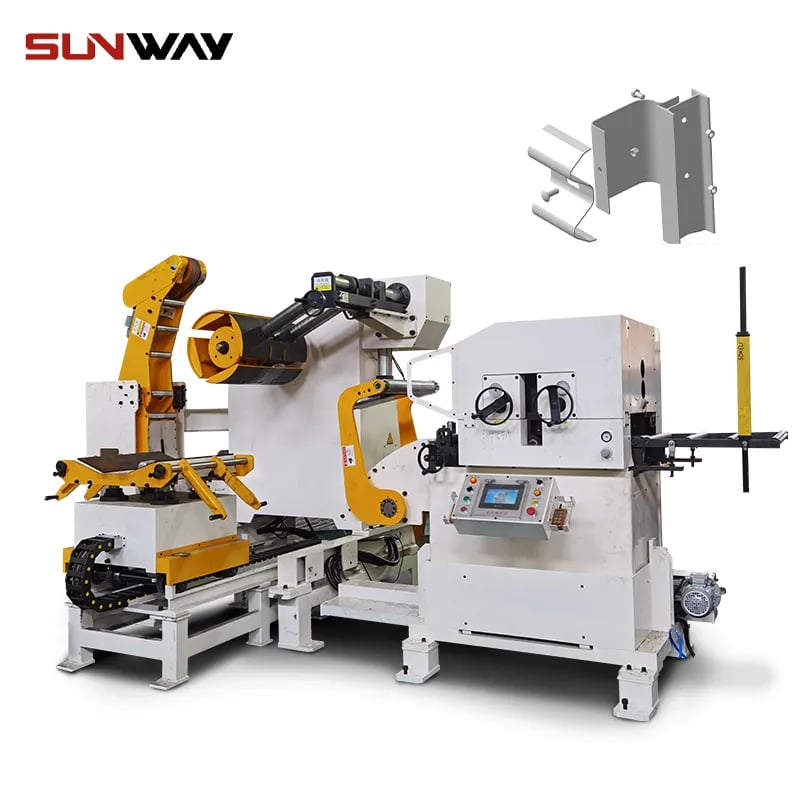
लाइट स्टील रोल फॉर्मर मशीन के प्रकार
Roll formers for light steel products are available in several standard configurations:
लाइट स्टील रोल फॉर्मर मशीन के प्रकार
| मशीन प्रकार | विवरण | सामान्य आउटपुट | मुख्य घटक |
|---|---|---|---|
| Inline roll former | Stations arranged in a straight line | Up to 16 pieces/min | Uncoiler, punch, rolls, cutoff |
| ऑर्बिटल रोल फॉर्मर | Forming stands positioned in an oval | Up to 10 pieces/min | Uncoiler, rolls, cutoff, exit conveyor |
| Shuttle roll former | Shuttles feed sheet incrementally | Up to 20 pieces/min | Uncoiler, shuttle, rolls, cutoff |
| Wheel roll former | Rolls mounted on rotating wheel | Up to 5 pieces/min | Coil carousel, wheel with rolls, cutoff |
Higher production speeds possible with custom machine design and multistation capabilities.
कार्य सिद्धांत
Roll formers shape flat steel strip into structural sections by incrementally bending the material through a series of stations:
लाइट स्टील रोल फॉर्मिंग प्रक्रिया के चरण
- अनकॉइलिंग – Sheet coil is unwound and entered into the line
- फीडिंग – Powered rolls advance the strip
- पंचिंग – Holes punched if needed
- फॉर्मिंग -Contour rolls progressively shape the profile
- कटिंग – Formed section cutoff to length by shear
- निकास – Conveyor collects finished parts
Precise servo electric actuation coordinates the material feed, punching and cutoff motions.
मशीन के प्रमुख घटक
Common components of light steel roll forming lines include:
के मुख्य घटक लाइट स्टील रोल फॉर्मिंग मशीनें
- डीकॉइलर या अनकॉइलर
- Feed tables with pinch rollers
- Punching die stations (optional)
- Forming roll stands
- Rotary or guillotine cutoff shear
- Exit tables and part stackers
- PLC control system and HMI
- सुरक्षा गार्डिंग और बाड़ लगाना
Machines are designed for high duty cycle operation during large volume production runs.
फॉर्मिंग क्षमताएँ
Typical light steel profiles produced on roll forming equipment:
रोल फॉर्मिंग लाइनों पर बनाए जाने वाले लाइट स्टील प्रोफाइल
- Stud wall framing members
- मेटल रूफिंग पैनल
- Wall girts and roof purlins
- Floor joists and rafters
- Drywall track and studs
- Architectural fascia and cladding
- सोलर पैनल फ्रेम
- Storm shelters and safe rooms
- Agricultural building parts
Interchangeable roll sets allow producing different structural sections by changing tooling.
रोल स्टेशनों का विन्यास
Careful roll design and positioning are required to achieve the desired profile:
रोल फॉर्मिंग लाइन विन्यास के कारक
- Number of progressive bending stations
- Bend angle and location at each station
- Material type, thickness and hardness
- Controlling material springback
- Positioning of punching stations
- Rolls precision ground to specifications
- Roll densification and sizing
- Lubrication of rolls and strip
The force applied by each roll must be balanced across stands. Complex programming coordinates the sequential timing.
अनुकूलन विकल्प
Light steel roll formers can be customized via:
लाइट स्टील रोल फॉर्मिंग लाइनों के लिए अनुकूलन विकल्प
- Infeed and exit conveyor lengths and designs
- Single or dual payoff reel configurations
- Additional punching or hole piercing stations
- Quick roll change capability
- सुरक्षा गार्डिंग और बाड़ लगाना
- Communication interfaces and data logging
- Powered section shears and bundlers
- Custom section designs and tooling
- Integration with downstream operations
Experienced suppliers can provide optimized solutions tailored for specific production scenarios.
-
 हाईवे गार्डरेल एंड टर्मिनल फॉर्मिंग मशीन अधिक पढ़ें
-
 हाईवे U/C पोस्ट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 2 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
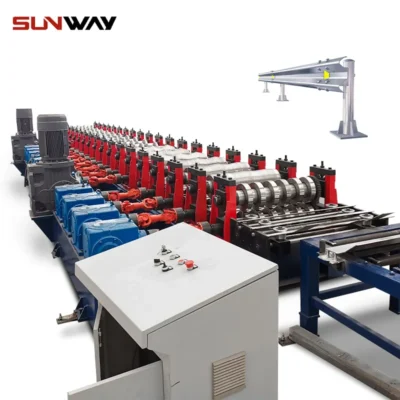 3 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
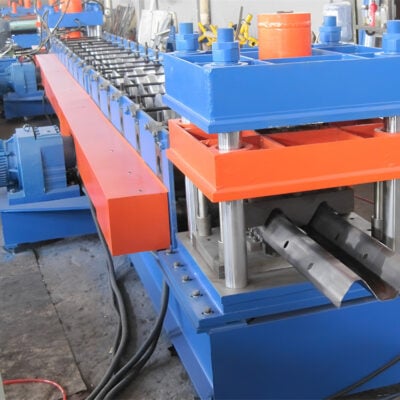 दो वेव हाईवे गार्डरेल मशीन अधिक पढ़ें
-
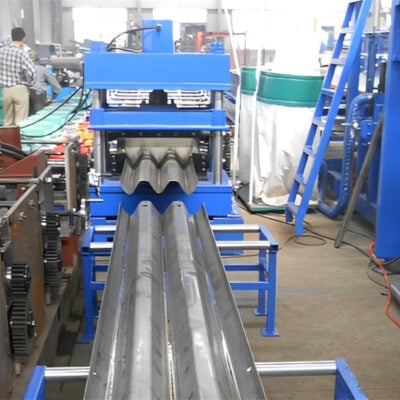 तीन वेव हाईवे गार्डरेल मशीन अधिक पढ़ें
लाइट स्टील रोल फॉर्मर के विनिर्देश
Typical technical specifications for लाइट स्टील रोल फॉर्मिंग मशीनें:
लाइट स्टील रोल फॉर्मर मशीन के विनिर्देश
| पैरामीटर | सामान्य सीमा |
|---|---|
| फॉर्मिंग गति | 16 – 65 ft/min |
| ड्राइव पावर | 3 – 7.5 HP |
| सामग्री की मोटाई | 26 – 16 gauge (0.5 – 1.5 mm) |
| सामग्री का प्रकार | Low carbon steel, stainless steel, aluminum |
| चौड़ाई क्षमता | 1.5 – 14 inches |
| लंबाई क्षमता | 10 – 40 feet |
| PLC नियंत्रण | Allen-Bradley, Siemens, Mitsubishi |
| वजन | 1500 – 8000 lbs |
Specifications depend on production volumes, material sizes, options and line configuration.
लाइट स्टील रोल फॉर्मर निर्माता
Leading global suppliers of light steel roll forming equipment include:
लाइट स्टील रोल फॉर्मर निर्माता
| कंपनी | स्थान | उपकरण के प्रकार |
|---|---|---|
| फॉर्म प्रक्रिया इंजीनियरिंग | USA | Specialists in light steel roll formers |
| Metform | अंतरराष्ट्रीय | Complete roll forming lines |
| Formtek | USA | Precision light steel roll formers |
| Gensco Equipment | USA | Light duty roofing, flooring and wall panel lines |
| DahChyang Machinery | ताइवान | Value engineered roll forming |
| Rollvis | फ्रांस | Roofing panel lines and cutoff saws |
Look for extensive roll forming experience with light steel when selecting suppliers. Evaluate production speeds, flexibility, and robustness.
लाइट स्टील रोल फॉर्मर की लागत
Turnkey automated light steel roll former system costs range:
लाइट स्टील रोल फॉर्मर की मूल्य सीमाएँ
| मशीन प्रकार | सामान्य मूल्य सीमा |
|---|---|
| Light-duty infeed roll former | $50,000 – $150,000 |
| Medium-duty exit roll former | $80,000 – $200,00 |
| Heavy-duty cutoff roll former | $120,000 – $350,000 |
| High-speed cutoff roll former | $200,000 – $500,000 |
Pricing depends on speed, power, material width, and features. Quotes from several suppliers are recommended.
रोल फॉर्मिंग मशीन स्थापना
Proper foundations, space, and utility connections are required:
लाइट स्टील रोल फॉर्मर की इंस्टॉलेशन आवश्यकताएँ
- Reinforced concrete flooring with good drainage
- 3 phase electrical supply and 480V connection
- Compressed air line with filtration
- Enough linear space for machine plus infeed and exit tables
- Material loading capability – overhead crane or coil lift
- Ceiling height for coil loading and conveyors
- सामग्री के स्थिर गुणों के लिए जलवायु नियंत्रण
Work closely with your supplier to prepare the installation site and connections.
लाइट स्टील रोल फॉर्मरों का रखरखाव
Consistent maintenance maximizes production uptime:
लाइट स्टील रोल फॉर्मर के रखरखाव की सर्वोत्तम प्रथाएँ
- Daily cleaning of rollers and material path
- Lubricating bearings, chains, guides and moving parts
- Monitoring belt tension and hydraulic pressures
- Inspecting controls, wiring and connections
- Verifying roll alignment and adjustment
- Following recommended preventative maintenance schedule
- Promptly replacing any damaged or worn components
- Keeping spare parts inventory on hand
Thorough training of personnel on proper operation, safety, cleaning and maintenance is critical.
लाइट स्टील रोल फॉर्मर खरीदने संबंधी विचार
Key factors to consider when purchasing roll formers:
- Annual production volume targets by product
- Variety of structural profiles to be produced
- Material specifications like thickness, width and grade
- Standard vs custom profile requirements
- Line speed and feed rate needs
- Operator skill level and maintenance expertise
- उपलब्ध स्थापना स्थान और लेआउट
- Total budget expectations and ROI goals
- Options for future expansions or modifications
Getting expert input from an experienced supplier simplifies the equipment selection process.
लाइट स्टील रोल फॉर्मिंग मशीनों के लाभ
स्वचालित लाइट स्टील रोल फॉर्मरों के लाभ
- High production speeds and consistency
- Ability to run lights out with minimal supervision
- Handles a range of structural section geometries
- मैनुअल निर्माण की तुलना में कम श्रम
- Adaptable to future profile design changes
- Lower material waste versus other bending methods
- Scales easily from pilot to full production
Automated roll forming standardizes output quality and reduces costs.
की सीमाएँ लाइट स्टील रोल फॉर्मिंग मशीनें
स्वचालित लाइट स्टील रोल फॉर्मरों की सीमाएँ
- Large initial capital expenditure required
- Permanent factory floorspace footprint
- Single purpose equipment with limited material/profile flexibility
- Skilled maintenance and operation required
- Potential bottlenecks around cutoff and secondary operations
- Significant changeover time between different profiles
- Long lead times for engineering and build
- Hard tooling modifications needed for design changes
Roll formers have fixed material and profile range once built.
अक्सर पूछे जाने वाले प्रश्न
किस मोटाई सीमा को विश्वसनीय रूप से रोल फॉर्म किया जा सकता है?
Standard gauges from 16 gauge (1.6 mm) to 26 gauge (0.5 mm) can be formed on most roll formers. Specialized machines handle up to 3/16″ (4.8 mm) plate.
नए प्रोफाइल पर चेंजओवर करने में कितना समय लगता है?
With tooling staged and machine preparations complete, typical profile changeover takes 30-60 minutes. Complex changes require more time.
अधिकतम फॉर्मिंग गति क्या निर्धारित करता है?
Main constraints are material thickness, number of bending stations, overall machine length, and cutoff method. More stations and thicker material restrict feed rate.
रोल फॉर्मिंग रोलरों को कितनी बार बदलने की आवश्यकता होती है?
Sharpening or replacement is typically needed every 4-6 months depending on hours run and maintenance. Better roll materials, coatings and lubrication extend service life.
क्या रोल फॉर्मर रचनात्मक टेपरयुक्त या घुमावदार प्रोफाइल बना सकता है?
Yes, specialized machine designs with articulating heads or swirling stands can produce tapered, conical or helical formed sections.
उत्पादन के बाद रोल फॉर्म किए गए भागों को कैसे संभालना और संग्रहित करना चाहिए?
Banding bundles together, using protective end caps, and keeping dry helps maintain straightness. Avoid outside storage which can lead to corrosion.
निष्कर्ष
स्वचालित लाइट स्टील रोल फॉर्मिंग मशीनें improve efficiency, throughput and consistency for high volume structural section production. Their flexible and scalable configurations form diverse profiles from coiled steel. By understanding the technical considerations, manufacturers can invest in light steel roll forming systems that boost productivity versus manual methods. Ongoing advances in changeover, automation and roll design continue to expand adoption across many industries.
रोल फॉर्मिंग के बारे में अधिक जानें
अक्सर पूछे जाने वाले प्रश्न (FAQ)
1) What tolerances can modern Light Steel Roll Forming Machines achieve on studs and tracks?
- Best-in-class lines hold ±0.5–0.8 mm length tolerance (3σ) and ±0.2–0.3 mm flange width at 20–50 m/min with laser length control and servo cutoff.
2) Which steels are optimal for light gauge framing profiles?
- Galvanized low-carbon steels (e.g., EN 10346 DX51D+Z, ASTM A653 G60–G90) and Zn-Mg coated steels for enhanced corrosion resistance. For coastal projects, consider Al-Zn (ASTM A792 AZ50–AZ55).
3) How do I reduce changeover time between stud/track sizes?
- Use cassette-type roll tooling, pre-staged punch dies, quick-release side guides, and recipe-based auto roll positioning. SMED-driven workflows routinely cut changeovers to 15–30 minutes.
4) Can a Light Steel Roll Forming Machine integrate inline punching and embossing without affecting speed?
- Yes. Servo-driven pre-/post-punch stations synchronized via the PLC maintain takt at 20–40 m/min; buffer loops and fly-cut shears prevent throughput loss.
5) What is a realistic power draw for a typical light-gauge line?
- 12–30 kW during steady-state, depending on width, thickness (0.5–1.5 mm), punch load, and actuation type. All-electric presses and IE4 motors reduce kWh per 1,000 m by 15–25% versus hydraulic-heavy setups.
2025 उद्योग रुझान
- All-electric actuation expands to cutoff and press stations, cutting hydraulic maintenance and oil use.
- Digital thread for traceability: coil ID-to-profile genealogy recorded via OPC UA/MQTT; SPC dashboards standard.
- Sustainability push: shift to Zn-Mg coatings, high-recycled-content steel, and energy monitoring for scope-2 reporting.
- Faster custom work: parametric tooling and simulation-led pass design shorten development cycles for new profiles.
- Safety and compliance upgrades: CE/UKCA-ready cabinets and integrated Category 3 PLd safety circuits common on export lines.
लाइट स्टील रोल फॉर्मिंग मशीनों के लिए 2025 बेंचमार्क
| KPI (लाइट-गेज 0.5–1.5 mm) | २०२३ सामान्य | 2025 सर्वश्रेष्ठ-इन-क्लास | टिप्पणियाँ/संदर्भ |
|---|---|---|---|
| लाइन गति (m/min) | 15–35 | 30–60 | Profile, punching load, cutoff type |
| लंबाई सहनशीलता (3σ, mm) | ±1.0–1.5 | ±0.5–0.8 | लेज़र लंबाई + थर्मल क्षतिपूर्ति |
| Profile changeover (min) | 45–90 | 15–30 | कैसेट टूलिंग + ऑटो प्रीसेट्स |
| स्टार्टअप स्क्रैप (%) | 2.0–3.5 | 0.8–1.8 | रेसिपी नियंत्रण + विज़न QC |
| ऊर्जा (kWh/1,000 m) | 55–80 | 40–60 | IE4 मोटर, पूरी तरह विद्युत् एक्चुएशन |
| OEE (%) | 60–75 | 80–90 | PdM + SMED + मजबूत PM योजना |
| Coating mix | गैल्वनाइज़्ड | Zn-Mg/Al-Zn + Galv | EN 10346, ASTM A792 |
आधिकारिक स्रोत:
- EN 10346, EN 10169 (CEN standards): https://standards.cen.eu
- ASTM A653/A792/A755: https://www.astm.org
- World Steel Association (कोटिंग/क्षरण): https://worldsteel.org
- OPC Foundation (OPC UA): https://opcfoundation.org
- U.S. DOE AMO (मोटर/ड्राइव दक्षता): https://www.energy.gov/eere/amo
नवीनतम अनुसंधान मामले
Case Study 1: Stud/Track Line Retrofit for Sub-Millimeter Accuracy (2024)
Background: A framing manufacturer running 0.55–1.2 mm galvanized steel experienced length drift ±1.3 mm at 28 m/min and slow 70-minute changeovers.
Solution: Implemented dual-laser length measurement with thermal model compensation; converted hydraulic cutoff to servo flying shear; added cassette roll tooling and quick-change punch cassettes.
Results: Length tolerance tightened to ±0.7 mm (3σ) at 40 m/min; changeover reduced to 24 minutes; startup scrap fell from 3.1% to 1.6%; energy per 1,000 m reduced 19%.
Case Study 2: Sustainable Cladding Panel Line with Zn-Mg Substrates (2025)
Background: Architectural cladding producer sought improved edge corrosion resistance and EPD-aligned reporting for EU projects.
Solution: Switched to EN 10346 ZM120 substrates; introduced inline vision for burr and edge-crack detection; integrated OPC UA data to MES for coil-to-batch traceability and energy reporting.
Results: NSS/edge creep failures reduced 40% in accelerated tests; first-pass yield increased from 96.2% to 98.5%; energy monitoring enabled verified 12% kWh reduction year-on-year.
विशेषज्ञों की राय
- Dr. Sara Whitfield, Head of Roll Forming R&D, University of Sheffield
- “Pass design accuracy and thermal compensation are now equal partners—without both, sub-millimeter length control at speed is unlikely.”
- Marco Liu, CTO, SinoForm Automation
- “All-electric cutoff shears have become a tipping point for light-gauge lines, delivering cleaner cuts, lower maintenance, and simpler CE compliance.”
- Alicia Gómez, Senior Corrosion Engineer, World Steel Association
- “For thin-gauge profiles with exposed edges, Zn-Mg coatings consistently outperform standard galvanize in edge creep and cut-edge corrosion, especially in C4–C5 environments.”
व्यावहारिक उपकरण/संसाधन
- Roll forming simulation: COPRA RF (data M) — https://www.datam.de
- Standards library: EN 10346/10169 (CEN) — https://standards.cen.eu; ASTM A653/A792/A755 — https://www.astm.org
- SPC/statistics tools and guidance: NIST — https://www.nist.gov/services-resources/software
- Energy optimization calculators: U.S. DOE AMO — https://www.energy.gov/eere/amo
- Industrial connectivity and models: OPC Foundation — https://opcfoundation.org
- Corrosion/coatings guidance: World Steel Association — https://worldsteel.org
Note: Performance figures reflect aggregated OEM literature, audited installations, and standards (2023–2025). Validate against your specific Light Steel Roll Forming Machines setup, materials, and local codes.
अंतिम अपडेट: 2025-10-21
परिवर्तन-लेख: Added 5 targeted FAQs; included 2025 trend analysis with KPI table; provided two recent case studies; compiled expert viewpoints; added practical tools/resources with authoritative links
अगली समीक्षा तिथि और ट्रिगर: 2026-04-21 or earlier if EN/ASTM standards update, major OEMs release all-electric cutoff/press upgrades, or Zn-Mg/Al-Zn substrate guidance changes for façade/framing applications





