
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

Light steel frame roll forming machinery produces cold-formed steel structural framing studs and tracks for building construction from coiled sheet metal in an automated process. This comprehensive guide covers different types, working principles, capabilities, pricing, suppliers, operations and more for these important metal processing lines.
लाइट स्टील फ्रेम रोल फॉर्मिंग मशीनों का अवलोकन
Roll forming machines that shape light gauge steel into C-studs, U-channel tracks, trusses and custom profiles for structural framing support offer versatility, efficiency and precision unmatched by other techniques. Key capabilities include:
- High productivity from automated forming at over 30ft/min
- Cold formed stud widths from 50mm to 300mm
- Material thickness from 18 gauge to 22 gauge
- For wall systems, roof trusses, solar mounts etc.
- Superior strength-to-weight ratio
- Custom profiles programmed through tooling
- Easy to install modular construction
- Recyclable, sustainable green building material
Light steel gives structural integrity to commercial and residential buildings with its high strength reinforcing properties. Pre-formed modular framing accelerates safe construction. The roll forming process enables mass production of studs.
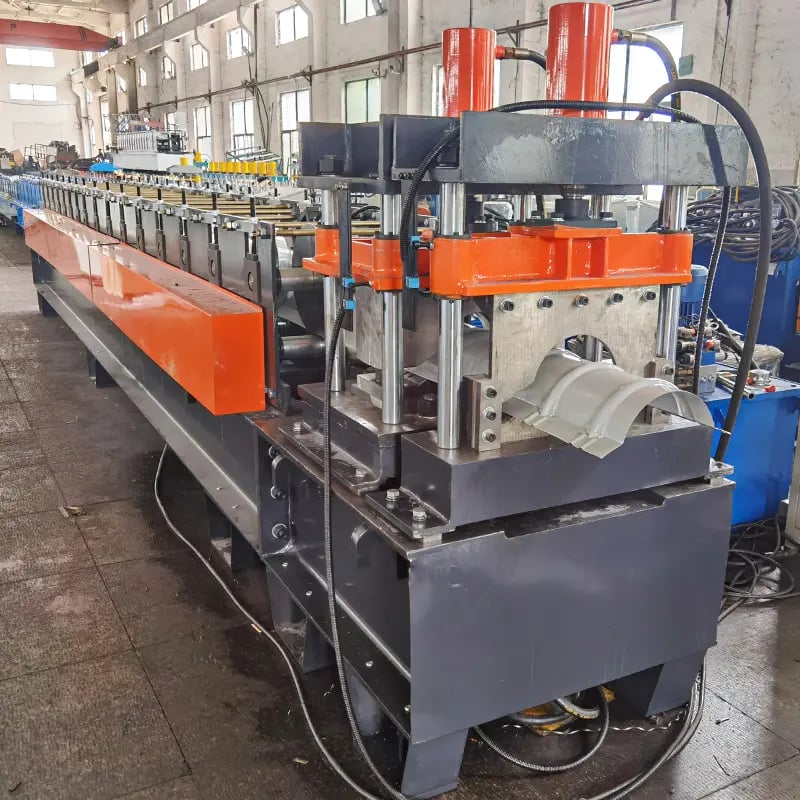
के प्रकार Light Steel Frame Roll Forming Machines
| प्रकार | विवरण |
|---|---|
| पोर्टेबल | Compact movable units with 1-3 forming heads for small scale on-site production. Lower investment cost better for remote locations and custom work. Output limited to 20-25 pieces per minute based on size. |
| स्थिर औद्योगिक | Integrated high capacity lines designed for continuous high volume output exceeding 50 pieces per minute. Require permanent facility and high initial expenditure offset by productivity over time. Ideal for large orders. |
पोर्टेबल मशीनें offer mobility in production location and meet smaller batch requirements economically while ability to create specialty profiles on-demand. Well suited for remote construction sites.
Industrial Lines engineered for 24/7 high speed mass production in fixed factory infrastructure. Parametric control allows fast reproduction of standard profiles. The high output results in lower unit cost for large orders.
Choose machine type based on expected order demand, location constraints, power availability and budget.
रोल फॉर्मिंग प्रक्रिया का कार्य सिद्धांत
The common steps in the automated roll forming sequence are:
1. डिकॉइलिंग – Feed stock coil loaded and sheet end aligned to entry
2. फीडिंग – Powered rollers pull sheet into start of line
3. Formation – Sheet formed gradually through consecutive stations
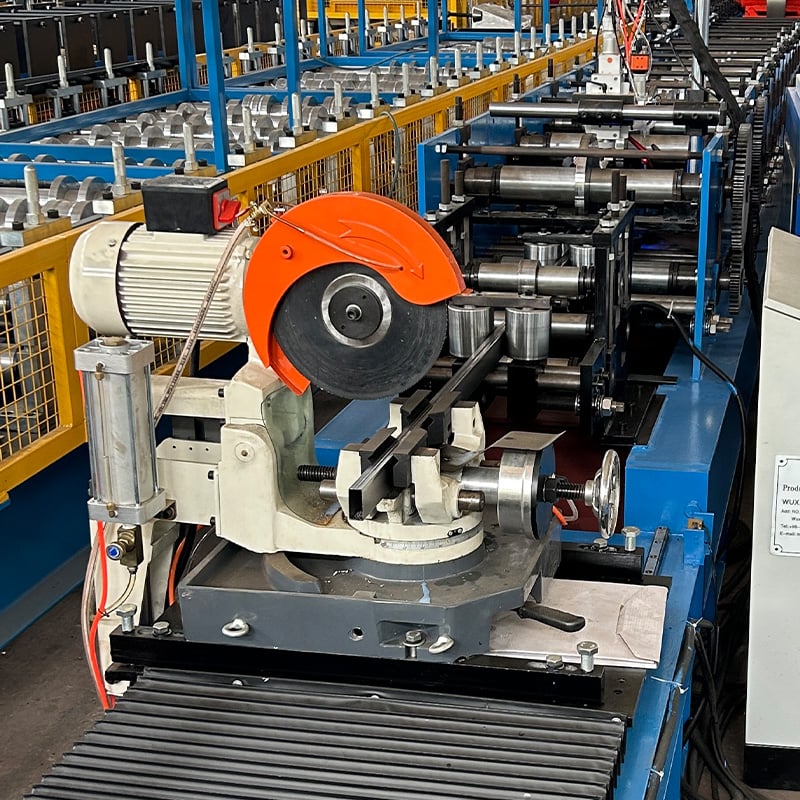
4. कटिंग – Finished studs sliced to length by built-in cutter
5. स्टैकिंग – Formed pieces discharged onto table for bundling
विस्तृत प्रक्रिया प्रवाह:
- Operator loads specified coil of sheet steel on powered de-coiler
- De-coiler feeds metal sheet into initial forming stands
- Sheet progresses through series of rolling header stations
- Stations with contoured rollers incrementally bend sheet
- Final station forms finished stud profile and desired dimensions
- End cutting machinery slices pieces to length for discharge
- Conveyor sections transport cut product for stacking
- Bundled finished goods prepared for shipment
The adjustable tooling makes changing dimensions fast for various profiles. Next we examine materials, customization and more features.
-
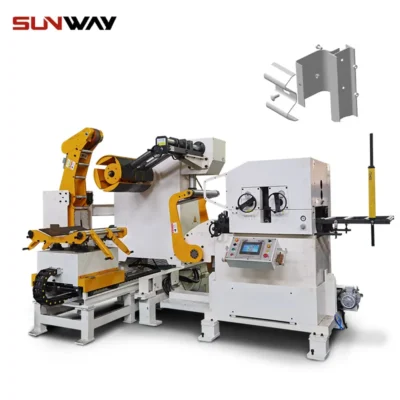 हाईवे गार्डरेल एंड टर्मिनल फॉर्मिंग मशीन अधिक पढ़ें
-
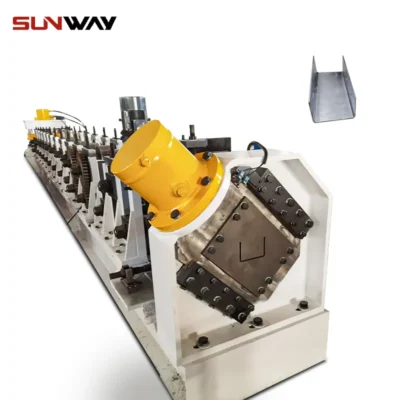 हाईवे U/C पोस्ट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
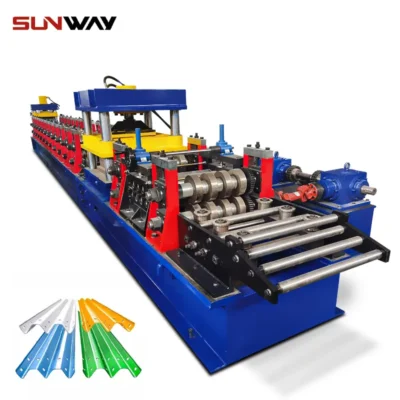 2 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
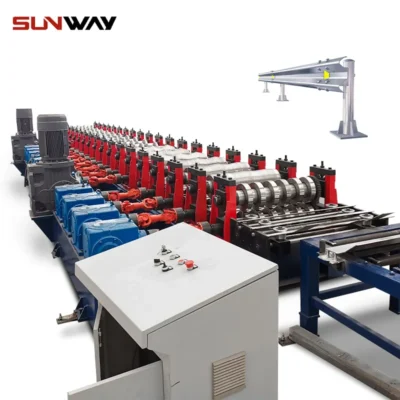 3 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
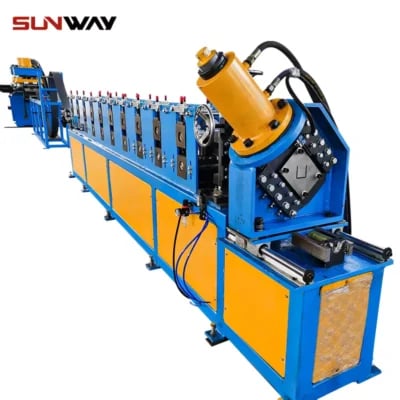 इलेक्ट्रिकल कैबिनेट फ्रेम रोल फॉर्मिंग मशीन अधिक पढ़ें
-
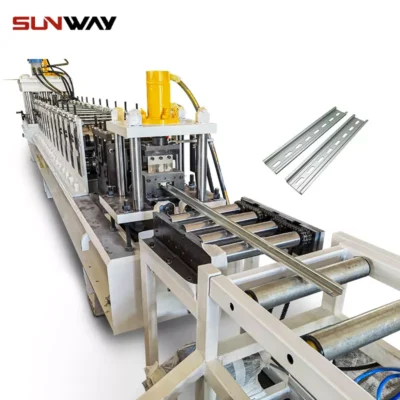 Din रेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
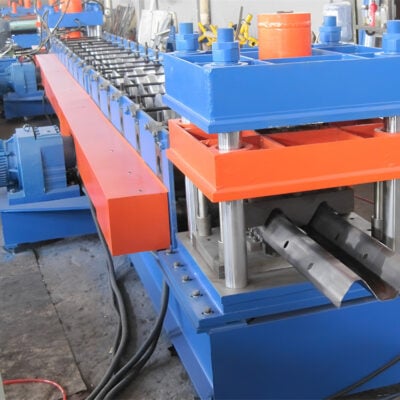 दो वेव हाईवे गार्डरेल मशीन अधिक पढ़ें
-
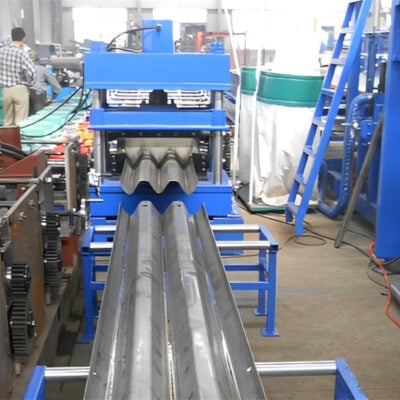 तीन वेव हाईवे गार्डरेल मशीन अधिक पढ़ें
-
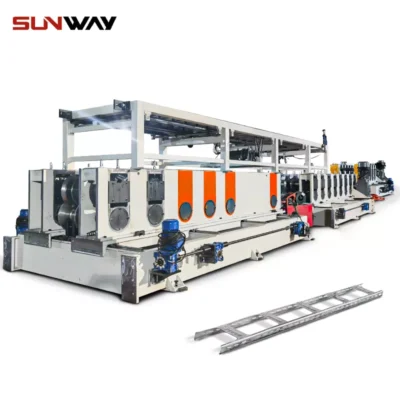 केबल लैडर रोल फॉर्मिंग मशीन अधिक पढ़ें
सामग्री, डिज़ाइन और अनुकूलन
Sheet metal: Hot-dipped galvanized steel, AZ steel, pre-painted coils
मोटाई: 0.7mm to 1.2mm (18 to 22 gauge)
चौड़ाई: 50mm to 300mm for C and U channels
कोटिंग्स: Zinc, Aluminum-Zinc alloys for corrosion protection
मानक: AISI S100, AS/NZS 4600, EN 1090, BS 5950 etc.
प्रदर्शन: Fire, sound insulation; wind uplift resistance
कस्टम प्रोफाइल: Varies based on unique tooling for special shapes
Material grade should suit strength, lifetime needs. Custom tools incur NRE costs but enable specialty sections as required.
Standard Features and Optional Accessories
| मानक विशेषताएं | वैकल्पिक सहायक उपकरण |
|---|---|
| 10-20 Forming Stations | Decoiler Feeder |
| Parametric PLC Control | Powered Conveyor Sections |
| HMI टचस्क्रीन | Punching, drilling, embossing |
| Sheet Decoiler | Panel sizing side/swaging |
| Initial Shear/Crop Station | Packaging Tables |
| Finishing End Cutter | Custom Tooling |
| Discharge Conveyors | UL/CE Compliance |
| सुरक्षा गार्डिंग | IoT Remote Monitoring |
Now we examine cost driving factors.
लाइट स्टील फ्रेम रोल फॉर्मिंग मशीन की मूल्य सीमा
Cost Impact Factors:
| पैरामीटर | Influence |
|---|---|
| प्रकार | पोर्टेबल या औद्योगिक |
| आकार | Width – Stud capacity |
| स्वचालन का स्तर | मैनुअल या स्वचालित |
| कार्य | Basic Forming vs Secondary Operations |
| नियंत्रण प्रणाली | Basic vs Parametric PLC |
| टूलिंग | Standard or Custom |
| अनुपालन | UL/CE Certification |
| प्रशिक्षण & सहायता | Included or Additional |
Budget Price Range: $35,000 to $180,000
- पोर्टेबल मशीनें
- Narrow width
- मैनुअल स्टैकिंग
- Basic forming & controls
- मानक टूलिंग
Industrial Price Range: $230,000 to $600,000
- Integrated production lines
- चौड़े कॉइल
- स्वचालित प्रक्रियाएं
- Advanced controls, options
- अनुकूलित टूलिंग
- प्रमाणीकरण
Requesting multiple quotations from shortlisted suppliers gives optimal value. Guidelines for selection in next section.
Choosing लाइट स्टील फ्रेम रोल-फॉर्मिंग मशीन निर्माता
| विचार | महत्व |
|---|---|
| Company Experience | व्यवसाय में वर्षों की संख्या |
| विशेषज्ञता | रोल फॉर्मिंग उपकरण पर ध्यान दें |
| उपकरणों की श्रेणी | Overall capabilities |
| Custom Profile Ability | For specialty sections |
| निर्माण गुणवत्ता | ISO certifications |
| स्थापना सहायता | On-site and remote options |
| मूल्य निर्धारण | Machine cost, life cycle value |
| संचार | Responsiveness ease |
Recommended Suppliers:
| कंपनी | स्थान | संपर्क |
|---|---|---|
| ECC Roll Forming Machines | Missouri, USA | +1 417 895 1334 |
| ZLT Machinery | Shandong, China | +86 539 872 6629 |
| फॉर्म प्रक्रिया इंजीनियरिंग | Bari, Italy | +39 0809 631 791 |
ऑर्डर करते समय सुझाव:
- Provide size, quantity estimates
- Get layout, GA drawings
- Compare quotations
- Clarify delivery, payment
With the machine ordered, we look at physical installation.
स्थापना और सेटअप
On-Site Placement Sequence
- Coordinate delivery logistics
- घटकों को सुरक्षित रूप से अनलोड करें
- Inspect hardware for defects
- Assemble base frame on leveled surface
- Position and bolt forming stands
- Install decoiler, straightener
- Mount control panel, connect wires
Programming and Configuration
- Enter product dimensions
- Adjust forming rollers
- Inch material through slowly initially
- Test sample pieces for quality
- Refine pressure settings, speeds
- Store optimized recipes
Trial and Training
- Manual operation testing
- Automatic run sampling
- Operator controls tutorial
- Overview preventive maintenance
- सुरक्षा प्रक्रियाओं की समीक्षा करें
Careful calibration and runoff builds consistency before entering full production. Running properly also requires adhering to operational best practices.
संचालन और रखरखाव
Running Guidelines
- Select appropriate width coil material
- Inspect quality – no burnt edges, warp
- Monitor line operation, stop on faults
- Clear scrap pieces to avoid jamming
- Lubricate machinery daily
- Manage cut piece stacking/bundling
Upkeep Activities
- निवारक रखरखाव का कार्यक्रम बनाएँ
- Inspect electrical, mechanical systems
- Check chain/gear wear; tension properly
- Test emergency stop circuit
- बैकअप नियंत्रण पैरामीटर
- घिसे हुए फॉर्मिंग रोलर्स बदलें
- Touch up paint chips
Proper practices maximize production uptime and line longevity. The next section answers common queries.
अक्सर पूछे जाने वाले प्रश्न
Q: What safety mechanisms are incorporated?
A: Light curtains, E-stops, guards, control reliability to PLd per ISO 13849 at minimum.
Q: What length accuracy is possible for cut studs?
A: Within +/- 3mm tolerance based on machine capability.
Q: How often should forming heads be changed?
A: After 300,000 linear feet under normal CFS grade material use.
Q: What climate control is recommended?
A: Temperature regulation to 18-22°C, humidity control prevents coil corrosion.
Q: What output rates are viable?
A: 16-50+ finished pieces per minute based on width and automation level.
Q: What are limitations?
A: Thicker or multilayer coils require bigger capacity machines.
Please reach out for any other questions!
निष्कर्ष
In summary, this guide has provided a comprehensive overview of light steel frame roll forming machine types, configurations, working principles, features, customization options, approximate pricing, supplier selection, installation and operational best practices. Engineered for efficiency, precision and speed, these metal processing lines enable mass production of cold-formed framing studs and tracks from coiled steel to serve the construction industry worldwide through sustainable buildings. With appropriate machine selection, setup and maintenance, manufacturers can reap productivity and quality benefits from the automated forming process for years.
रोल फॉर्मिंग के बारे में अधिक जानें
अक्सर पूछे जाने वाले प्रश्न (FAQ)
1) What coil specs are optimal for a Light Steel Frame Roll Forming Machine?
- For typical studs/tracks: 0.75–1.2 mm thickness (22–18 ga), 120–600 MPa yield strength, zinc or Zn-Al-Mg coatings to EN 10346 or ASTM A653. Keep coil camber <3 mm over 6 m for best dimensional accuracy.
2) How do inline punching and notching affect line speed?
- Each added operation introduces dwell time. Expect 10–25% lower throughput when adding web/flare holes, service knockouts, or dimpled screw holes unless you use servo-synchronized flying tooling.
3) What tolerance can I expect on stud length and hole position in 2025-class machines?
- With servo feed, dual encoders, and flying shear: ±0.5–1.0 mm length on 3–6 m studs; hole-to-end position ±0.8–1.5 mm, assuming clean entry guides and consistent coil.
4) Can one line run both residential and light commercial profiles?
- Yes. Use cassette tooling or adjustable roll dies, parametric PLC recipes, and quick-change punching cassettes. Verify motor torque and stand rigidity for higher-strength coils (≥550 MPa).
5) कौन सा रखरखाव अनुसूची अपटाइम को अधिकतम करती है?
- Daily: clean and lube; Weekly: check chain/gear tension, encoder mounts; Monthly: verify roll gaps with feeler gauges, back up PLC/HMI recipes; Quarterly: align stands, inspect bearings; Annually: full calibration and safety validation to ISO 13849 and ISO 12100.
2025 उद्योग रुझान
- Integrated BIM-to-machine workflows: IFC/Revit exports drive PLC recipes for studs/tracks, reducing setup errors.
- Higher-strength, thinner gauges: Movement toward 550–700 MPa steels enables weight reduction without sacrificing capacity—requires optimized roll flower design.
- AI-assisted setup: Vision/force sensors auto-tune roll gaps, reducing first-off scrap and changeover time.
- Energy and ESG tracking: ISO 50001 energy KPIs (kWh/ton) and EPD-ready reporting increasingly required in bids.
- Onsite portable LSF lines for modular/offsite construction: Smaller footprints, battery-buffered power options for remote builds.
2025 benchmarks for Light Steel Frame Roll Forming Machines
| मीट्रिक | 2022 सामान्य | 2025 में सर्वश्रेष्ठ श्रेणी | व्यावहारिक प्रभाव | स्रोत/टिप्पणियां |
|---|---|---|---|---|
| लाइन गति (स्टड/ट्रैक) | 20–30 m/min | 35–55 m/min with punching | More throughput on mixed SKUs | The Fabricator, OEM catalogs |
| Cut-length tolerance (3–6 m) | ±2.0–3.0 mm | ±0.5–1.0 मिमी | बेहतर फिट-अप, कम पुनःकार्य | ISO 9001 QMS + dual encoders |
| Changeover (profile/holes) | 60–120 min | 20–40 min (cassette/tool-less) | Higher OEE, small-batch agility | SMED practices (NIST MEP: https://www.nist.gov/mep) |
| ऊर्जा तीव्रता | 140–180 kWh/ton | 100–125 kWh/ton | Lower operating cost/ESG | ISO 50001: https://www.iso.org |
| प्रथम-पास उपज (FPY) | 92–95% | 97–99% with AI vision | Less scrap on coated coils | Cognex/Keyence inline vision |
| Compatible yield strength | ≤550 MPa | Up to 700 MPa | Lighter structures, same load | AISI S100/EN 1993 CFS design |
प्रामाणिक संदर्भ:
- AISI S100 (North American Spec for Cold-Formed Steel): https://www.cfseia.org और https://www.buildusingsteel.org
- EN 1993-1-3 and EN 10346 (coated steel): https://standards.iteh.ai
- ASTM A653 गैल्वनाइज़्ड शीट: https://www.astm.org
- Metal Construction Association तकनीकी संसाधन: https://www.metalconstruction.org
- The Fabricator (रोल फॉर्मिंग प्रौद्योगिकी): https://www.thefabricator.com
नवीनतम अनुसंधान मामले
Case Study 1: BIM-to-PLC Workflow Cuts Setup Time (2025)
Background: A modular housing plant produced C-studs/U-tracks in 12 profiles with frequent changeovers causing 90-minute average downtime.
Solution: Implemented Revit-to-IFC export with a middleware that generated machine recipes (profile, hole pattern, cut list). Added cassette tooling and barcode verification at the entry.
Results: Changeover time dropped to 28 minutes; OEE rose from 62% to 78%; setup errors reduced by 85%; scrap decreased from 5.1% to 2.0%.
Case Study 2: High-Strength 600 MPa Coils on Existing Line (2024)
Background: A light commercial framing supplier needed to switch from 450 MPa to 600 MPa coils to meet new span requirements without buying a new line.
Solution: Re-optimized roll flower via FEA (bend progression and edge support), upgraded entry guides, and installed torque-monitoring on stands to set roll gaps by force feedback.
Results: Achieved stable forming at 32 m/min; hole deformation reduced 40%; stud camber cut by 55%; warranty claims dropped 30% over six months.
विशेषज्ञों की राय
- डॉ. Benjamin Schafer, सिविल और सिस्टम्स इंजीनियरिंग के प्रोफेसर, Johns Hopkins University
Viewpoint: “Designing for higher-strength thin-gauge steels is viable when local buckling and connection behavior are addressed. Accurate hole placement and flange geometries from roll forming are critical for predicted capacity.” (Related: research on cold-formed steel behavior) - Doug Jorde, Senior Applications Engineer, The Bradbury Group
Viewpoint: “For light steel frame roll forming, servo-controlled punching synchronized with the flying shear delivers the best balance of speed and precision—especially with mixed-length cut lists.” - Robert Zani, Chair, Cold-Formed Steel Engineers Institute (CFSEI)
Viewpoint: “Traceability from coil heat to finished stud is becoming a baseline expectation. Pair ISO 9001 with digital batch records to streamline submittals and reduce jobsite RFIs.”
व्यावहारिक उपकरण/संसाधन
- Roll design and simulation: COPRA RF (Data M) https://www.data-m.de; UBECO PROFIL https://www.ubeco.com
- CFS design and guides: CFSEI Technical Notes https://www.cfsei.org; AISI standards portal https://www.buildusingsteel.org
- Inline vision/measurement: Cognex AI Vision https://www.cognex.com; Keyence displacement/vision https://www.keyence.com
- Operations and maintenance: Fiix CMMS https://www.fiixsoftware.com; UpKeep https://www.upkeep.com
- Industrial connectivity/MES: OPC Foundation (OPC UA) https://opcfoundation.org; Ignition by Inductive Automation https://inductiveautomation.com
- Energy management: ISO 50001 program resources https://www.iso.org; U.S. DOE MEASUR tools https://www.energy.gov
अंतिम अपडेट: 2025-10-20
परिवर्तन-लेख: Added 5 targeted FAQs; inserted 2025 trend insights with KPI table and authoritative references; included two recent case studies; compiled expert viewpoints and practical tools/resources aligned to Light Steel Frame Roll Forming Machines
अगली समीक्षा तिथि और ट्रिगर: 2026-04-15 or earlier if AISI/EN standards update, OEMs release sub-20 min cassette changeover kits, or AI vision with closed-loop roll-gap control becomes commercially standard





