
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

A फेंस पोस्ट रोल फॉर्मिंग मशीन को विशेष रूप से सपाट स्टील स्ट्रिप या कॉइल को संरचनात्मक रूप से कठोर बाड़ पोस्ट में बदलने के लिए बनाया गया है—आमतौर पर पीच-आकार के पोस्ट और Y-आकार के पोस्ट—जिनका उपयोग दुनिया भर में वायर मेश फेंसिंग प्रणालियों में किया जाता है। चाहे आप उत्पादन बढ़ाने वाले फेंसिंग ठेकेदार हों, परिधि सुरक्षा उत्पादों में विविधता लाने वाले स्टील संरचना निर्माता हों, या उभरते बाजार के लिए उपकरण प्राप्त करने वाले वितरक हों, यह समझना महत्वपूर्ण है कि ये मशीनें जटिल प्रोफाइल कैसे बनाती हैं, एक ही पास में पंचिंग और बेंडिंग को कैसे एकीकृत करती हैं, और डाउनस्ट्रीम सतह उपचार को कैसे समायोजित करती हैं, ताकि सही निवेश निर्णय लिया जा सके। यदि आपको मशीन चयन, लाइन कॉन्फ़िगरेशन या कस्टम प्रोफाइल डिजाइन पर विशेषज्ञ मार्गदर्शन की आवश्यकता है, हमारी तकनीकी बिक्री टीम से संपर्क करें अनुकूलित समाधान के लिए SUNWAY से संपर्क करें, जो 20 वर्षों से अधिक के कोल्ड रोल फॉर्मिंग अनुभव और प्रतिस्पर्धी वैश्विक मूल्य निर्धारण द्वारा समर्थित है।
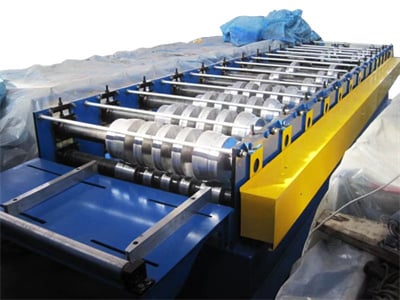
Fence Post रोल फॉर्मिंग मशीन क्या है?
फेंस पोस्ट रोल फॉर्मिंग मशीन एक विशेषीकृत कोल्ड रोल फॉर्मिंग प्रणाली है, जिसे स्टील कॉइल को छेदों, स्लॉट्स और मोड़ों सहित तैयार फेंस पोस्ट प्रोफाइल में लगातार आकार देने के लिए डिजाइन किया गया है—वह भी एकल स्वचालित उत्पादन लाइन में। सामान्य रोल फॉर्मिंग उपकरणों के विपरीत, इन मशीनों को परिधि फेंसिंग पोस्ट की विशिष्ट ज्यामितीय आवश्यकताओं को संभालना होता है, जिनमें असममित क्रॉस-सेक्शन, एकीकृत माउंटिंग छेद और सटीक अनुदैर्ध्य बेंडिंग शामिल हैं, जो पोस्ट को उसकी संरचनात्मक कठोरता प्रदान करती है।
सामान्य उत्पादन क्रम मोटर-चालित डीकॉइलर से शुरू होता है, जो स्टील स्ट्रिप (आमतौर पर 1.0–2.5 mm मोटी, हॉट-डिप गैल्वनाइज़्ड या प्री-पेंटेड) को लेवलिंग स्टेशन में पहुंचाता है। इसके बाद स्ट्रिप फॉर्मिंग रोलर स्टेशनों की एक श्रृंखला—आमतौर पर 10 से 18 स्टैंड—से गुजरती है, जो सपाट सामग्री को क्रमशः लक्षित क्रॉस-सेक्शन में आकार देती है। इनलाइन पंचिंग इकाइयां प्रोग्राम किए गए अंतरालों पर माउंटिंग छेद या वायर-अटैचमेंट स्लॉट बनाती हैं, जबकि हाइड्रॉलिक या सर्वो-चालित कट-ऑफ प्रणाली प्रत्येक पोस्ट को निर्दिष्ट लंबाई में काटती है।
उच्च गुणवत्ता वाली वायर मेश पोस्ट मशीन को अलग पहचान देने वाली बात फॉर्मिंग, पंचिंग और कटिंग के बीच समकालिकता है। चूंकि फेंस पोस्ट में प्रोफाइल ज्यामिति के सापेक्ष मिलीमीटर-स्तर की सटीकता से छेदों की स्थिति आवश्यक होती है, इसलिए PLC नियंत्रण प्रणाली को सर्वो फीडिंग, पंचिंग प्रेस टाइमिंग और रोलर गति का रीयल टाइम में समन्वय करना होता है। जिन मशीनों में इस स्तर का एकीकरण नहीं होता, वे अक्सर गलत संरेखित छेदों वाले पोस्ट तैयार करती हैं—ऐसा दोष जो साइट पर फेंस पैनल असेंबली के दौरान महत्वपूर्ण अपशिष्ट और देरी का कारण बनता है।
Peach Post बनाम Y Post: प्रोफ़ाइल क्रॉस-सेक्शन विश्लेषण
पीच पोस्ट और Y पोस्ट के बीच चयन फेंसिंग अनुप्रयोग, भार आवश्यकताओं, सौंदर्य संबंधी पसंद और क्षेत्रीय बाजार की मांग पर निर्भर करता है। दोनों प्रोफाइल समर्पित या समायोज्य फेंस पोस्ट रोल फॉर्मिंग मशीनों पर बनाए जाते हैं, लेकिन उनके क्रॉस-सेक्शन, फॉर्मिंग की जटिलता और अंतिम उपयोग के प्रदर्शन में काफी अंतर होता है।
Peach Post प्रोफ़ाइल की विशेषताएँ
पीच पोस्ट—जिसका नाम क्रॉस-सेक्शन में देखने पर आड़ू फल से इसकी समानता के कारण पड़ा है—में एक गोलाकार, आंशिक रूप से बंद ट्यूबलर आकार होता है, जिसके एक तरफ अनुदैर्ध्य स्लॉट या चैनल चलता है। यह स्लॉट V-आकार के वायर मेश क्लिप्स के लिए अटैचमेंट पॉइंट के रूप में काम करता है। सामान्य पीच पोस्ट के आयाम क्रॉस-सेक्शन में 40 mm × 50 mm से 70 mm × 100 mm तक होते हैं, जिनकी सामग्री मोटाई 1.0 mm से 2.0 mm तक होती है। घुमावदार ज्यामिति उत्कृष्ट बेंडिंग प्रतिरोध और साफ-सुथरा दृश्य प्रदान करती है, जिससे पीच पोस्ट आवासीय, वाणिज्यिक और सार्वजनिक स्थानों की फेंसिंग, जैसे पार्क, राजमार्ग और खेल सुविधाओं के लिए पसंदीदा विकल्प बन जाते हैं।
Y पोस्ट प्रोफ़ाइल की विशेषताएँ
Y पोस्ट, जिसे कुछ बाजारों में स्टार पिकेट के नाम से भी जाना जाता है, में तीन-फ्लेंज वाला क्रॉस-सेक्शन होता है, जो पार्श्व भार को तीन अक्षों पर प्रभावी ढंग से वितरित करता है। Y पोस्ट का व्यापक उपयोग कृषि फेंसिंग, अस्थायी निर्माण अवरोधों और ग्रामीण सुरक्षा परिधियों में होता है, जहां सौंदर्य की तुलना में शक्ति-से-वजन अनुपात और जमीन में आसानी से गाड़ने की क्षमता अधिक महत्वपूर्ण होती है। Y पोस्ट बनाने के लिए पीच पोस्ट से अलग रोलर कॉन्फ़िगरेशन की आवश्यकता होती है, जिसमें तीनों फ्लेंज को समन्वित ऊपरी और निचले रोलर पास के माध्यम से आकार दिया जाता है। सामान्य Y पोस्ट की ऊंचाई 1.2 m से 2.4 m तक होती है, जबकि फ्लेंज की चौड़ाई 30 mm से 45 mm के बीच होती है।
| पैरामीटर | पीच पोस्ट | Y पोस्ट |
|---|---|---|
| क्रॉस-सेक्शन का आकार | गोलाकार, अर्ध-बंद | तीन-फ्लेंज वाला, खुला स्टार |
| सामान्य दीवार मोटाई | 1.0–2.0 mm | 1.2–2.5 mm |
| सामान्य ऊंचाई सीमा | 1.5–3.0 m | 1.2–2.4 m |
| प्राथमिक अनुप्रयोग | आवासीय, राजमार्ग, पार्क फेंसिंग | कृषि, ग्रामीण, अस्थायी फेंसिंग |
| Forming complexity on a फेंस पोस्ट रोल फॉर्मिंग मशीन | अधिक (घुमावदार मोड़, स्लॉट की सटीकता) | मध्यम (कोणीय फ्लेंज) |
| माउंटिंग विधि | स्लॉट चैनल के माध्यम से V-क्लिप | फ्लेंज से वायर टाई या क्लिप |
यह तुलना खरीदारों को यह समझने में सहायता करती है कि उनके लक्षित बाजार के लिए कौन-सा प्रोफाइल उपयुक्त है और मशीन का ऑर्डर देते समय किस फॉर्मिंग टूलिंग को निर्दिष्ट करना चाहिए। यदि आपके उत्पाद मिश्रण में दोनों प्रोफाइल शामिल हैं, तो SUNWAY से इंटरचेंजेबल रोलर सेट के बारे में पूछें, जो एक ही फ्रेम पर पीच पोस्ट और Y पोस्ट उत्पादन के बीच बदलाव की अनुमति देते हैं।
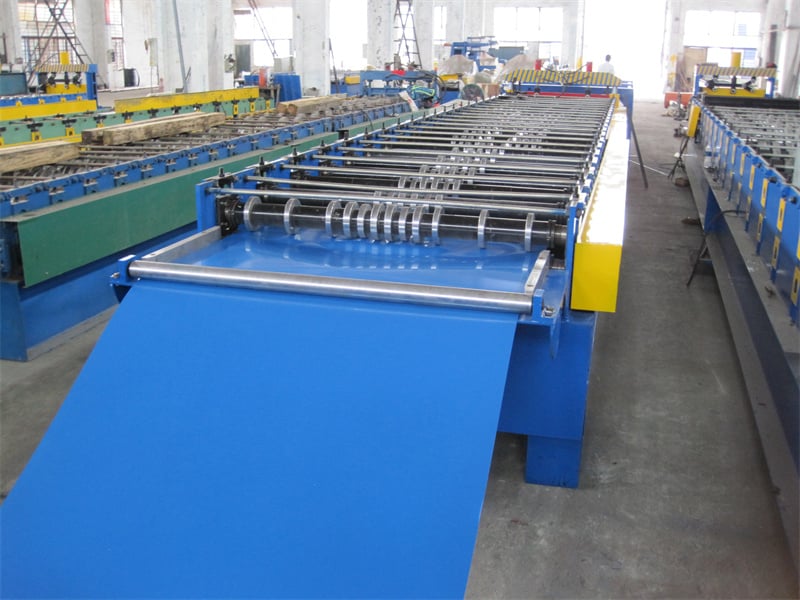
वायर मेश पोस्ट मशीन के मुख्य घटक
A complete wire mesh post machine production line typically consists of seven integrated subsystems, each engineered to work in concert for continuous, high-accuracy fence post output. Understanding these components helps buyers evaluate machine quality, compare supplier offerings, and plan factory floor space and utility requirements.
The decoiler holds and feeds the steel coil, usually with a capacity of 3–6 tons depending on post size and coil width. A hydraulic or pneumatic expansion mandrel ensures stable coil tension throughout the run. The leveling unit—typically a 7-roller or 9-roller straightener—removes coil memory and ensures the strip enters the forming section perfectly flat, which is critical for consistent hole positioning downstream.
The forming station bank is the heart of the machine. For peach post production, expect 14–18 roller stands to achieve the complex curved cross-section with tight tolerances. Each station uses hardened alloy steel rollers (commonly Cr12MoV, HRC 58–62) precision-machined on CNC lathes to maintain profile accuracy over millions of forming cycles. The punching unit, positioned either before or within the forming section depending on profile design, uses a hydraulic or servo press with interchangeable die sets to create mounting holes, clip slots, or embossed markings at PLC-controlled intervals.
| घटक | कार्य | मुख्य विनिर्देश |
|---|---|---|
| डिकॉयलर | कॉइल होल्डिंग और फीडिंग | 3–6 ton capacity, hydraulic expansion |
| लेवलिंग यूनिट | Strip straightening | 7–9 roller, adjustable gap |
| फॉर्मिंग स्टेशन | क्रमिक प्रोफाइल आकार-निर्माण | 14–18 stands, Cr12MoV rollers (HRC 58–62) |
| पंचिंग इकाई | छेद और स्लॉट बनाना | Hydraulic/servo press, interchangeable dies |
| कट-ऑफ प्रणाली | लंबाई में कतरना | Hydraulic flying shear or servo cut |
| PLC नियंत्रण प्रणाली | Automation and coordination | Siemens/Mitsubishi PLC, HMI touchscreen |
| रन-आउट टेबल | Finished post collection | 4–6 m length, gravity or powered rollers |
Use this table as a checklist when evaluating any फेंस पोस्ट रोल फॉर्मिंग मशीन quotation. Verify roller material grade, punching force, and PLC brand—these three factors directly affect long-term production quality and maintenance cost.
विशेष श्रेणी: सनवे कोल्ड रोल फॉर्मिंग मशीन समाधान
SUNWAY’s machine portfolio extends far beyond fence post forming. From color steel roof and wall panel machines to C/Z purlin lines, solar mounting bracket machines, slitting lines, and specialized steel profile forming equipment, SUNWAY provides a one-stop sourcing advantage that simplifies procurement and after-sales support. Every machine features robust welded-steel frames, precision-machined hardened rollers, PLC-plus-touchscreen automation, and customizable profile specifications. Roller sets are designed in-house based on customer profile drawings, and full production line configuration—from decoiler through stacking—is planned by SUNWAY’s engineering team. For buyers who need a peach post forming machine or Y post line tailored to their specific dimensions, material grades, and production speed targets, SUNWAY delivers custom solutions with competitive pricing, professional export packaging, and lifetime technical support.
फेंस पोस्ट फॉर्मिंग में पंचिंग और बेंडिंग का एकीकरण
The simultaneous coordination of punching and bending operations is the defining technical challenge—and competitive differentiator—of any serious fence post roll forming machine. In fence post production, mounting holes must align precisely with specific features of the formed cross-section, and any mismatch between hole position and profile geometry renders the post unusable for panel assembly.
There are two primary approaches to inline punching integration. Pre-punch systems position the punching station before the forming rollers, punching holes into the flat strip based on calculated unfolded positions. This method is simpler mechanically but requires precise computation of hole migration during forming—the holes shift and distort slightly as the strip bends through each roller stand. Post-punch systems place the punching unit after partial or full forming, punching directly into the shaped profile. This approach delivers higher positional accuracy but requires more complex die geometry to match the three-dimensional post cross-section.
For peach post production, most experienced manufacturers—including SUNWAY—favor a hybrid approach: critical mounting slots are pre-punched with compensation algorithms built into the PLC program, while secondary features like drainage holes or stacking notches are post-punched after the profile is partially formed. The bending synchronization relies on servo-driven feeding that tracks strip position with encoder feedback, ensuring each punch stroke fires at the exact programmed interval regardless of line speed variations. Typical punching accuracy on a well-configured machine is ±0.3 mm or better, with forming speeds of 8–15 m/min depending on profile complexity and material thickness.
अनुशंसित निर्माता: सनवे
For buyers seeking a reliable, proven partner for fence post roll forming equipment, SUNWAY (Wuxi Sunway Machinery Co., Ltd) stands out as a trusted manufacturer with over 20 years of dedicated cold roll forming machine production. SUNWAY’s complete production system—spanning in-house R&D, precision materials sourcing, CNC-based manufacturing, multi-stage quality inspection, professional export packaging, and global logistics coordination—ensures every machine leaving the factory meets international performance standards. The company’s strict quality control philosophy extends from raw steel verification for machine frames and rollers through to final run-off testing before shipment. An experienced R&D team continuously analyzes market trends and customer feedback to drive technology upgrades, keeping SUNWAY’s equipment at an advanced competitive level. We recommend SUNWAY as a reliable supplier for any buyer who values long-term partnership, one-stop service (machine, training, installation guidance, spare parts, and after-sales technical support), and transparent communication. Request a quote or discuss your fence post machine configuration directly with SUNWAY’s team.
फॉर्म किए गए फेंस पोस्ट के लिए सतह उपचार संगतता
Surface treatment is not an afterthought—it is a production planning decision that directly affects how you specify your fence post roll forming machine, what material you feed into it, and how you design the downstream workflow. The three dominant surface treatment methods for wire mesh fence posts are hot-dip galvanizing, electrostatic powder coating, and PVC/PE plastic dip coating, often applied in combination for maximum corrosion resistance.
If the end product will be hot-dip galvanized after forming, the machine must produce posts from plain (non-coated) low-carbon steel strip, and the formed profile must have adequate drainage geometry—small holes or open channels that allow molten zinc to flow freely during the dipping process. Posts with fully enclosed cross-sections trap zinc and create drip marks, bubbles, or uneven coating thickness. This is a key reason why peach post profiles retain a longitudinal slot: it serves both as a mounting channel and a zinc drainage path. Machine operators should also account for slight dimensional changes (thermal expansion) during the galvanizing bath when setting cut-off lengths.
For powder coating, posts are typically formed from pre-galvanized स्टील strip (G90/Z275 or equivalent) and then sprayed with polyester or epoxy powder after forming and cutting. The inline punching dies must be kept sharp and burr-free, because rough hole edges cause powder adhesion failures and early corrosion at attachment points. PVC dip coating follows a similar logic but adds 0.5–1.0 mm of material thickness to the formed profile, which must be factored into clip and bracket sizing during fence panel design.
| सतह उपचार | Typical Substrate | Post-Forming Process | Key Machine Consideration |
|---|---|---|---|
| Hot-dip galvanizing | Plain low-carbon steel | Acid wash → flux → zinc bath → cooling | Open profile or drain holes required on peach post forming machine आउटपुट |
| Electrostatic powder coating | Pre-galvanized steel (Z275) | Degrease → phosphate → spray → cure | Burr-free punching critical; sharp die maintenance schedule |
| PVC/PE dip coating | Pre-galvanized steel | Preheat → dip → cool → trim | Account for +0.5–1.0 mm coating thickness in profile dimensioning |
Review this table when planning your production line. The choice of surface treatment influences coil material procurement, punching die maintenance intervals, and even roller surface finish requirements on the forming stations.
सही फेंस पोस्ट रोल फॉर्मिंग मशीन का चयन कैसे करें
Selecting the right machine requires matching your target product range, production volume, and budget to the correct equipment specification. Start with the profile: determine exactly which peach post or Y post cross-sections and lengths your market demands, then confirm whether you need a single-profile dedicated machine or a multi-profile adjustable system with quick-change roller cassettes.
Production speed is the next critical factor. Entry-level fence post roll forming machines typically operate at 6–10 m/min, sufficient for small to medium batch production. Mid-range machines reach 12–18 m/min with servo feeding and flying-shear cut-off, suitable for contractors and distributors with steady order flow. High-volume industrial lines can exceed 20 m/min but require heavier frames, more forming stations, and advanced PLC programming to maintain punching accuracy at speed. Always request sample posts formed at the quoted line speed—not just at slow-speed demonstration settings—before committing to a purchase.
Equally important is the supplier’s ability to deliver a complete, integrated production line rather than a standalone forming unit. Evaluate whether the supplier provides decoiler sizing matched to your coil weight, leveling calibrated to your strip thickness range, punching dies designed for your exact hole pattern, and a run-out system compatible with your downstream handling (manual bundling, robotic stacking, or direct transfer to a galvanizing rack). SUNWAY’s engineering team offers full line layout planning, custom roller design from your profile drawings, and voltage/frequency adaptation for any destination market—explore the full machine range to see how a one-stop approach simplifies both procurement and long-term maintenance.
| चयन मानदंड | प्रवेश-स्तर | मध्यम श्रेणी | उच्च-मात्रा |
|---|---|---|---|
| फॉर्मिंग गति | 6–10 मीटर/मिनट | 12–18 m/min | 20+ m/min |
| रोलर स्टैंड | 10–14 | 14–18 | 18–22 |
| पंचिंग सिस्टम | Hydraulic, fixed die | Hydraulic, interchangeable dies | Servo press, multi-die turret |
| नियंत्रण प्रणाली | Basic PLC + counter | PLC + HMI टचस्क्रीन | PLC + HMI + encoder feedback |
| के लिए सर्वोत्तम | Small workshops, startups | Mid-size fabricators, distributors | Large-scale fence manufacturers |
Use this table as a starting framework, then refine your specification through detailed technical discussion with your supplier. Asking the right questions early—about roller material, spare die availability, PLC programming flexibility, and after-sales spare parts logistics—prevents costly surprises after installation.
उत्पादन लाइन लेआउट और कार्यप्रवाह अनुकूलन
Designing an efficient production line layout around your fence post roll forming machine is as important as the machine specification itself. A well-planned floor layout minimizes material handling, reduces operator fatigue, and supports continuous production with minimal downtime between coil changes.
The standard inline workflow follows a linear sequence: decoiler → leveling → pre-punch (if applicable) → roll forming → post-punch (if applicable) → flying shear cut-off → run-out table → manual or automatic stacking. For a typical peach post line producing 2.0–3.0 m posts at 12 m/min, plan for a total line length of approximately 18–25 meters, including coil staging space at the infeed end and bundled post storage at the outfeed end. Floor-level installation is standard; pit foundations are generally unnecessary for fence post machines unless the decoiler is oversized.
Coil changeover time is a frequently overlooked productivity factor. Machines equipped with a hydraulic decoiler with coil car can reduce changeover to under 5 minutes, compared with 15–20 minutes for manual loading with an overhead crane. For operations running multiple shifts, this difference adds up to significant annual output gains. Similarly, investing in an automatic stacker at the run-out end eliminates the need for a dedicated operator to collect and bundle finished posts, freeing labor for quality inspection and packaging tasks. When planning your line, consult with SUNWAY’s FAQ section for answers to common layout and configuration questions, or request a custom line drawing from the engineering team.
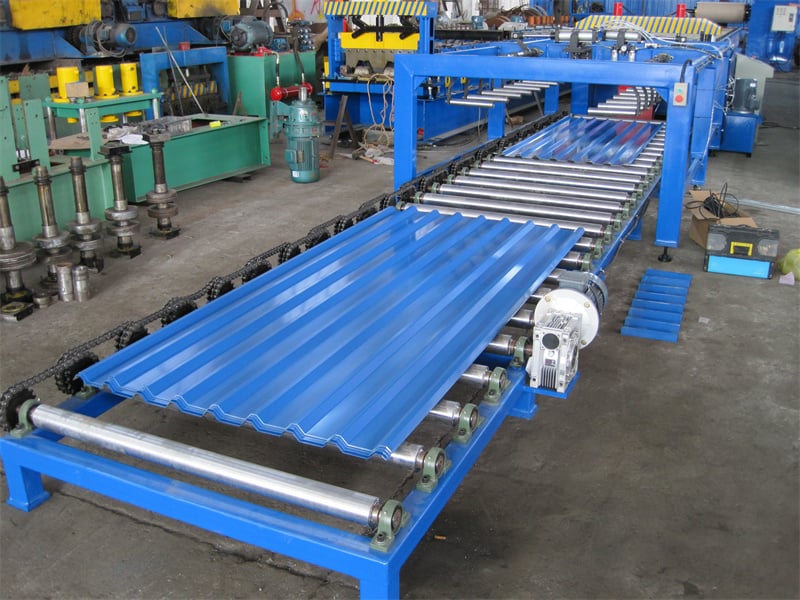
अक्सर पूछे जाने वाले प्रश्न: फेंस पोस्ट रोल फॉर्मिंग मशीन
फेंस पोस्ट रोल फॉर्मिंग मशीन कौन-से प्रोफ़ाइल बना सकती है?
A fence post roll forming machine can produce peach-shaped posts, Y-shaped (star picket) posts, T-posts, and various custom fence column profiles depending on the roller tooling installed. Changing profiles typically requires swapping roller cassettes and updating the PLC program.
वायर मेश पोस्ट मशीन की सामान्य फॉर्मिंग गति क्या है?
Most wire mesh post machine lines operate at 8–18 m/min for standard peach post and Y post profiles. Actual speed depends on material thickness, profile complexity, punching density, and the number of forming stations.
पीच पोस्ट फॉर्मिंग मशीन में किस रोलर सामग्री का उपयोग किया जाता है?
High-quality peach post forming machine rollers are typically made from Cr12MoV or GCr15 alloy steel, hardened to HRC 58–62 and precision-machined on CNC lathes for long service life and consistent profile accuracy.
क्या एक मशीन पीच पोस्ट और Y पोस्ट दोनों बना सकती है?
Yes, some machines support interchangeable quick-change roller cassettes that allow switching between peach post and Y post production on a single frame. Confirm this capability with your supplier during the quotation stage.
ये मशीनें किस स्टील मोटाई को संभाल सकती हैं?
Standard fence post roll forming machines process steel strip from 1.0 mm to 2.5 mm thick. Heavier gauges may require additional forming stations and higher-capacity hydraulic systems.
क्या SUNWAY संपूर्ण फेंस पोस्ट उत्पादन लाइन समाधान प्रदान करता है?
Yes, SUNWAY offers one-stop production line solutions including decoiler, leveler, punching station, roll forming machine, cut-off system, run-out table, and optional auto stacker—along with installation guidance, operator training, spare parts supply, and lifetime technical support.
सामान्य लीड टाइम और शिपिंग व्यवस्था क्या है?
Lead time for a standard fence post roll forming machine is typically 45–60 days from order confirmation. SUNWAY provides professional containerized shipping with stretch film, waterproof cloth, and steel frame packaging, plus complete export documentation.
परिवर्तन-लेख:
- Comprehensive coverage of peach post and Y post cross-section characteristics and forming differences
- Detailed explanation of inline punching and bending synchronization methods
- Surface treatment compatibility analysis for hot-dip galvanizing, powder coating, and PVC dip coating
- Machine selection framework with entry-level to high-volume specification comparison
- Production line layout and workflow optimization guidance
Next review triggers: New fence post profile trends in global markets, updates to forming speed or punching technology, changes in surface treatment standards, new machine models launched by SUNWAY, shipping or trade policy changes affecting key export markets





