
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

Elevator guide rail making machines are used to produce the guide rails used in elevator systems. The guide rails act as tracks to precisely guide the elevator car up and down the hoistway.
एलिवेटर गाइड रेल बनाने वाली मशीन का मुख्य विवरण
- Equipment type: Roll forming machine
- Materials: Steel coils
- Forming methods: Roll forming
- Outputs: Formed metal rails
- Industrial applications: Elevator systems, material handling systems
एलिवेटर गाइड रेल बनाने वाली मशीन गाइड
| प्रकार | विवरण |
|---|---|
| रोल फॉर्मिंग मशीन | Continuously forms metal coils into customized rail profiles by progressively bending sheet through series of roller dies |
| डिकॉयलर | धातु कॉइल स्ट्रिप को रोल फॉर्मर में फीड करता है |
| Pre-cutting shears | Trims sheets to required coil width before forming |
| रोल फॉर्मिंग स्टैंड | Successive stands with roller dies to incrementally bend metal strip |
| Post-cutting shears | Cuts formed rails to required lengths |
| Supporting equipment | PLC control, hydraulics, gearboxes, instruments |
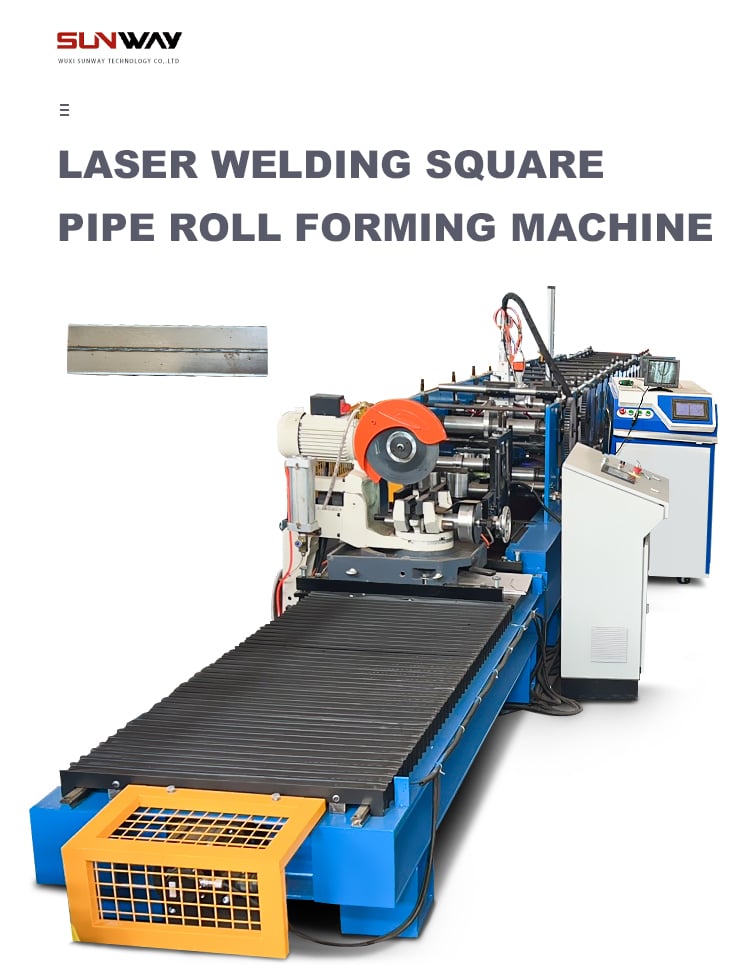
एलिवेटर गाइड रेल बनाने वाली मशीन की कार्य प्रक्रिया
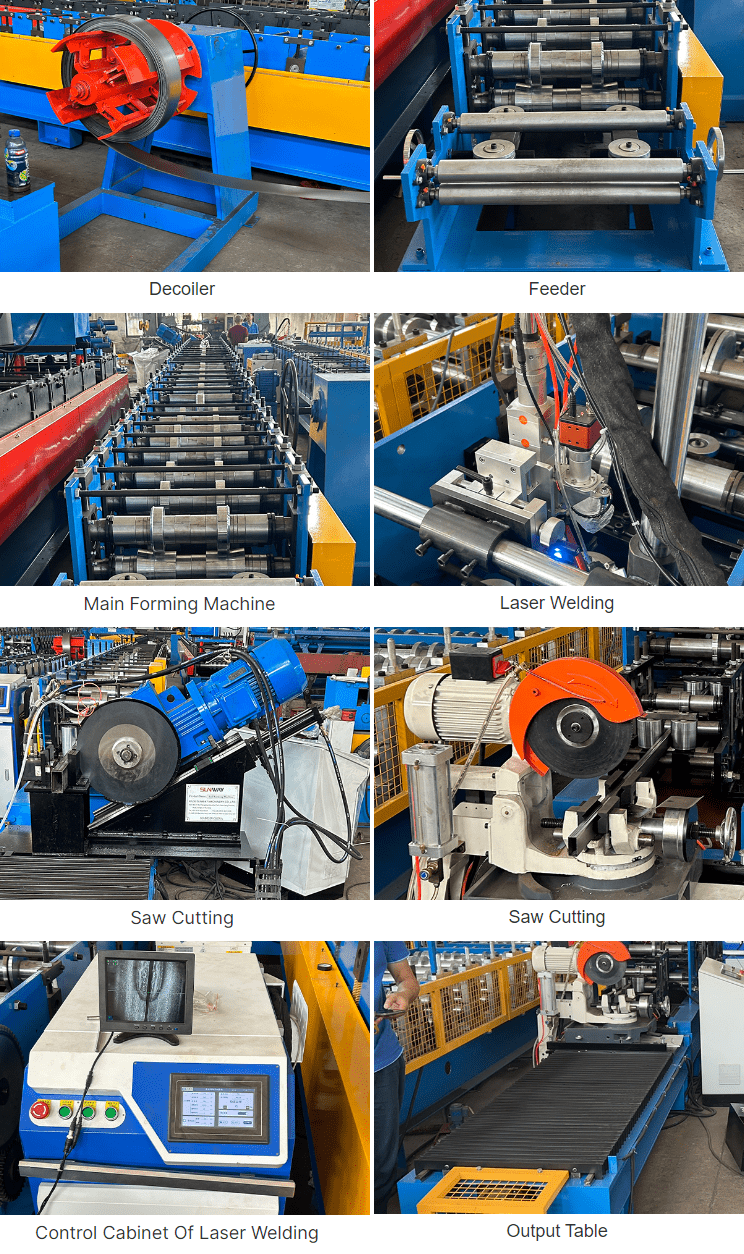
यह एलिवेटर गाइड रेल बनाने की मशीन works by roll forming process. The input raw material is steel coil loaded on an uncoiler. The coil passes through pre-cutting shears where it is trimmed to the specified width required for the rail profile.
The trimmed metal strip then proceeds through successive roller dies mounted on forming stands. Each set of rolls progressively bends the sheet incrementally to gradually form the desired rail configuration.
The fully formed rail profile exits the last stand of rolls and is cut to desired lengths by post-forming shears. The finished cut rails are collected on the outfeed tables.
पैरामीटर
| पैरामीटर | विवरण |
|---|---|
| सामग्री | Low carbon steel, stainless steel, galvanized steel coils |
| मोटाई | 1-3 mm typically |
| चौड़ाई | 50-100 mm typically |
| लंबाई | Up to 6000 mm |
| गति | 10-15 m/min |
| सहनशीलताएँ | +/- 0.02 mm |
| सतह फिनिश | <0.5 microns |
सामग्री फीडिंग
- Decoiler accommodates up to 5 mt coils
- Decoiler equipped with precision feed rollers
- Width is trimmed by pre-cut shears before forming
- Coil is fed continuously at constant speed into roll forming stands
प्रोफ़ाइल निर्माण
- Gradually formed by set of rolls bending sheet incrementally
- 6-8 adjustable forming stands with changeable rolls
- Rolls have machined grooves to impart profile shape
- Bottom rolls powered by geared motors and drives
- Top rolls free running and adjustable by hydraulic cylinder
प्रोफ़ाइल डिज़ाइन
- Roll pass design software calculates correct roll groove geometry
- Roll pass simulation validates shape through forming stands
- Design optimized for material type and desired rail configuration
- Rolls CNC machined from D2 steel for hardness and durability
लंबाई कटाई
- Carried out by robust post-forming cutting machine
- Heavy duty cutter with hardened blades shears the formed rails
- Length measurement by precision rotary encoder
- Length tolerance +/- 0.5 mm
- Length range 500 mm to 6000 mm
अनुकूलन
- Forming rolls designed and produced for custom rail dimensions
- Roll changeover in 24 hours enables rapid prototyping
- Profile simulation validates rail shape before machining rolls
- Product development support for unique applications
आपूर्तिकर्ता और मूल्य सीमा
| निर्माता | स्थान | मूल्य सीमा |
|---|---|---|
| Machine Mfg Ltd | चीन | $100,000 – $150,000 |
| Formmasters Inc | यूरोप | $200,000 – $250,000 |
| Rolling Equipments | भारत | $125,000 – $175,000 |
स्थापना आवश्यकताएँ
| पैरामीटर | विवरण |
|---|---|
| स्थान | Indoor shop floor |
| शक्ति | 25-30 kW connection |
| वोल्टेज | 380-440 V AC 3 phase |
| संपीड़ित वायु | Pressure – 6 bar |
| Volume – 10 CFM | |
| बेस फ्रेम | Load bearing concrete floor |
| लाइटिंग | 500 lux intensity |
| जलवायु नियंत्रण | Ambient temp 15-35°C |
| Humidity: 20%-60% RH |
-
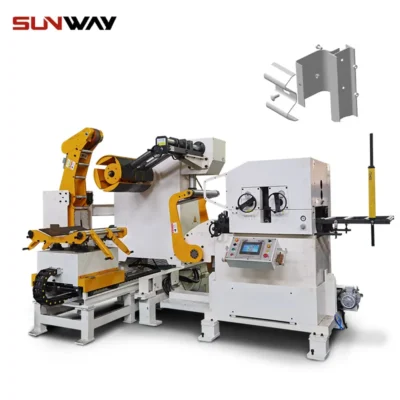 हाईवे गार्डरेल एंड टर्मिनल फॉर्मिंग मशीन अधिक पढ़ें
-
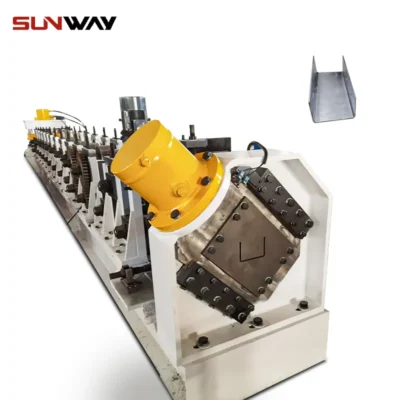 हाईवे U/C पोस्ट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
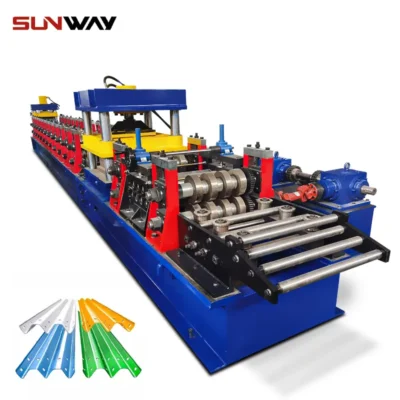 2 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
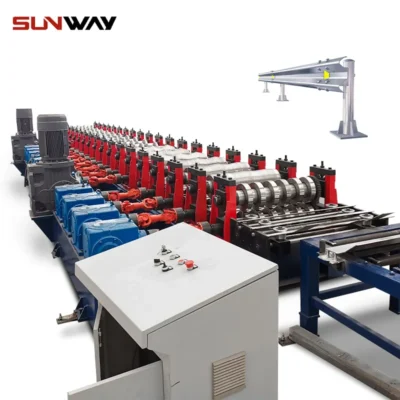 3 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
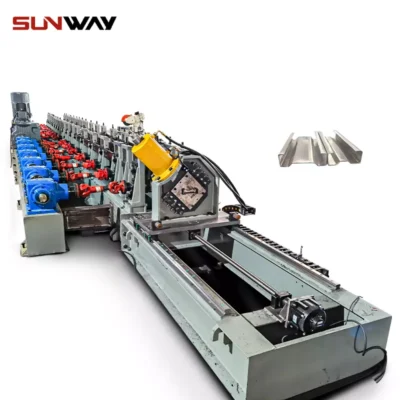 ऑटो साइज चेंजेबल सिग्मा पर्लिन रोल फॉर्मिंग मशीन अधिक पढ़ें
-
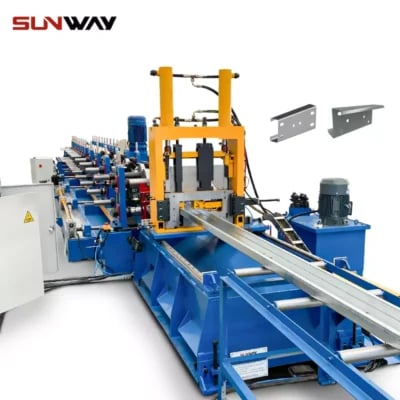 स्वचालित आकार बदलने योग्य C Z पर्लिन रोल फॉर्मिंग मशीन अधिक पढ़ें
-
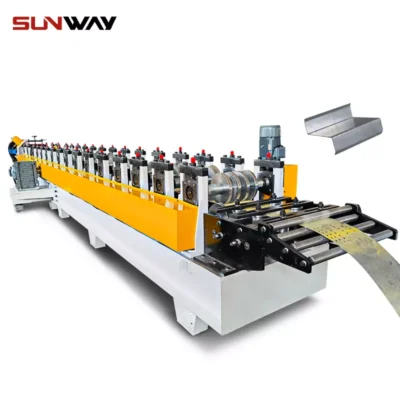 स्वचालित आकार बदलने योग्य Z पर्लिन रोल फॉर्मिंग मशीन अधिक पढ़ें
-
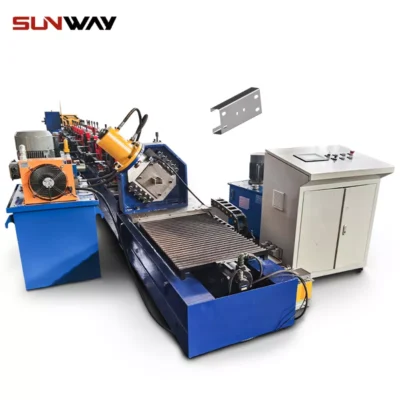 स्वचालित आकार बदलने योग्य C U पर्लिन रोल फॉर्मिंग मशीन अधिक पढ़ें
-
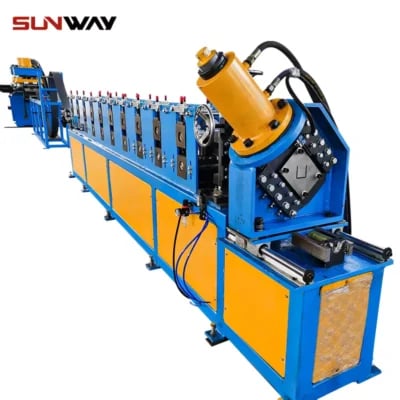 इलेक्ट्रिकल कैबिनेट फ्रेम रोल फॉर्मिंग मशीन अधिक पढ़ें
संचालन
- Minimum 3 operators per shift
- One operator at decoiler & feeding
- One operator to manage roll tooling
- One operator at post-forming cutting station
- Centralized PLC panel for controlling parameters
- HMI touchscreen for monitoring and datalogging
रखरखाव
| कार्य | आवृत्ति | विधि |
|---|---|---|
| रोल निरीक्षण | दैनिक | Visual inspection for damage or wear |
| Roll lubrication | साप्ताहिक | Grease all bearings |
| हाइड्रोलिक तेल | मासिक | Check level and top up |
| वार्षिक | Replace oil | |
| प्रतिस्थापन पुर्जे | आवश्यकतानुसार | Spare backup rolls, blades, sensors, motors recommended |
| Roll recalibration | हर 2 वर्ष में | Re-grind roll grooves if wear exceeds 0.15mm |
आपूर्तिकर्ता का चयन
| पैरामीटर | महत्व |
|---|---|
| अनुभव | उच्च |
| Roll Design expertise | उच्च |
| निर्माण गुणवत्ता | उच्च |
| Roll quality | उच्च |
| फॉर्मिंग सटीकता | उच्च |
| उत्पादन दर | मध्यम |
| स्वचालन स्तर | मध्यम |
| सेवा सहायता | उच्च |
| लीड टाइम | कम |
| मूल्य | कम |
फायदे और नुकसान
| फायदे | नुकसान |
|---|---|
| Continuous and efficient forming process | उच्च प्रारंभिक टूलिंग निवेश |
| Fast set up between batches | Requires heavy baseframe |
| Compact layout compared to press brakes | सीमित मोटाई और चौड़ाई क्षमता |
| Consistent tolerance control | नियमित रखरखाव आवश्यक |
| Adaptable to custom profiles | Roll damage can interrupt production |
प्रेस ब्रेक की तुलना में लाभ
- No sheet marking or scratches from dies
- Higher production rate for mass production
- Lower tooling cost per piece
- Continuous forming action vs cyclic bending
- Uniform material properties along length
प्रेस ब्रेक की तुलना में सीमाएँ
- अधिक प्रारंभिक टूलिंग लागत
- सीमित मोटाई क्षमता
- Cannot form complex 3D shapes
- Certain asymmetric shapes difficult to form
- Longer tooling lead time
सामान्य अनुप्रयोग
- Elevator guide rails
- Drawer rails, slide ways
- Conveyor side rails
- Crane wheel tracks
- Automatic parking pallets
- Material handling tracks
- Industrial storage racks
अक्सर पूछे जाने वाले प्रश्न
Q: What thickness of steel can these machines handle?
A: Typically 1 mm to 3 mm thickness is possible. Maximum capacity reaches up to 4 mm steel grades.
प्रश्न: उत्पादन दर कितनी तेज़ है?
A: 10 – 15 meters per minute linear speed is standard. Some high speed machines achieve up to 30 m/min production rate.
Q: What length of rails can be produced?
A: Standard length capacity is 6 meters. Custom built machines can produce up to 12 meter rails.
Q: What accuracy and surface quality is possible?
A: Roll formed parts can achieve tolerances of +/- 0.02 mm and surface finish around 0.5 microns.
Q: What aftersales support is provided?
A: Installation and commissioning help, operator training, warranty on parts, field service for repairs, and phone/email tech support.
रोल फॉर्मिंग के बारे में अधिक जानें
अक्सर पूछे जाने वाले प्रश्न (FAQ)
1) What standards should elevator guide rails produced by a roll forming machine comply with?
- For passenger and freight elevators, rails and their dimensions typically reference ISO 7465 and EN 81-20/50 for safety and performance. Verify profile geometry, straightness, surface roughness, and hole/slot tolerances against the project’s specification and applicable local codes.
2) How do I ensure rail straightness and twist are within tolerance after roll forming?
- Use inline laser straightness gauges and post-process roller straighteners. Control coil flatness via precision leveling, maintain consistent roll gaps, and document thermal stabilization times before QA checks.
3) Can one Elevator Guide Rail Making Machine handle both T-rail and custom C/U profiles?
- Yes, with modular roll tooling and pass-design cassettes. However, changeover time and achievable tolerances depend on stand adjustability, spindle rigidity, and whether the line supports motorized roll positioning and recipe presets.
4) What are common causes of edge waviness and how can they be corrected?
- Causes: uneven roll gap, residual coil crown, inadequate entry guide alignment, or overforming at early passes. Fixes: re-balance pass reductions, re-level the coil, reset entry guides, and adjust roll diameters/overbend compensation in mid passes.
5) What level of automation is recommended for consistent elevator rail quality?
- PLC/servo control with encoder feedback, automatic length measurement, closed-loop speed sync from decoiler to shear, and optional vision/laser inspection. For high-end lines, add MES/SCADA connectivity for traceability and SPC charts.
2025 उद्योग रुझान
- AI-assisted pass setup: digital twins predict springback; changeover scrap reduced to 1–2%.
- Inline metrology: multi-axis laser systems verify straightness, twist, and hole pitch at full speed.
- Sustainability: IE5 motors and regenerative drives cut energy to sub-85 kWh/ton; EPD-ready data logging.
- Material evolution: increased use of zinc–magnesium coated steels for corrosion resistance in humid shafts.
- Compliance-by-design: recipe locks tied to ISO 7465 geometry and EN 81-20 safety checks.
2025 Performance Benchmarks for Elevator Guide Rail Making Machines
| मीट्रिक | 2022 सामान्य | 2025 में सर्वश्रेष्ठ श्रेणी | टिप्पणियाँ |
|---|---|---|---|
| लाइन गति (m/min) | 10–15 | 20–30 | Profile dependent; flying shear with servo control |
| लंबाई सहिष्णुता (mm) | ±0.5 | ±0.2–0.3 | With high-res encoders and thermal compensation |
| Straightness (mm per 5 m) | ≤1.0 | ≤0.5 | Inline laser straightness control |
| Twist (deg per m) | ≤0.2 | ≤0.1 | Measured via 3D vision/laser triangulation |
| चेंजओवर समय (min) | 120–240 | 45–90 | Quick-change cassettes + motorized roll positioning |
| ऊर्जा उपयोग (kWh/ton) | 110–140 | 75–90 | IE4/IE5 motors, regenerative braking |
| सेटअप स्क्रैप (%) | 3–5 | 1–2 | AI pass prediction + SPC |
प्रामाणिक संदर्भ:
- ISO 7465: Lift guide rails and fishplates: https://www.iso.org/standard/14673.html
- EN 81-20/50 Safety rules for the construction and installation of lifts: https://standards.cen.eu
- World Steel Association—metallic coatings: https://worldsteel.org
- The Fabricator—roll forming process control: https://www.thefabricator.com
- ISO 50001 ऊर्जा प्रबंधन प्रणालियाँ: https://www.iso.org/standard/69426.html
नवीनतम अनुसंधान मामले
Case Study 1: AI Pass-Design Optimization for Elevator T-Rails (2025)
Background: An OEM producing 5–6 m elevator T-rails saw variable straightness (up to 0.9 mm/5 m) after coil lot changes.
Solution: Implemented a digital twin of the roll stands with material models calibrated from tensile/YS data; added inline 3D laser straightness and twist sensors and automatic roll-gap presets.
Results: Straightness improved to 0.42 mm/5 m (P95), twist to 0.08°/m; setup scrap dropped from 3.8% to 1.6%; OEE increased by 11%.
Case Study 2: ZM-Coated Stainless Alternative for Humid Hoistways (2024)
Background: Retrofits in tropical climates required improved corrosion performance without switching fully to stainless due to cost.
Solution: Switched from GI to ZM-coated low-carbon steel with optimized pass schedule to manage coating hardness; introduced post-form anti-corrosion seal and controlled handling to protect edges.
Results: Salt spray (ISO 9227) time-to-red-rust >2× vs GI; no speed penalty; total cost reduced 14% compared with 304 stainless option while meeting EN 81-20 requirements.
विशेषज्ञों की राय
- Dr. Meera Venkataraman, Head of Forming Processes, Fraunhofer IWU
Viewpoint: “For elevator guide rails, roll stand rigidity and controlled pass reduction are decisive. Pairing digital twins with inline laser metrology is now the fastest route to sub-0.5 mm straightness over 5 meters.” - Juan Carlos Prieto, Global Elevator Supply Chain Director, Schindler Group
Viewpoint: “Traceability matters. Linking coil heat, pass recipe, and QA scans to each rail segment shortens approvals with major builders and supports EPD submissions.” - Alessia Romano, Product Manager, FICEP Rollforming
Viewpoint: “IE5 drives and regenerative braking aren’t just green—they stabilize torque at low speeds, improving cut-length accuracy and reducing rework on premium rails.”
व्यावहारिक उपकरण/संसाधन
- ISO 7465: Lift guide rails and fishplates standard: https://www.iso.org/standard/14673.html
- EN 81-20/50 safety standards overview: https://standards.cen.eu
- NIST Digital Metrology resources (inline dimensional measurement): https://www.nist.gov
- The Fabricator—roll forming design guides: https://www.thefabricator.com
- World Steel Association—coatings/corrosion insights: https://worldsteel.org
- SPC software for shop-floor QA (q-DAS/Hexagon): https://www.hexagonmi.com
- Vision/laser metrology vendors (Cognex, Keyence): https://www.cognex.com | https://www.keyence.com
- ऊर्जा प्रबंधन ढाँचा (ISO 50001): https://www.iso.org/standard/69426.html
अंतिम अपडेट: 2025-10-20
परिवर्तन-लेख: Added 5 focused FAQs; inserted 2025 benchmarks table and trend insights; provided two recent case studies; included expert viewpoints; compiled practical tools/resources with authoritative links
अगली समीक्षा तिथि और ट्रिगर: 2026-04-15 or earlier if EN/ISO standards update, inline metrology specs improve by >20%, or new corrosion-resistant substrates are adopted in elevator rail production





