
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

का अवलोकन CZ पर्लिन रोल फॉर्मिंग मशीनें
CZ Purlin roll forming machines are used to continuously bend metal coils into customized C and Z shaped purlins and girts for the construction industry. Purlins provide structural framing and support for roofing and siding materials.
CZ पर्लिन क्या है?
C and Z purlins have a unique cross-sectional shape that provides strength and rigidity from the angled web. The flanges allow easy attachment to roofing and walls. Common materials are galvanized steel, aluminum, and stainless steel.
CZ पर्लिनों के उपयोग के लाभ
- Lightweight but load-bearing for long roof spans
- Easy to install, requiring simple bolted connections
- Angled web provides torsional rigidity under wind or seismic loads
- Variety of sizes suit residential, commercial and industrial applications
- Galvanizing offers corrosion resistance for low maintenance
कार्य सिद्धांत CZ Purlin Roll Forming
- Coiled metal sheet or strip is unrolled and fed into the mill
- Forming rollers progressively cold-form the strip into C or Z shape through a series of bending steps
- Cutoff knives slice formed sections to specified lengths
- Formed purlins are collected on the output side for bundling and shipping
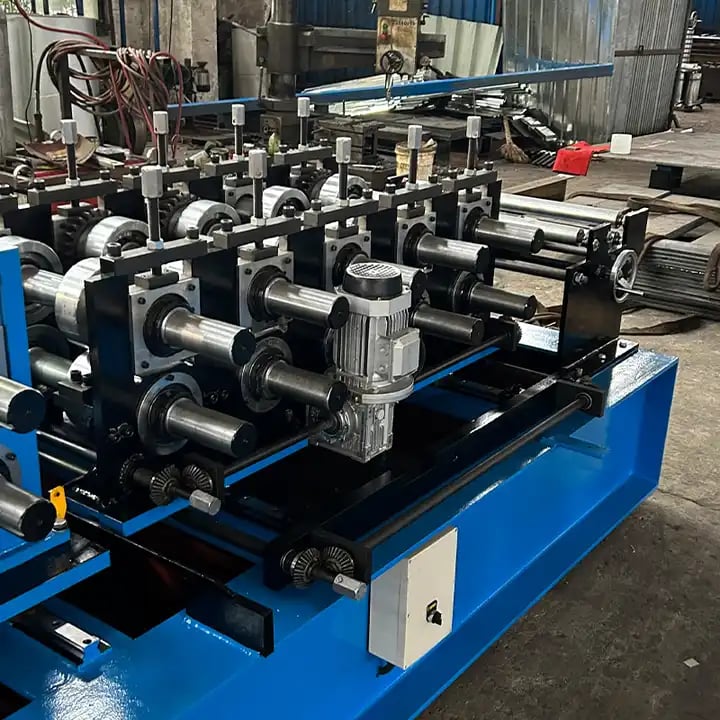
CZ Purlin Roll Forming Equipment के प्रकार
| उपकरण प्रकार | विवरण | उत्पादन दर |
|---|---|---|
| मैनुअल लाइनें | Basic manually-operated machines for small scale producers | Around 10 m/min |
| स्वचालित लाइनें | Feature powered unwinding, feeding and cutting for high volume efficiency | 35 m/min तक |
| अनुकूलित लाइनें | Designed to make specialized purlin sizes and thicknesses | Varies based on need |
CZ Purlin Roll Forming की कार्य प्रक्रिया
The CZ purlin production line forms the raw metal strip from coiled stock through a series of progressive bending and forming stages into the final C or Z-shaped profile.
Key processes include:
- सामग्री फीडिंग: Automated powered unwinding of coiled sheet metal into the mill
- फॉर्मिंग: Precision roller dies continuously cold form the strip through multiple bending steps
- डिज़ाइन और आकार निर्धारण: Roller dies customized to produce exact purlin dimensions
- कटिंग: Automated cutoff knives slice formed CZ sections to fixed lengths
- अनुकूलन: Lines can be adapted to make special purlin sizes
Forming rollers are machined to precision tolerances for accurate profile dimensions and straightness. The forming process induces work hardening into the metal for a strong finished purlin product.
CZ Purlin Roll Forming में सामग्री फीडिंग
| विशेषता | विवरण |
|---|---|
| Stock Material | Hot-dip galvanized steel coil / Aluminum coils |
| चौड़ाई सीमा | 50mm to 750mm |
| मोटाई सीमा | 0.4mm से 2.0mm |
| कॉइल I.D. | 508mm (standard) |
| Coil O.D. | 1200mm to 1500mm (standard) |
| डिकॉइलर क्षमता | 5 tons to 20 tons |
| Feeder Type | Powered mechanical, servo motor, hydraulic |
| फीड गति | 35 m/min तक |
Galvanized steel is commonly used, along with aluminum and stainless steels in some cases. A variety of stock coil widths, thicknesses, diameters can be accommodated. Powered decoilers and programmable feed systems provide reliable, high-speed material input.
डिज़ाइन और आकार निर्धारण क्षमताएँ
CZ purlin roll forming lines can produce different designs, sizes, lengths and material gauges.
| पैरामीटर | क्षमताएँ |
|---|---|
| प्रोफ़ाइल आकार | C or Z shape purlins |
| ऊँचाई | 50mm to 400mm |
| फ्लैंज की चौड़ाई | 30mm to 80mm |
| Lip Height | 6mm to 20mm |
| सामग्री की मोटाई | 0.4mm से 2.0mm |
| Purlin Lengths | 2m to 15m programmable |
Through precision tooling, various purlin heights, flange widths, material gauges can be formed in standard or custom dimensions. Cutoff knives slice purlins from 2 to 15 meter fixed lengths.
-
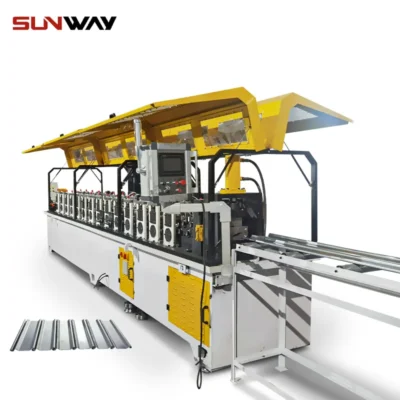 रोलिंग शटर स्लैट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
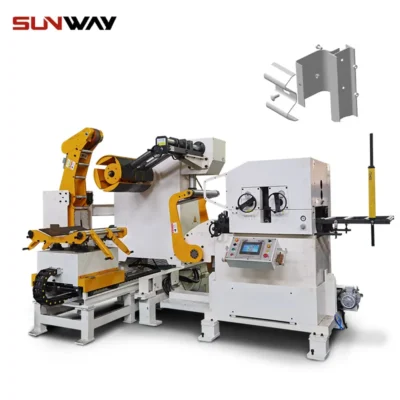 हाईवे गार्डरेल एंड टर्मिनल फॉर्मिंग मशीन अधिक पढ़ें
-
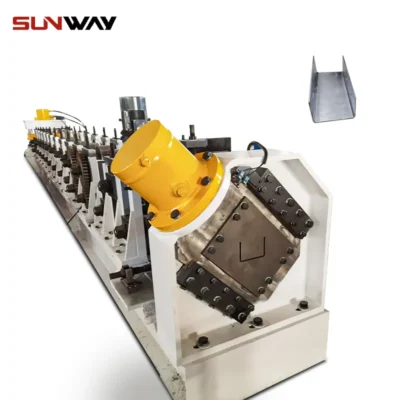 हाईवे U/C पोस्ट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 2 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 3 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 इलेक्ट्रिकल कैबिनेट फ्रेम रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 Din रेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 दो वेव हाईवे गार्डरेल मशीन अधिक पढ़ें
-
 तीन वेव हाईवे गार्डरेल मशीन अधिक पढ़ें
Roll Forming Lines में कटिंग संचालन
| विशेषता | विवरण |
|---|---|
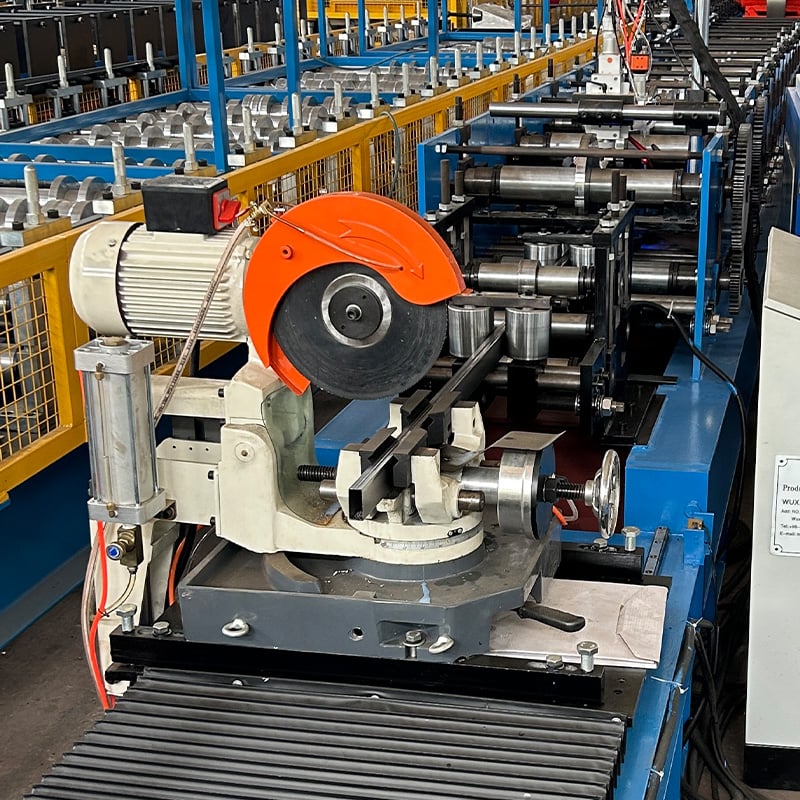
| Cutting Principle | Pneumatically actuated shear knives |
| कटिंग सहनशीलता | +/- 1.0mm |
| Minimum Cut Length | 2000mm |
| Maximum Cut Length | 15000mm |
| Section Length Indicator | Digital meter counter |
| Section Length Tolerance | +/- 1.0mm |
| Scrap Collection | Chute below shear station |
Purlin lengths are set by precision ballscrew mechanisms to position the pneumatic shears. A high tolerance cutting operation ensures each purlin is within +/- 1mm of the exact programmed length.
का अनुकूलन CZ Purlin Roll Forming Lines
Roll forming lines can be customized to produce specialized purlin and girt sections based on customer requirements:
Possible Customizations
- Non-standard purlin and girt dimensions
- Special material types and thicknesses
- Custom coatings and finishes
- Integration with packing equipment
- Non-standard power supplies
- Motor control hardware upgrades
- UL/CE compliance packages
Custom lines enable small scale producers to make specialized products for niche markets cost effectively.
स्थापना, संचालन और रखरखाव
| गतिविधि | विवरण | आवृत्ति |
|---|---|---|
| स्थापना | Performed by supplier technicians onsite. Requires flat, level floor and provision of utilities. | One time |
| संचालन | Machine operators feed coils, set dimensions, monitor production. Basic mechanical aptitude is needed. | Daily production runs |
| रखरखाव | Includes lubrication, inspection, spare parts replacement and recalibration of components. | As per supplied manual |
Proper installation forms the base for smooth functioning. Routine maintenance helps maximize production uptime and output quality.
सही CZ Purlin Roll Forming Machine का चयन कैसे करें
Key considerations when selecting a roll forming machine:
- Type and volume demand
- Product dimensions, specifications
- Raw material type and thickness
- आवश्यक स्वचालन का स्तर
- Production efficiency targets
- बजट सीमाएँ
- Options for future expansion
- Supplier reputation and service
Accurately estimating key requirements will help identify the ideal machine specifications and avoid overpaying. Leading manufacturers offer production guidance.
के फायदे और नुकसान CZ पर्लिन रोल फॉर्मिंग मशीनें
| लाभ | सीमाएं |
|---|---|
| Continuous unattended production | Fixed tooling limits profile shapes |
| कॉइल इनपुट से उच्च सामग्री उपज | Significant initial capital expenditure |
| Consistent quality end product | Complex for extremely thick metals |
| Versatile production capacities | Narrow sheets under 50mm challenging |
| Simple bolt-together field installation | Maximum 15 m lengths without secondary bending |
When correctly specified, CZ purlin roll forming lines offer efficient, automated production of roofing components with quick payback on investment.
अक्सर पूछे जाने वाले प्रश्न
Q: What thickness of sheets can be formed on these machines?
A: Standard machines accommodate metal thickness from 0.4mm up to 2mm. Special heavy gauge lines are available for plates over 2mm.
Q: Can other profiles be produced besides C and Z?
A: Machine tooling is currently limited to CZ purlins and girts. Custom roll dies would be needed for different profiles.
Q: How long is supplier training and commissioning?
A: Standard lines require just 2-3 days at the factory. For customized equipment, specialists may remain 5-7 days for full transfer.
प्र: सामान्य उत्पादन दर क्या है?
A: 10 – 35 meters per minute based on automation level and power. Faster cycles are possible with accumulator cutoff.
Q: What factors affect price most?
A: Key drivers are production speed, level of automation, customization needs, and ancillary equipment integration.
रोल फॉर्मिंग के बारे में अधिक जानें
अतिरिक्त अक्सर पूछे जाने वाले प्रश्न (FAQ)
1) Can one line switch between C and Z profiles without changing the entire tooling set?
Yes. Modern CZ Purlin Roll Forming Machines use quick-change cassettes or programmable punching/roll stands that rotate or shift to convert from C to Z in 3–15 minutes, minimizing downtime.
2) What tolerances are achievable for height, flange, and length on high-end lines?
With servo feeding and encoder feedback, typical dimensional tolerances are ±0.3–0.5 mm on web height/flange width, ±0.2–0.4 mm on hole positions (servo punching), and ±0.5–1.0 mm on cut length.
3) Which steels are most common for high-strength purlins, and what thickness range is typical?
Galvanized coil in S350–S550 grade (ASTM A653/A1008 equivalents) is common. Thickness usually ranges 1.2–3.0 mm for structural CZ purlins; lighter gauges (0.8–1.0 mm) are used for secondary members.
4) How is hole punching handled for bolted connections?
Inline hydraulic or servo-electric punching units index hole patterns (round, slotted, service openings) before forming. CAD/CAM recipes can be loaded to vary hole pitch per project.
5) What factors most affect straightness and twist in long purlins?
Coil crown/flatness, pass progression, roll gap setup, entry guide alignment, and cutoff impact. Using a leveler, SPC checks, and ramped shear profiles reduces bow, camber, and twist.
2025 उद्योग रुझान: CZ पर्लिन रोल फॉर्मिंग मशीनें
- Servo-electric actuation replaces hydraulics on punching and shearing for cleaner shops, precise repeatability, and energy savings.
- On-the-fly C↔Z changeover with digital recipes shortens SMED to under 10 minutes on premium lines.
- Sustainability driver: wider adoption of galvanized steel with higher recycled content; energy monitoring at the machine level.
- Integrated quality analytics: machine vision measures web height, flange, and lip during production; data streams to MES via OPC UA/MQTT.
- Regional code shifts (wind/seismic) push higher-strength grades (S450–S550) and closed-lip designs for improved torsional stiffness.
प्रदर्शन और अपनाने के मानक (2024 बनाम 2025)
| मीट्रिक | २०२४ सामान्य | 2025 सर्वश्रेष्ठ-इन-क्लास | लाभ | स्रोत/टिप्पणियां |
|---|---|---|---|---|
| C↔Z चेंजओवर समय | 25–45 मिनट | 3–10 मिनट | +OEE, कम डाउनटाइम | SMED + कैसेट टूलिंग |
| लाइन गति (1.5–2.0 mm S350) | 20–35 m/min | 35–50 m/min | थ्रूपुट में वृद्धि | OEM कैटलॉग; The Fabricator |
| लंबाई की सटीकता (±) | 1.0–1.5 मिमी | 0.5–1.0 mm | कम पुनः-कटिंग | सर्वो फ्लाइंग शीयर + एन्कोडर |
| छेद की स्थिति की सटीकता (±) | 0.6–1.0 mm | 0.2–0.4 मिमी | तेज़ असेंबली | सर्वो-इलेक्ट्रिक पंच |
| ऊर्जा उपयोग (kWh/ton) | 125–170 | 95–130 | 15–25% बचत | DOE AMO मार्गदर्शन |
| स्क्रैप दर | 2.5–4.0% | 1.0–2.0% | सामग्री की बचत | In-line vision + SPC |
संदर्भ और स्रोत:
- U.S. DOE उन्नत विनिर्माण: https://www.energy.gov/eere/amo
- द फैब्रिकेटर (रोल फॉर्मिंग अंतर्दृष्टियाँ): https://www.thefabricator.com
- AISI/Steel Framing Industry resources: https://www.steel.org
- OPC Foundation (OPC UA): https://opcfoundation.org
नवीनतम अनुसंधान मामले
Case Study 1: Rapid C↔Z Changeover with Servo Punching (2025)
Background: A mid-size building products OEM faced frequent profile changes, causing 35–40 minutes of downtime per shift.
Solution: Upgraded to cassette-style roll tooling, servo-electric punching with barcode-loaded recipes, and OPC UA integration to MES.
Results: Average changeover fell to 8 minutes; first-pass yield improved from 97.9% to 99.2%; scrap reduced from 3.2% to 1.6%; annualized savings ≈ $180k.
Case Study 2: High-Strength S550 Purlins for Wind Zones (2024)
Background: Contractor serving coastal projects needed longer spans with lighter members while meeting new wind uplift codes.
Solution: Implemented S550 galvanized coil with closed-lip Z-purlin design; added precision leveler and camera-based straightness monitoring.
Results: Member mass reduced 11% per linear meter; deflection under service load decreased 7%; installation time per bay dropped 9% due to hole accuracy.
विशेषज्ञों की राय
- डॉ. Michael De Moor, मैकेनिकल इंजीनियरिंग के प्रोफेसर, KU Leuven
Viewpoint: “For S500+ steels, pass design and roll surface finish are critical—micro-cracking at the lip starts when radii violate material bend limits.”
स्रोत: https://www.kuleuven.be - Sara Kim, उत्पाद प्रबंधक, The Bradbury Group
Viewpoint: “Servo-electric punching has become the default for CZ lines in 2025—cleaner operation, longer tool life, and superior hole repeatability versus hydraulics.”
स्रोत: https://bradburygroup.com - Jorge Alvarez, Structural Engineer, AISI Committee Contributor
Viewpoint: “Designers increasingly specify higher-grade Z sections to control lateral-torsional buckling; accurate hole placement directly affects diaphragm behavior.”
स्रोत: https://www.steel.org
व्यावहारिक उपकरण/संसाधन
- मानक और डिज़ाइन
- AISI S100 कोल्ड-फॉर्म्ड स्टील विनिर्देश: https://www.steel.org
- Eurocode 3 (EN 1993) guidance: https://eurocodes.jrc.ec.europa.eu
- प्रक्रिया अनुकूलन
- NIST विनिर्माण संसाधन: https://www.nist.gov/manufacturing
- प्रिसिजन मेटलफॉर्मिंग एसोसिएशन (PMA): https://www.pma.org
- Industrial connectivity and analytics
- OPC Foundation (OPC UA): https://opcfoundation.org
- Siemens Industrial Edge/MindSphere: https://www.siemens.com
- Rockwell FactoryTalk Analytics: https://www.rockwellautomation.com
- OEMs and technical insights
- द ब्रैडबरी ग्रुप: https://bradburygroup.com
- Samco Machinery: https://www.samco-machinery.com
- Dallan S.p.A.: https://www.dallan.com
- Formtek: https://www.formtekgroup.com
- सामग्री और कोटिंग संबंधी मार्गदर्शन
- Galvanized coatings (A653): https://www.astm.org
- Aluminum Association alloy data: https://www.aluminum.org
अंतिम अपडेट: 2025-10-22
परिवर्तन-लेख: Added 5 targeted FAQs; inserted 2025 trends with benchmark table and sources; compiled two recent case studies; included expert viewpoints; listed practical tools/resources aligned with E-E-A-T for CZ purlin roll forming
अगली समीक्षा तिथि और ट्रिगर: 2026-04-22 or earlier if major code updates (AISI/Eurocode), new OEM releases on servo-electric punching, or energy regulations affecting metal forming lines





