
 अंग्रेज़ी
 स्पेनिश
 फ़्रेंच
 बंगाली
 रूसी
 अरबी
 तुर्की

CZ पर्लिन फॉर्मिंग मशीनें हैं रोल फॉर्मिंग उपकरण used to produce C and Z shaped purlins from metal coils. Purlins are structural beams widely used in metal buildings and structures.
CZ पर्लिन क्या है?
A CZ Purlin is a type of structural component used in construction and building applications, particularly in the framing of roofs and walls. Purlins are horizontal beams or members that provide support to the roof covering or wall cladding and help distribute the load of the building’s roof or walls to the main structural frame, such as columns or rafters. They are commonly used in metal building construction.
The term “CZ Purlin” typically refers to two different shapes of purlins:
- C Purlin: A C-shaped purlin is formed like the letter “C” in cross-section, with two horizontal flanges and a vertical web connecting them. C purlins are commonly used for roof framing and wall girts.
- Z Purlin: A Z-shaped purlin is formed like the letter “Z” in cross-section, with a pair of vertical flanges connected by a horizontal web. Z purlins are typically used as roof purlins, and their shape provides added strength and stability compared to C purlins.
CZ Purlins are made from various materials, including steel and aluminum, and they come in different sizes and thicknesses to suit the specific load-bearing requirements of a building’s design. They are essential components in the construction of steel-framed and metal-clad buildings, providing structural support for the roof and walls while also helping to maintain the overall stability and integrity of the structure.
के मुख्य विवरण CZ पर्लिन फॉर्मिंग मशीनें
| मुख्य विवरण | विवरण |
|---|---|
| मशीन प्रकार | सीज़ेड पर्लिन बनाने की मशीन |
| कार्य | To produce C and Z-shaped purlins from flat metal coils |
| Materials Processed | Steel, Aluminum, or other metal materials |
| फॉर्मिंग प्रक्रिया | Roll forming or cold roll forming |
| घटक | Typically includes decoiler, leveling device, punching unit, roll forming unit, cutting unit, and control system |
| Profile Shapes | Produces both C-shaped and Z-shaped purlins |
| कॉइल चौड़ाई | Adjustable, depending on the machine’s design and capacity |
| मोटाई सीमा | Varies based on machine specifications, typically ranging from 1mm to 3mm or more |
| Speed of Production | Varies widely depending on the machine model, ranging from 10 to 30 meters per minute or more |
| कटिंग विधि | Hydraulic or mechanical cutting systems |
| रोल फॉर्मिंग स्टेशन | Multiple sets of roll forming stations for shaping purlins |
| नियंत्रण प्रणाली | PLC (Programmable Logic Controller) for automated operation and precision |
| Size and Dimensions | Various machine sizes available, depending on production requirements |
| शक्ति स्रोत | Electric, typically three-phase power supply |
| सुरक्षा सुविधाएँ | Emergency stop buttons, safety guards, and sensors for worker safety |
| उपयोग | Used in manufacturing and construction industries for producing purlins used in building structures |
| अनुकूलन विकल्प | Machines can be customized based on specific requirements |
| रखरखाव | Regular maintenance and lubrication required for optimal performance |
| Manufacturer Support and Warranty | Usually provided by the machine manufacturer |
कार्य सिद्धांत
- Uncoiler feeds metal strip into machine
- Forming stations progressively shape strip into C or Z profile
- Cutting tool slices beams to required length
- Output table stacks finished purlins
मुख्य घटक
- अनकॉइलिंग यूनिट
- स्ट्रेटनिंग रोल्स
- अक्यूमुलेटर
- Forming stations with top/bottom blades
- हाइड्रॉलिक सिस्टम
- Cutting tool
- कंट्रोल पैनल
के प्रकार
CZ पर्लिन फॉर्मिंग मशीनें| मशीन प्रकार | विवरण |
|---|---|
| Manual CZ Machine | Basic model with manual adjustment for size changes |
| Automatic CZ Machine | Fully automatic adjustment of forming parameters |
| Double Layer CZ Machine | Produces two purlins simultaneously |
| Customized CZ Machine | Customized to produce special purlin designs |
Working Process of CZ Purlin Forming
The working process involves uncoiling the metal coil, feeding it through progressive forming stations to shape the C or Z profile, and cutting the beams to length:
- यह अनकॉइलिंग यूनिट feeds the metal strip into the machine through गाइडिंग रोल
- अक्यूमुलेटर controls loop of material for stable feeding
- The metal strip passes through फॉर्मिंग स्टेशन with upper and lower फॉर्मिंग रोलर्स
- Forming rollers have customized ब्लेड to bend the strip into C or Z shape through stages
- हाइड्रॉलिक सिस्टम adjusts the space between rollers
- The profiled purlin beam passes through the cutting station
- Cutting blades slice the beam at preset length into individual purlins
- Formed purlins are stacked on the आउटपुट टेबल
-
 रोलिंग शटर स्लैट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 हाईवे गार्डरेल एंड टर्मिनल फॉर्मिंग मशीन अधिक पढ़ें
-
 हाईवे U/C पोस्ट रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 2 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 3 वेव्स हाईवे गार्डरेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 इलेक्ट्रिकल कैबिनेट फ्रेम रोल फॉर्मिंग मशीन अधिक पढ़ें
-
 Din रेल रोल फॉर्मिंग मशीन अधिक पढ़ें
-
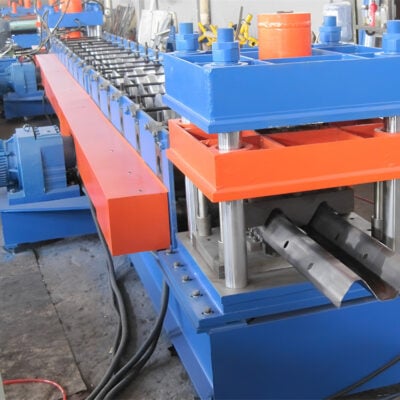 दो वेव हाईवे गार्डरेल मशीन अधिक पढ़ें
-
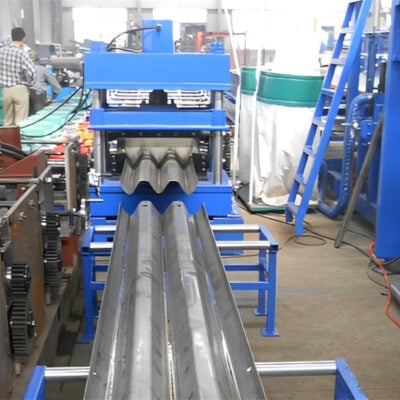 तीन वेव हाईवे गार्डरेल मशीन अधिक पढ़ें
Main Aspects of CZ Purlin Forming
सामग्री फीडिंग
- Coiled steel or aluminum strip of thickness 0.7-3 mm
- Max coil weight 5 tons
- Uncoiler with mandrel for smooth unroll of coil
- Accumulator controls feed loop for continuous production
प्रोफ़ाइल निर्माण
- Up to 8 progressive forming stations
- Stations have customized top and bottom blades
- Hydraulic cylinders adjust clearances between rollers
- Blades customized for specific purlin dimensions
- Quick tooling changeovers for profile changes
कटिंग और स्लाइसिंग
- Top and bottom cutting blades shear purlins at preset length
- Servo motor synchronizes blade action
- Length between 3-13 meters continuously
- Individual purlin lengths of 0.3-9 meters
अनुकूलन क्षमताएँ
- Flexible adjustment of all forming parameters
- Custom purlin sizes without blade replacement
- Special hole punching or embossing if needed
- Double layer machines produce two beams together
तकनीकी विनिर्देश
| मॉडल | उत्पादन गति (m/min) | Finished sizes (mm) | सामग्री की मोटाई (mm) | पावर (kW) |
|---|---|---|---|---|
| Manual 1000 | 8-10 | 100-300×50-120 | ≤3 | 11 |
| Auto 2000 | 15-18 | 100-300×50-150 | 0.7-2 | 37 |
| Double Layer 3000 | 8-12 | 150-250×80-100 | ≤2 | 45 |
के आपूर्तिकर्ता और मूल्य सीमा
CZ पर्लिन फॉर्मिंग मशीनें| आपूर्तिकर्ता | स्थान | मूल्य सीमा |
|---|---|---|
| Factory A | चीन | $10,000 – $100,000 |
| Factory B | भारत | $15,000 – $120,000 |
| ब्रांड C | यूरोप | $80,000 – $250,000 |
- Prices vary by production speed, purlin sizes, customization, and automation level
- Chinese machines offer cost advantage
- European brands provide high precision and durability
- Expect bulk order discounts up to 20%
- Additional cost for parameters like hole punching, embossing
स्थापना, संचालन और रखरखाव
| चरण | विवरण |
|---|---|
| स्थापना | – Civil and electric work needed – Trained technicians required for setup |
| संचालन | – 1-2 operators per shift – Parameter settings through control panel – Easy switchover between sizes |
| रखरखाव | – Daily oiling and cleaning – Inspect blade condition weekly – Replace blades annually or as needed – Check hydraulics and electrics biannually |
- Installation takes 1-2 weeks
- Comprehensive operator manual provided
- Online service support available
- Consumables include forming blades, oils, electrics
How to Select a CZ Purlin Forming Machine
Here are key considerations for selecting a CZ purlin forming machine:
अनुप्रयोग आवश्यकताएं
- Type and dimensions of purlins needed
- Production volume per shift/month
- Level of flexibility for future purlin changes
मशीन क्षमताएँ
- Size range of machine – min/max purlin depths
- Material thickness handling capacity
- Production speed to match volumes
- Automation vs manual adjustment
आपूर्तिकर्ता की विश्वसनीयता
- Experience in the industry
- Clientele and reviews
- पूछताछ के प्रति प्रतिक्रियाशीलता
- Warranties and service support
बजट सीमाएँ
- Available investment capital
- Desired ROI timeline
- Expected operating costs
Understanding application needs is essential before comparing machine specs and supplier proposals.
के फायदे और नुकसान
CZ पर्लिन फॉर्मिंग मशीनें| फायदे | नुकसान |
|---|---|
| – High production capacity – Flexible size changes – कम संचालन लागत | – High initial investment – Regular blade maintenance – Limited customization |
लाभ
- Single equipment produces entire range of purlin sizes
- Manual to fully automated options
- Reliable performance for small or large plants
- Low per piece production costs
सीमाएं
- Regular forming blade replacement
- प्रोफाइल परिवर्तनों के लिए सीमित लचीलापन
- Cannot match custom roll former output
अक्सर पूछे जाने वाले प्रश्न
Q: What thickness of coils can be handled?
A: Standard input material thickness is 0.7mm to 3mm. Some models support up to 4mm thickness.
Q: How often do the blades need replacement?
A: On average, forming blades require replacement after producing 15,000-25,000 tons depending on the material.
Q: What level of training is required to operate the machine?
A: Basic training takes 1-2 days. Manufacturers provide detailed operating manuals for reference.
Q: Can I get customized purlin designs?
A: Customization is limited to available profiles. For specialized designs, custom roll formers would be preferable.
Q: What safety measures are incorporated?
A: Standard safety features include emergency stop buttons, safety guards near moving parts, and covered electricals.
Q: What is the typical warranty period?
A: Warranty is generally 12 months from the installation date, covering manufacturing defects in materials and workmanship.
रोल फॉर्मिंग के बारे में अधिक जानें
अक्सर पूछे जाने वाले प्रश्न (FAQ)
1) What tolerances can modern CZ purlin forming machines reliably hold?
- Best-in-class lines achieve ±0.3–0.6 mm on web/flange dimensions and ±0.5 mm on hole-to-hole spacing with servo punching and closed-loop encoders. Cut-length accuracy of ±0.5–1.0 mm is typical with servo flying shear.
2) How fast can a quick-change CZ purlin line switch between C and Z profiles?
- With automatic tool cassette, motorized width/depth adjustment, and recipe recall, changeovers often take 8–20 minutes. Manual-adjust lines may require 30–60 minutes.
3) Can one machine handle high-strength steels (e.g., S350–S550)?
- Yes, but roll tooling, power, and passes must be specified accordingly. Expect more forming stations, higher motor torque, and anti-scratch coatings to manage springback and surface quality.
4) What punching options are common on CZ purlin lines?
- Inline hydraulic or servo-electric punching for web/flange holes, slots, service openings, and reference notches. Servo-electric units improve stroke precision and energy efficiency.
5) How do I reduce twist, bow, and camber defects in C and Z profiles?
- Ensure proper roll flower design, symmetric pass progression, calibrated entry guides, correct strip crown selection, and verify straightener settings. Use inline straightening and post-forming roll/press correction if needed.
CZ पर्लिन फॉर्मिंग मशीनों के लिए 2025 के उद्योग रुझान
- Servo-electric actuation: Replacing hydraulics on punching and gap control to reduce energy and improve repeatability.
- Smarter QA: Inline laser profilometry and vision AI detect flange flare, web bow, and hole position in real time, feeding SPC dashboards.
- High-strength transitions: More projects specify S450–S550 galvanized steel; roll designs optimized for controlled springback and hole accuracy.
- Rapid changeover: Auto C↔Z swap, motorized flange/web adjustments, and barcode-driven recipes minimize downtime in high-mix fabrication.
- Sustainability focus: Recycled-content galvanized coils and energy monitoring tied to ISO 50001 programs; suppliers disclose kWh/ton metrics.
- Compliance: Wider adoption of ISO 13849-1 PL d/e safety, IEC 60204-1, and EN 1090 execution standards for structural members.
2025 का प्रदर्शन स्नैपशॉट
| Metric (CZ Purlin Lines) | 2022 सामान्य | 2025 सर्वश्रेष्ठ-इन-क्लास | Benefit/Notes | स्रोत |
|---|---|---|---|---|
| Changeover time C↔Z | 35–60 मिनट | 8–20 मिनट | Higher OEE for mixed SKUs | OEM datasheets: Dallan, Bradbury, Samco |
| कट लंबाई सटीकता | ±1.0–1.5 mm | ±0.5–1.0 मिमी | Fewer erection-site adjustments | EN 1090 practices, OEM specs |
| छेद की स्थिति की सहनशीलता | ±1.0–1.5 mm | ±0.5–0.8 mm | Faster bolted connections | सर्वो पंचिंग विक्रेता |
| ऊर्जा तीव्रता (kWh/टन) | 150–190 | 110–140 | कम परिचालन लागत/उत्सर्जन | Siemens/ABB motion notes |
| Max line speed (plain profiles) | 18–25 m/min | 30–45 m/min | Throughput gains with servo shear | OEM brochures |
| Inline QA adoption (new lines) | ~25% | 50–60% | रियल-टाइम दोष निवारण | Keyence/Micro-Epsilon |
प्रामाणिक संदर्भ:
- ISO 13849-1 मशीनरी की सुरक्षा: https://www.iso.org
- IEC 60204-1 मशीनों के विद्युत उपकरण: https://webstore.iec.ch
- EN 1090 स्टील संरचनाओं का निष्पादन: https://standards.cen.eu
- World Steel Association (materials, HSS trends): https://worldsteel.org
- Keyence इनलाइन निरीक्षण: https://www.keyence.com
- Siemens motion efficiency resources: https://new.siemens.com
- ABB drives and energy optimization: https://new.abb.com/drives
नवीनतम अनुसंधान मामले
Case Study 1: Accelerating C↔Z Changeovers with Servo-Electric Punching (2025)
Background: A Middle East fabricator supplying high-mix purlins for logistics centers struggled with 45–55 min changeovers and hole-position rework.
Solution: Upgraded to servo-electric punching, auto C/Z cassette, motorized flange/web width control, barcode recipe loading, and inline laser measurement for flange flare and hole coordinates.
Results: Changeover time reduced to 14–18 min; hole-position CpK improved from 1.05 to 1.48; scrap fell 32%; energy/ton decreased 15%.
Case Study 2: Forming S500GD Z Purlins with Tight Tolerances (2024)
Background: An EU OEM needed Z purlins in S500GD with ±0.6 mm hole tolerance for automated bolting on site. Traditional roll design caused springback and twist.
Solution: Re-engineered roll flower with additional passes, crowned rolls, anti-flare calibration pass, and predictive springback compensation in CAD/CAM; added web pre-punch alignment sensors.
Results: Twist reduced by 41%; hole tolerance achieved ±0.6 mm at 32 m/min; first-pass yield improved from 95.1% to 98.4%.
विशेषज्ञों की राय
- Mark Thompson, Product Manager, Bradbury Group
“Demand is shifting to high-strength galvanized steels for longer spans. The winners will be lines that maintain hole accuracy and cut length at speed while minimizing springback.” - Dr. Ana Ribeiro, Structural Steel Specialist, European Committee for Standardization (CEN)
“Alignment with EN 1090 and robust traceability—heat numbers to hole maps—reduces site risks. Inline metrology linked to digital lot records is becoming a procurement requirement.” - Vivek Narula, CTO, Samco Machinery
“Servo-electric punching and automated gap control cut both energy and setup time. For CZ purlin forming machines, these upgrades typically pay back in 12–24 months at moderate volumes.”
व्यावहारिक उपकरण/संसाधन
- रोल डिज़ाइन और सिमुलेशन:
- COPRA RF (Datapoint/DAHEX): https://www.datam.de
- PROFIL Rollform Design Software: https://www.ubeco.com
- Altair Inspire/Forming: https://www.altair.com
- मानक और अनुपालन:
- EN 1090 स्टील संरचनाओं का निष्पादन: https://standards.cen.eu
- ISO 13849-1 सुरक्षा मानक: https://www.iso.org
- IEC 60204-1 विद्युत सुरक्षा: https://webstore.iec.ch
- इनलाइन QA और मापन:
- Keyence विज़न सिस्टम: https://www.keyence.com
- Micro-Epsilon laser profile sensors: https://www.micro-epsilon.com
- Operations and maintenance:
- Fiix CMMS: https://www.fiixsoftware.com
- UpKeep CMMS: https://www.onupkeep.com
Implementation tip: Before purchase, run a witnessed FAT using your coil grades (e.g., S350–S550) and full hole patterns. Verify changeover time, cut-length accuracy, hole position CpK, twist/bow, and energy/ton at target speeds, and retain SPC reports for Erection Method Statements.
अंतिम अपडेट: 2025-10-23
परिवर्तन-लेख: Added 5 FAQs, 2025 trends with performance table and citations; inserted two recent case studies; included expert viewpoints; compiled tools/resources with an implementation tip focused on CZ purlin forming machines.
अगली समीक्षा तिथि और ट्रिगर: 2026-05-15 or earlier if EN/ISO standards update, major OEMs release new CZ lines, or new HSS (S550+) forming data emerges.





